
CAPABILITY · PRESSES
Stamping & Forming Capacity
From 5-tonne high-speed progressive lines to 500-tonne hydraulic deep draws — matched to the part, not the other way round.
Two Families of Machines, One Shop
Mechanical presses win on speed; hydraulic presses win on controlled drawing speed and depth. We run both, so the process route follows the part. Progressive dies run on 5–250 tonne mechanical lines for high-volume stamped and lightly drawn parts, while 250–500 tonne hydraulic presses pull deep, thin-wall shells that mechanical motion would tear.
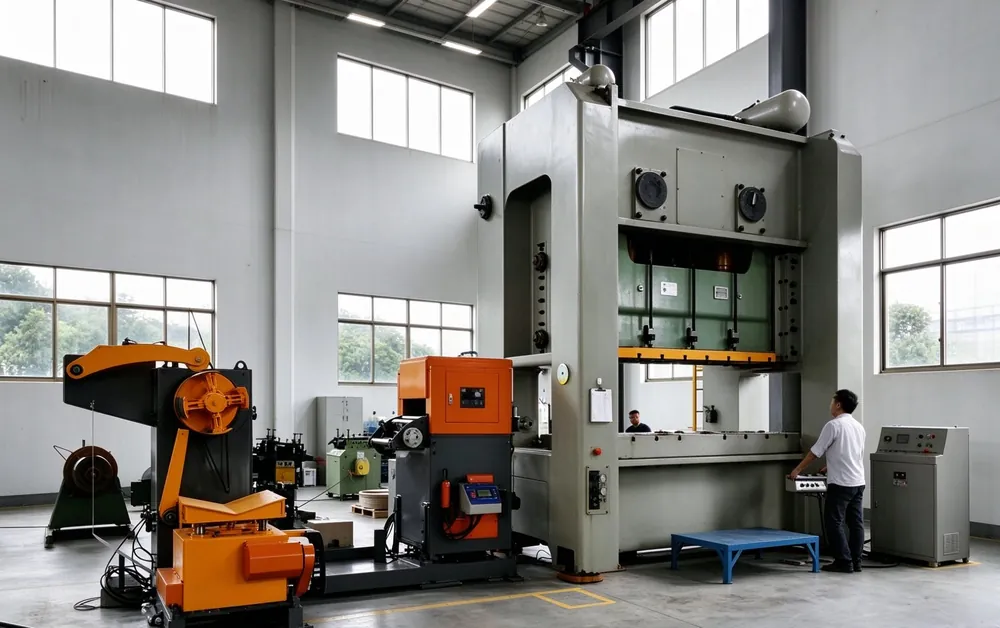
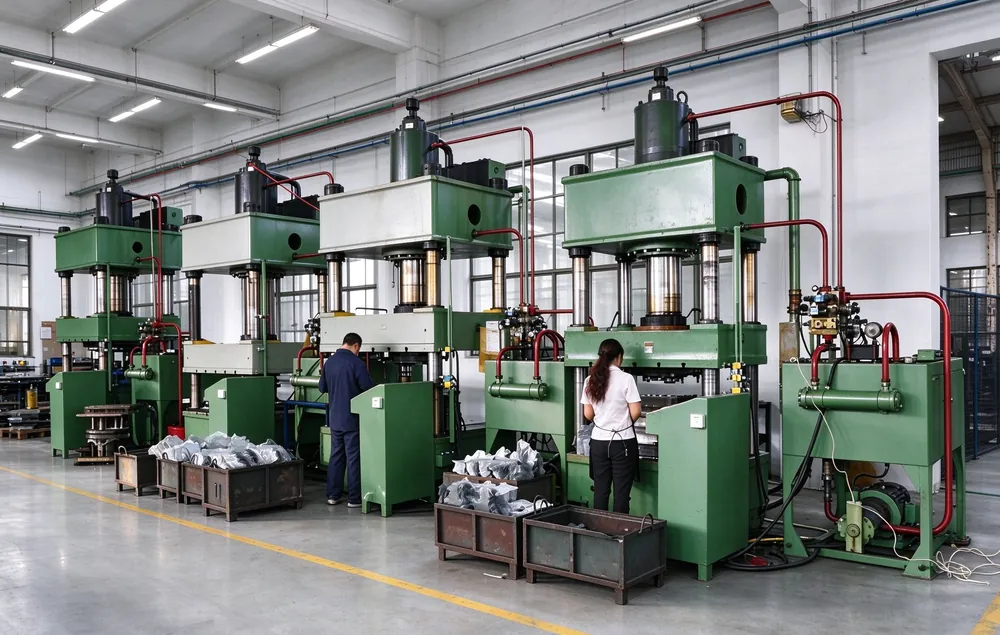
Multi-Stage Forming Under One Roof
Complex parts move through redraw, ironing, piercing, extruding and coining stages — each staged by our own tooling group so that tolerances accumulate correctly instead of drifting between vendors. Because the die shop, the presses and the inspection lab share one floor, a dimension that is drifting is caught at the press, not at the customer’s incoming check.
Typical cycle: coil in → progressive stamp or deep draw → CNC trim → wash → heat treatment or surface treatment where specified → final inspection → export packing.
Continue through the capability tour: the deep drawing process, tool & die design and quality control.
Talk To Our Engineers
Send your drawing to larry@aunov.com — material advice, tooling plan and a per-piece price within 24 hours.
Stamped and formed parts
- Oxygen sensor frame
- Stamped Round-Base Mounting Bracket
- Stamped End Cap with Side Hole
- Wiper Motor Cap with Shaft Boss
- Custom Multi-Hole Stamped Mounting Bracket with Locating Bosses
- Black Powder Coated Stamped Sheet Metal Panel Frame
- Custom Bent Sheet Metal Stamping Bracket
- Progressive Die Stamped Formed Bracket for Automotive
- Deep Drawn Circular Motor End Cap Stamping
- Custom Spun Metal Flanged Ring Bearing Seat
- Stamped Steel Shallow Drawn Motor Cover
- Automotive Chassis Stamped Mounting Bracket
- Automotive Seat Stamped Mounting Plate
- Deep Drawn Automotive Seat Stamping Component
- Stamped Automotive Seat Side Bracket with Large Bore
- Copper Coated Clutch Backing Plate Stamping
- Deep Drawn Square Cover with Flanged Rim Zinc Plated
- Galvanized Stamped Angle Bracket with Circular Cutout
- Stamped Sheet Metal Frame Corner Connector
- Zinc Plated Stamped L Angle Brackets
- Stamped U-Shaped Clamp Bracket Galvanized Steel
- Stamped Triangular Gusset Angle Bracket