
CAPABILITY · PROCESS
The Deep Drawing Process
How a flat blank of steel or aluminum becomes a seamless shell — the physics, the limits, and how we control them.
What Deep Drawing Actually Does
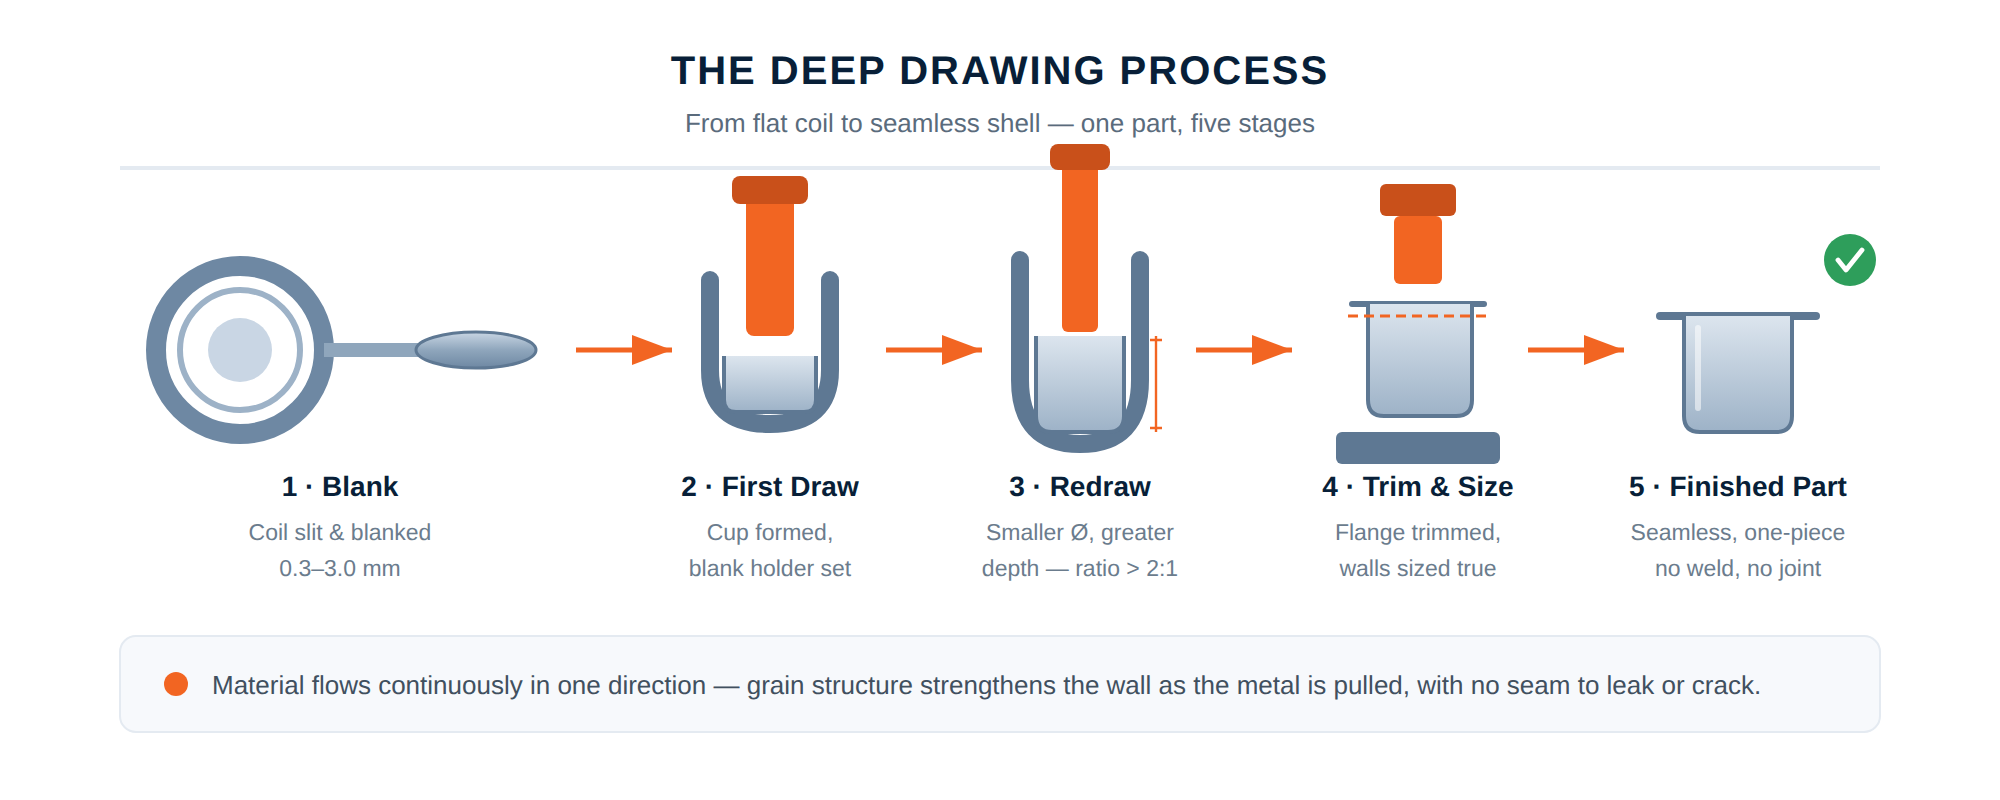
Deep drawing is a sheet-metal forming process that pulls a flat blank into a die cavity with a punch, transforming it into a closed, seamless hollow part — a shell, can, tube or housing — without welding or joining along the wall. The blank is clamped by a blank holder, the punch draws the material through a controlled gap, and the metal flows plastically into shape. Because the wall is formed from one piece of metal, the finished part has no weld seam to leak, corrode or fail.
The process is limited by how aggressively metal can be stretched in one pass. The draw ratio — blank diameter to punch diameter — governs whether a shell forms in one, two or three draws. Exceed it, and the wall tears at the punch radius. Our engineers calculate the blank size, draw ratio and intermediate annealing steps before tooling steel is ever cut, so the process is proven on paper first.
What Our Presses Can Draw
We deep draw stainless steels (SUS301, SUS304, SUS316, SUS430), low-carbon steels (SPCC, SPCE, 65Mn), aluminum (AL1060, AL3003, AL5052, AL6061) and brass (H62, H65) in thicknesses from 0.3 mm to 3.0 mm. Shell diameters range from a few millimetres — sensor-bushing scale — up to 300 mm across, with depth-to-diameter ratios beyond 2:1 using multi-stage draws.
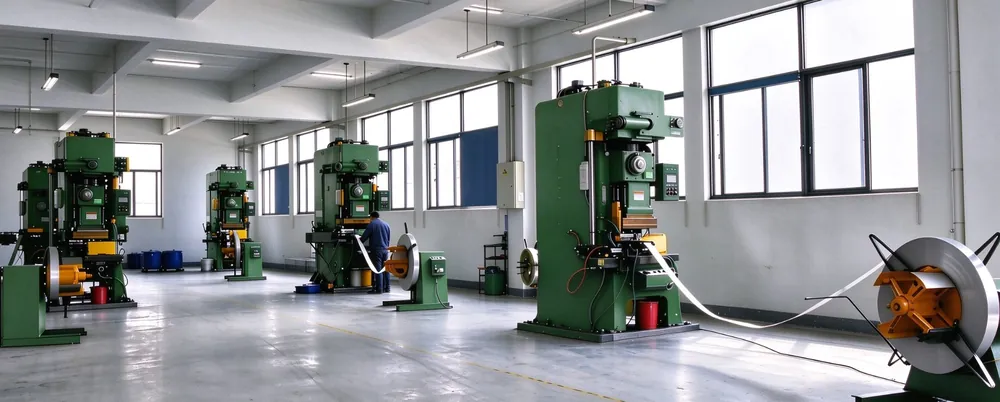
Mechanical presses of 5–250 tonnes run progressive and single-station dies at production speed, while 250–500 tonne hydraulic presses deliver the controlled drawing speed that deep, thin-wall shells demand. That combination means the process is never forced to fit the machine — the part dictates the route.
Where the Process Goes Next
Deep drawing rarely stands alone. Most of our parts continue through CNC trimming and turning, laser welding, surface treatment and final inspection before packing — all inside the same factory.
Continue through the capability tour: tool & die design, material selection and quality control pages.
Talk To Our Engineers
Send your drawing to larry@aunov.com — material advice, tooling plan and a per-piece price within 24 hours.