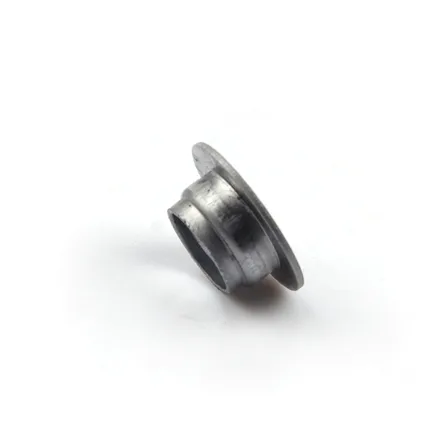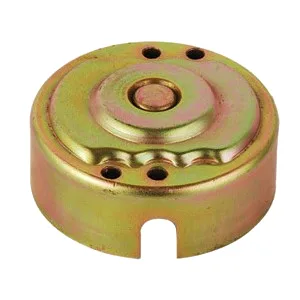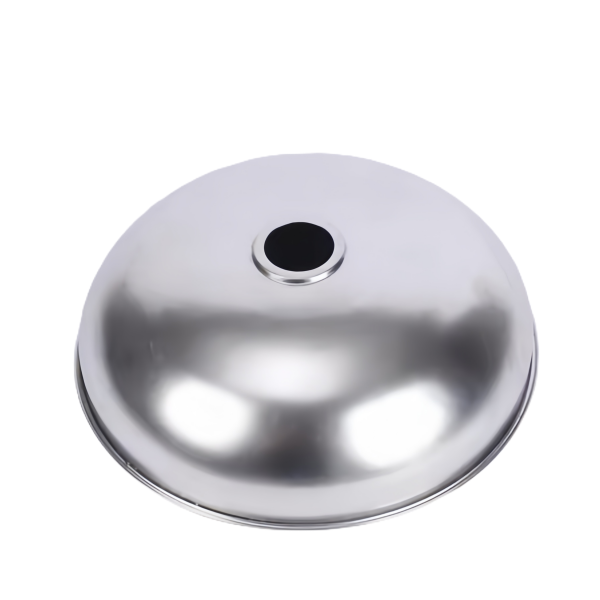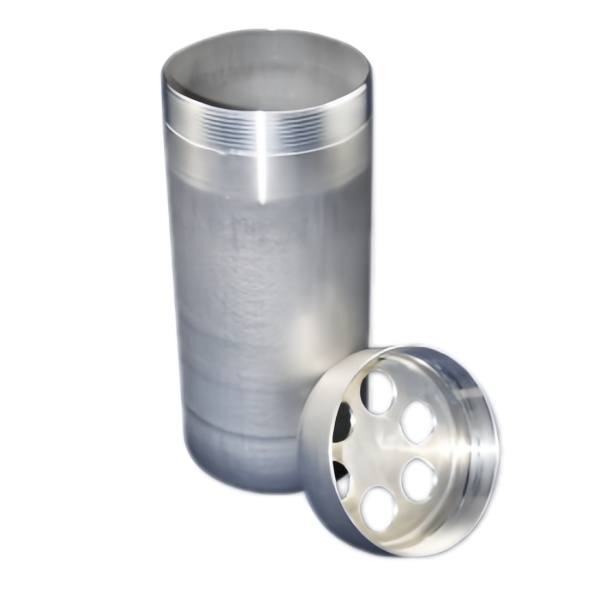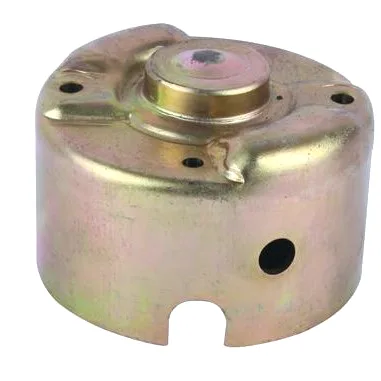
Aunov Tech manufactures the Deep drawn electric motor end cover in stainless steel on a single production floor. In operation, the drawn housing provides a closed, seam-free body the customer builds into. The same floor forms, machines and inspects the part, so first-article dimensions hold through volume batches without a second supplier involved.
Product overview
The specification of this metal cover turns on, the forming route, the tolerance band and the sealing faces, audited against the approved sample at each production release.
Toolroom, presses and machining centres used on this metal cover operate on the same site, so a change of wall or hole does not restart the programme, with process data archived for repeat orders.
Production route
The process for this metal cover runs in a fixed sequence: Drawing converts a flat blank into the finished envelope in one controlled sequence; flanges and rims are formed in the same line, then trimmed to length.
Each electric motor end shipment is verified against the master sample before it leaves the shop. That record is what every electric motor end reorder is built on, so nothing changes silently between shipments.
Materials and finishing
Everything is drawn from a fixed stock list: cold-rolled steel (SPCC / DC01), 304 / 316 stainless, aluminium, brass, copper and bronze with carbon steel or stainless specified on the drawing for this metal cover.
The finish is chosen for the duty it will see: zinc, nickel or chrome plating, anodising, powder coating, electrophoresis and passivation. The agreed finish for this metal cover travels with the part number on every reorder.
Route cards follow each electric motor end batch through the shop, so the next run starts from the data that already worked. Process settings for the electric motor end are archived, so later runs can be compared with the one you approved.
Quality control and inspection
Production runs under an ISO 9001 certified quality system: material traceability starts with mill certificates, the CMM measures the first article dimension by dimension, and run inspections follow an agreed sampling plan. Seal face finish and cavity depth are measured on the electric motor end first article. Where the application asks for it, torque, leak or pressure testing is added to the plan, and results travel with the batch paperwork.
Applications
The metal cover sits in industrial equipment and general assembly work in volume programmes as well as aftermarket supply.
Drawings for this metal cover are adapted across programmes, so the specification is set by the toughest of them, and the same first article applies throughout.
Specifications
| Item | Deep drawn electric motor end cover |
|---|---|
| Brand | AUNOV |
| Designing | Quotation follows the print, not a catalogue – a manufacturability review comes back with the quotation; changes are priced before they are made. |
| Tooling | Our toolroom covers die design, wire-cut EDM and maintenance, so no tooling step is outsourced, and first-article timing is measured from the tooling start date. |
| Samples | Sample and first article are the same discipline here: measured, reported, then approved. |
| Materials | Stock runs to carbon steel, 304 / 316 stainless, aluminium and brass; the final grade is fixed with the drawing review. |
| Surface finish | Surface treatment matched to the duty: plating, coating or polishing; finish thickness and adhesion checked on the first article. |
| Processing | Multi-stage deep drawing with interstage annealing, trimmed and pierced in following dies; every stage is logged against your part number. |
| Equipment | 5-250 T mechanical presses, 250-500 T hydraulic presses and annealing furnaces in line; first articles and batch samples are checked on the CMM. |
| Tolerance | +/-0.1 mm general on drawn sections, +/-0.03 mm on machined seats; dimensional reports accompany the first article. |
| Delivery terms | CIF or DDP, with FOB available, T/T with deposit and L/C for larger runs; price breaks tie to annual volume. |