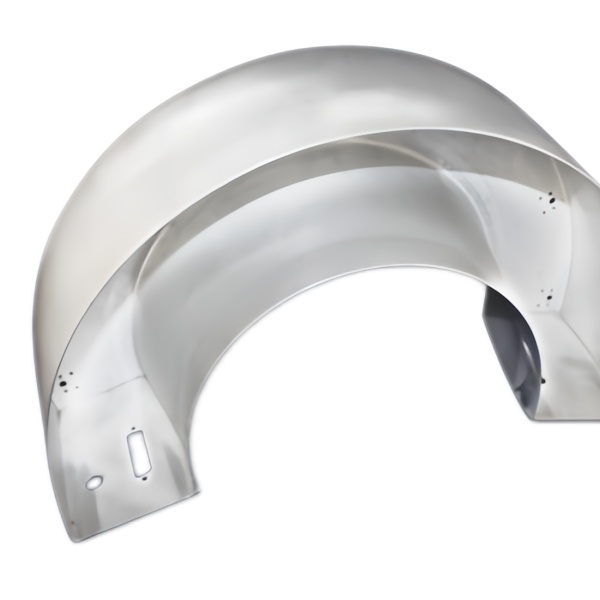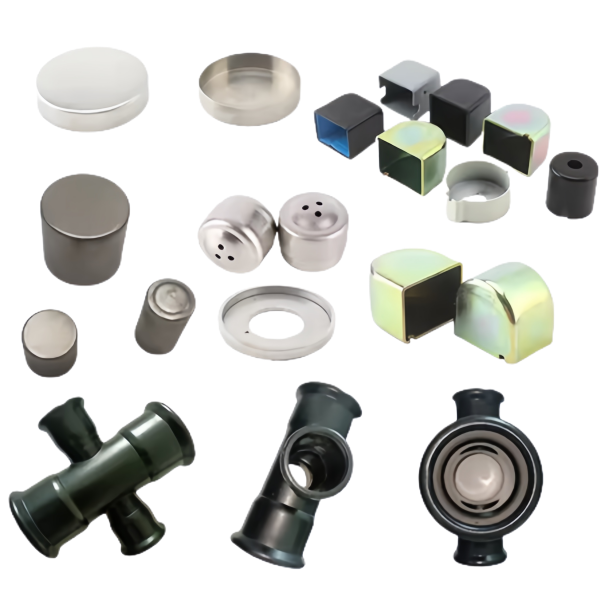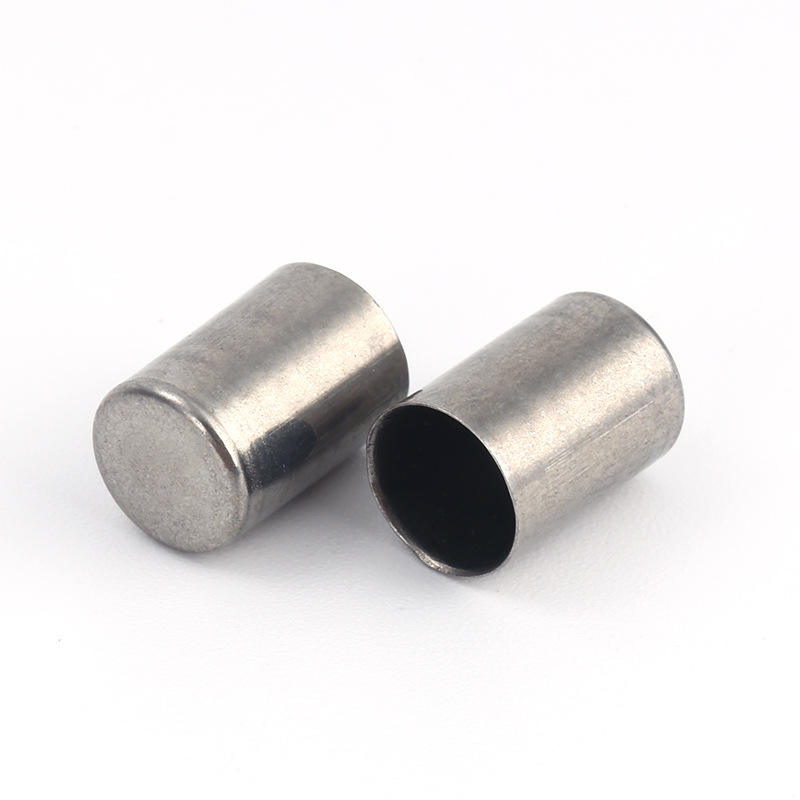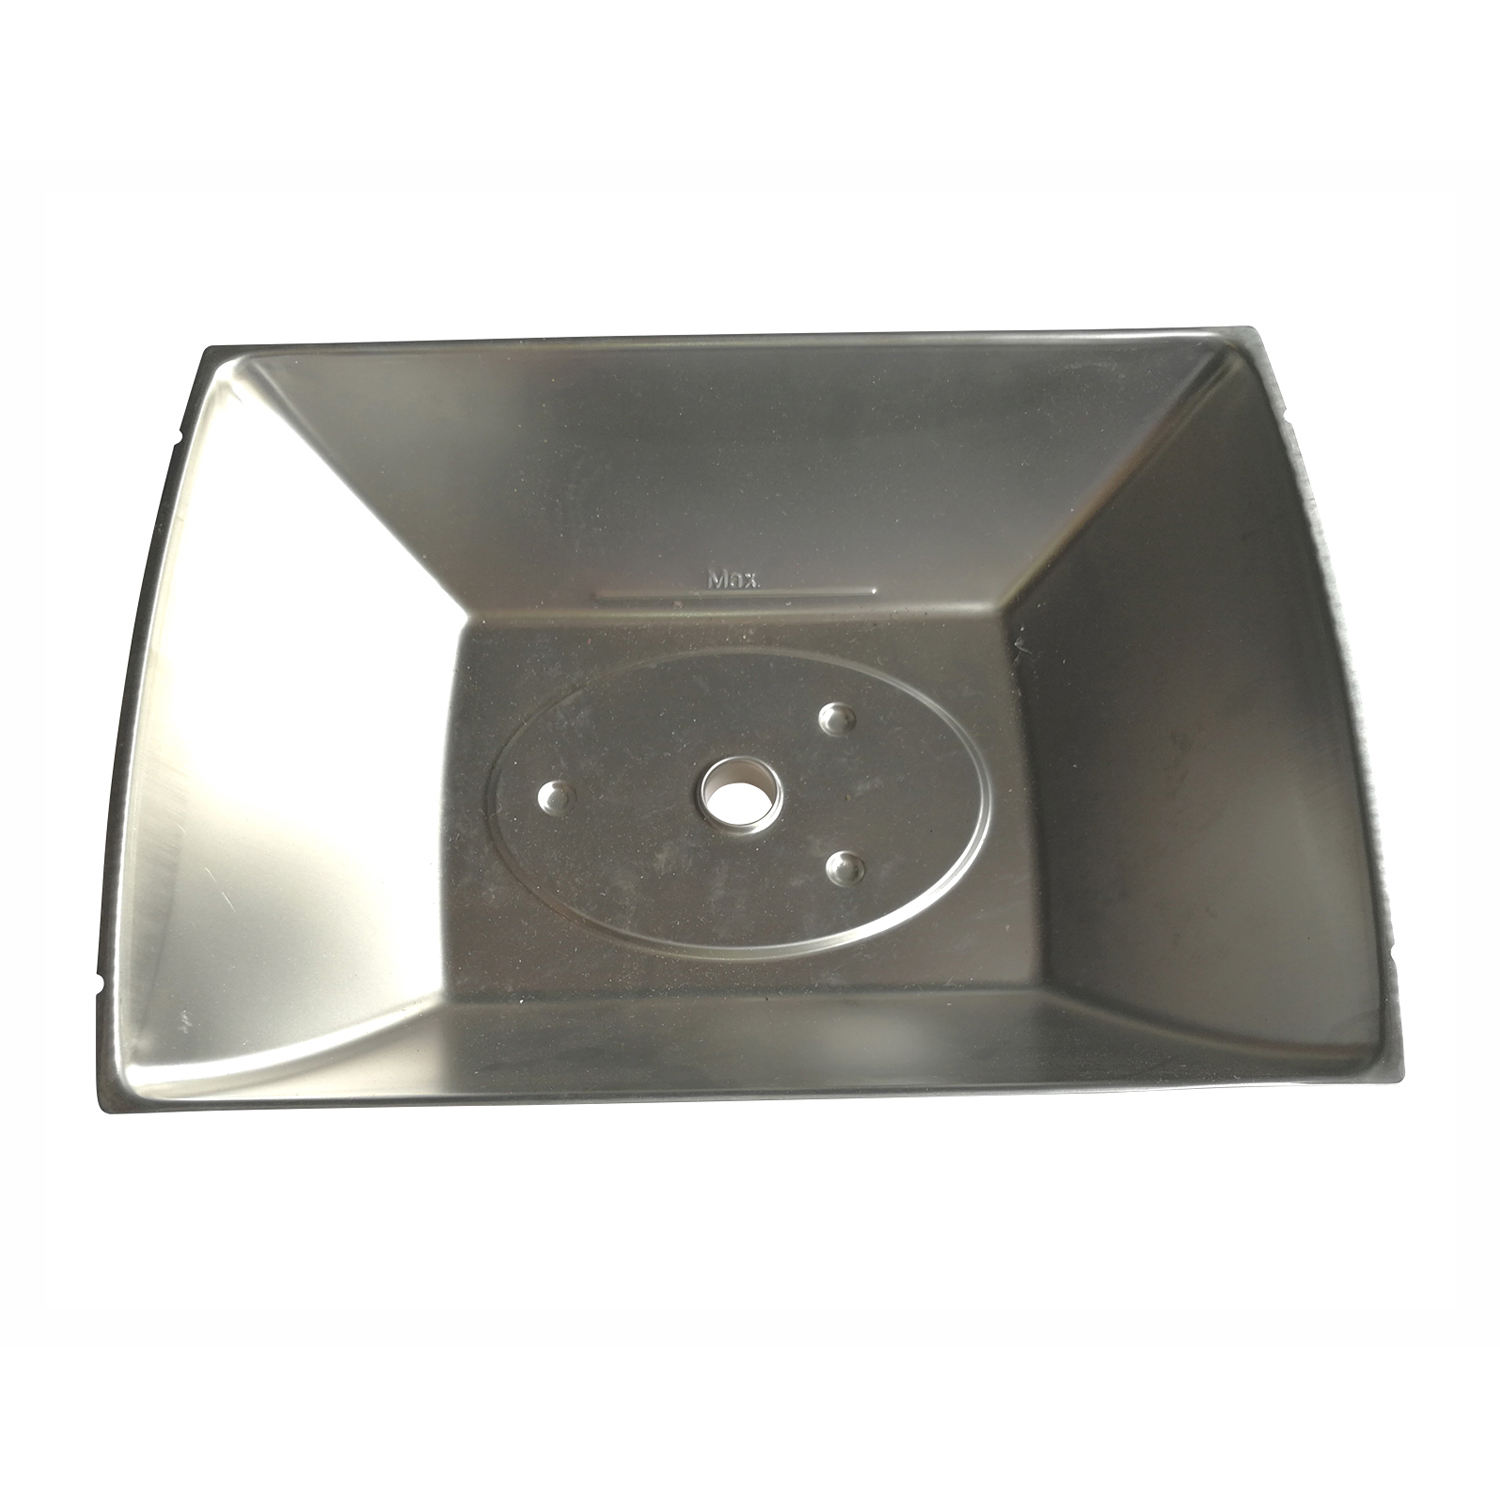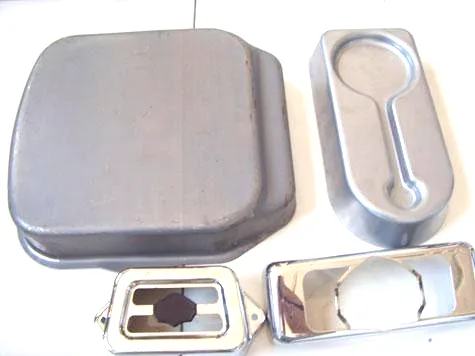
The Deep drawn box is produced by Aunov Tech from stainless steel, formed and finished under one roof. In the assembly, the deep drawn part combines forming and machining to reach the print on every controlled face. One production floor covers forming, finishing and inspection, keeping first-article quality through scheduled runs on one production route.
Product overview
What defines this metal component is, wall thinning, concentricity and the finished mating faces, audited against the approved sample at each production release.
Tooling and finishing for this metal component run under one roof, so a change of wall or hole does not restart the programme, with process data archived for repeat orders.
How the part is produced
The route for this metal component is fixed and repeatable: Drawing runs from flat blank to finished envelope in one controlled sequence; secondary machining holds the seats, threads and faces that forming cannot produce.
Production batches of the box are gauged back to the signed first article, not to a memory of it. Any change to the box drawing is re-approved and re-verified before production continues.
Materials and finishing
Our stock list runs to SPCC / DC01 carbon steel, 304 / 316 stainless, aluminium, brass, copper and bronze and the grade agreed for this metal component is carbon steel or stainless.
The finish is chosen for the duty it will see: polishing, plating in zinc, nickel or chrome, anodising, powder coating, electrophoresis and passivation. Once approved, the finish for this metal component is fixed and does not get re-decided.
Production batches are gauged to the signed first article, and material certificates are kept per batch.
Quality control
An ISO 9001 certified system governs production: material traceability starts with mill certificates, a full CMM report approves the first article, and production batches are inspected on a sampling plan. The box first article is CMM measured – threads gauged to class, diameters on the record. Functional testing – torque, leak or pressure – can be written into the plan, and results travel with the batch paperwork.
Applications
Typical installation of the metal component is in industrial equipment and general assembly work for OEM and Tier-1 customers.
One part number for this metal component frequently serves several assemblies, so the specification is set by the toughest of them, and the die does not have to change.
Specifications
| Item | Deep drawn box |
|---|---|
| Brand | AUNOV |
| Designing | Made to your 2D/3D drawings (PDF, DWG, STEP, IGS) – unusual walls, threads or tolerances are feasibility-checked first; changes are priced before they are made. |
| Tooling | The die is dedicated to your part and maintained on a recorded schedule. |
| Samples | Sample parts are measured and reported before submission, so any deviation is corrected at sample stage, and later batches are gauged back to the signed sample. |
| Materials | Carbon steel (SPCC / DC01), 304 / 316 stainless, aluminium and brass are held on site; mill certificates and heat numbers accompany the first article. |
| Surface finish | Plating, powder coating, anodising or polishing, per the print; alternatives quoted with the quotation, samples approved in writing. |
| Processing | Coil blanking and progressive drawing, coining on the final station where the print calls for it; first articles verify the whole flow before the run is released. |
| Equipment | Press shop running 5-250 T mechanical and 250-500 T hydraulic presses, annealing ovens on site, with CNC turning centres for secondary operations and CMM inspection. |
| Tolerance | +/-0.05 mm on formed features, with capability data on critical dimensions; capability is checked on the first article before the run continues. |
| Delivery terms | FOB, CIF or DDP per Incoterms 2020, payment by T/T or L/C, quoted in USD or EUR; price breaks tie to annual volume. |
Also known as: deep drawn cases — same part, same tooling, only the drawing reference differs.