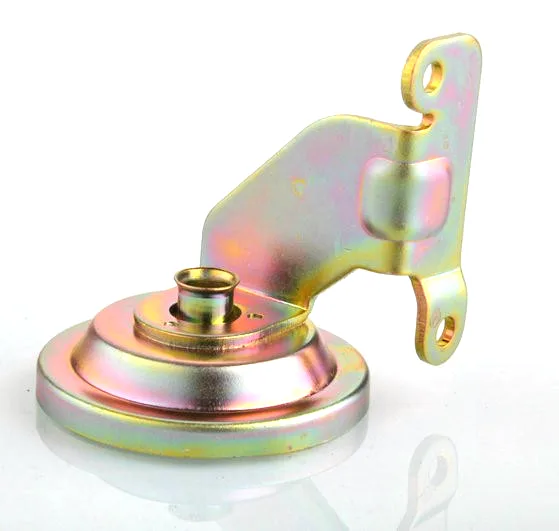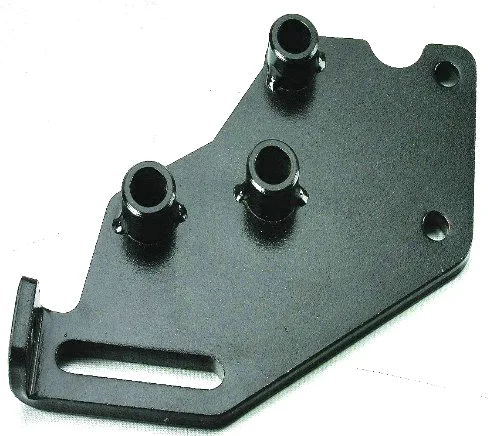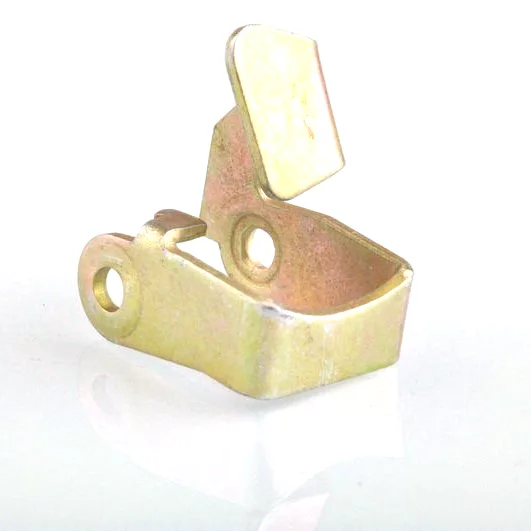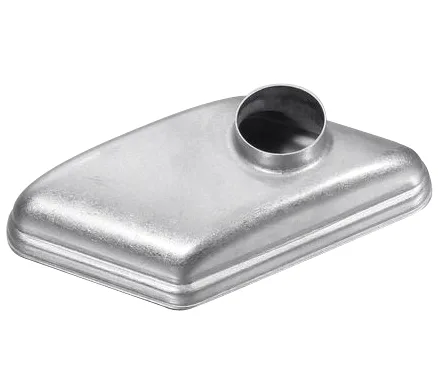
Aunov Tech manufactures the Sheet metal forming deep drawn deep drawing stainless steel parts deep in stainless steel on a single production floor. In service, the deep drawn part combines forming and machining to reach the print on every controlled face. Drawing, cutting and measurement sit on one floor, and a design change is re-sampled in one place on one production route.
Product overview
For this stainless steel component, the drawing centres on, the draw ratio, corner radii and the faces that must stay flat, each measured at first article and gauged on production batches.
Die work and machining for this stainless steel component sit on the same floor, so feasibility questions are answered on the shop floor, and nothing about the route depends on a third party.
How the part is produced
This is how the stainless steel component is built: Coil is blanked and drawn through progressive and single-stage dies; threads are single-pointed or rolled and seats bored in one setup where possible.
Production batches of the oval cover are gauged back to the signed first article, not to a memory of it. Process settings for the oval cover are archived, so later runs can be compared with the one you approved.
Materials and finishing
Base materials in stock: cold-rolled steel (SPCC / DC01), 304 / 316 stainless, aluminium, brass, copper and bronze and the grade agreed for this stainless steel component is 304 / 316 stainless steel.
Coating and polishing are matched to the end use: zinc and nickel plating, chrome, anodising, powder coating and passivation. Once approved, the finish for this stainless steel component is fixed and does not get re-decided.
Production batches of the oval cover are gauged back to the signed first article, not to a memory of it. Process settings for the oval cover are archived, so later runs can be compared with the one you approved.
Quality control
Production runs under an ISO 9001 certified quality system: stock arrivals are checked against mill certificates, the CMM measures the first article dimension by dimension, and production batches are inspected on a sampling plan. The oval cover first article goes on the CMM, with threads gauged to class. If the assembly calls for torque, leak or pressure proof, the test is built into the quality plan, and results travel with the batch paperwork.
Applications
This stainless steel component is used in industrial and appliance assemblies for customers who own the drawing and the tooling.
Drawings for this stainless steel component are adapted across programmes, so the finish is chosen to cover the harshest of them, and the same first article applies throughout.
Customization and options
Frequently varied options in this oval cover family
Points customers normally tailor on this stainless steel component: material and coating for the duty, wall bands, flange forms, threads and bosses, closed ends and finishes matched to the working environment, with orders run as prototypes, pilot lots or scheduled call-offs.
Options for this stainless steel component already covered by the die are shown on the quote, so new tooling is only quoted where it is genuinely required. The same split appears on every oval cover reorder.
Specifications
| Item | Sheet metal forming deep drawn deep drawing stainless steel parts deep |
|---|---|
| Brand | AUNOV |
| Designing | Driven by your drawing or a physical sample – samples are reverse-measured into a controlled drawing; changes are priced before they are made. |
| Tooling | Dies, fixtures and gauges are made in our own toolroom, so die cost stays transparent, and the die remains dedicated to your part. |
| Samples | Samples are issued for approval before the run, so the part is proven before it is made in volume, and production starts only after your written sign-off. |
| Materials | Carbon steel, 304 / 316 stainless, aluminium and brass are all held in stock; special grades are sourced to the drawing when volumes justify. |
| Surface finish | Natural, plated or coated – the print decides, and the agreed finish is logged; alternatives quoted with the quotation, samples approved in writing. |
| Processing | Coil-fed stamping, deburred and finished to the print; in-process checks sit between stages, not only at the end. |
| Equipment | Press shop with 5-250 T mechanical presses and dedicated dies, backed by CNC turning centres and a climate-controlled inspection room. |
| Tolerance | +/-0.03 mm on pierced holes, +/-0.1 mm on formed sections; GD&T per drawing, PPAP-style reports on request. |
| Delivery terms | FOB, CIF or DDP per Incoterms 2020, T/T with deposit and L/C for larger runs; repeat orders reuse the approved first article. |
Packing and shipment
Finish comes first when packing this stainless steel component: each coating gets its own packing – interleaves, bags or trays, then cartons are sealed and palletised, with marks and documents as you specify.