
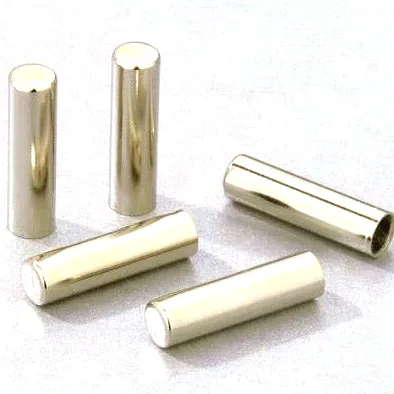
An NTC housing’s job changes completely depending on how the element is held in it, and that one decision – bonded, crimped, potted, or simply pressed – determines whether the housing is a two-part assembly or a single part, whether it can be serviced, and how it fails. It is worth starting there because most of what follows branches from it.
Deep drawing followed by CNC finishing on critical faces, at +/-0.02 mm on machined seats and sealing faces flat to drawing, with capability checked on the first article. So this is a drawn shell with machined features, and the shell is where the element goes.
Four ways to hold the element, and each is a different product
- Bonded. The element’s leads or its body are bonded to the housing’s interior – with an epoxy, a cyanoacrylate, or a thermally conductive adhesive. Advantages: cheap, no machining of a pocket. Requirements: the adhesive has to survive the temperature, it has to conduct, and it has to be applied to a clean and prepared surface. Failure mode: the adhesive softens or creeps, the element moves, and the reading shifts slowly.
- Crimped or riveted. A mechanical interference that squeezes the element’s leads against the housing. Advantages: it holds without adhesive and it survives temperature better than an adhesive does. Requirements: the crimp’s force has to be right, and the crimp’s damage to the element has to be acceptable. Failure mode: the crimp relaxes and the element becomes loose, which adds a thermal resistance in the measurement path.
- Potted. The housing is filled with a thermally conductive compound that encapsulates the element and its leads. Advantages: mechanically protected, thermally well coupled, and it eliminates air gaps. Requirements: the compound has to be poured to a controlled depth, it has to be thermally conductive, and it has to survive the temperature. Failure mode: the compound shrinks away from the wall over years, which opens an air gap, which degrades the accuracy slowly.
- Simply pressed or loose. The element sits in a pocket sized to it and is retained by the housing’s closure or by a press fit. This is the simplest and it is the one where the housing’s internal geometry has to hold the element in position exactly, because there is nothing else doing it.
So the first item on this part’s drawing should be: how is the element held, and is the housing supplied with the element in it or empty? Those are different parts – one is a sensor, the other is a housing – and the tolerance scheme, the inspection plan and the price are all different.
The pocket, which is the dimension that sets the accuracy
On a loose or a crimped element, the pocket’s geometry is the element’s positioning, and three of its dimensions are functional.
- Depth. How far the element sits from the process wall. Too close and the element is in the boundary layer where the temperature is not the bulk temperature. Too far and there is an air gap and the reading lags. The element’s datasheet usually states the required immersion and the housing should follow it exactly.
- Diameter. This is a fit to the element and it is also a thermal decision. A loose fit leaves an air gap, which is an insulator, which is a lag. A very close fit improves conduction but makes assembly harder and makes any tolerance variation into an interference. So the pocket’s diameter is a fit and a thermal specification at the same time.
- And the flatness of the pocket’s bottom, where the element sits. A pocket whose bottom is not square to the housing’s axis will hold the element tilted, and a tilted element is tilted relative to the process.
The wall, and the same trade as everywhere on this site
Stock covers carbon steel, 304 and 316 stainless steel, aluminium and brass. On an NTC housing the wall is a pressure boundary if the process is under pressure, a thermal path always, and a structural member if the part is handled or mounted.
- Thermal. The wall’s thickness sets the response, and the material sets the conductivity. Stainless Steel’s poor conductivity is why NTC housings are often thin, and on a fast-response NTC that is the main design lever.
- Structural, in a way that is easy to miss on a small sensor. A drawn thin-wall housing has very little resistance to being dropped, stepped on, or gripped hard. On a consumer or a field-installed NTC the wall’s minimum thickness at the corners is a durability requirement and the drawn corners are where it will fail first.
- And corrosion, where the process decides the grade – 316L for chloride-bearing and for cleaning regimes, and the L grade if the housing is welded.
If the element is bonded in the pocket, the pocket’s interior is the finish
Surface treatment matched to the duty, with alternatives quoted alongside the quotation and samples approved in writing. On this part the finish’s most important job is inside.
- The pocket’s interior, if the element is bonded or potted there. The adhesive or the compound adheres to the surface, and a plated or passivated surface will not bond reliably. So if the design uses adhesive, the pocket has to be masked from the plating or specified pre-finish – and on a drawn pocket, the masking is a process step rather than an operation on a machined feature.
- The sealing face, unmasked.
- The thread, masked or specified post-finish with an allowance.
- And a specific case on this part: where the element is bonded with a thermally conductive epoxy that needs the surface to have some roughness for adhesion, then the interior’s finish requirement is the opposite of a plating requirement – and stating “plated per the print” on a bonding surface is a contradiction that will only be found at assembly.
The pocket is the dimension most likely to be left as a general tolerance
+/-0.02 mm on machined seats and sealing faces flat to drawing. The tight band is on the machined features, and on this part the flagged dimensions are four, with the pocket being the one that is functionally most important and functionally most likely to be a general tolerance.
- Sealing face: flatness and perpendicularity, measured as two values.
- Pocket depth and diameter, as a fit to the specified element, with the pocket’s bottom’s flatness stated.
- Any locating feature’s concentricity to the pocket, where the element’s position is set by the housing’s geometry.
- And the drawn wall at a general band, with a minimum wall at the closed end and at the corners as a separate requirement – because on a drawn part the wall’s variation is the material’s own and it cannot be held tighter, but the minimum at the corners is a design parameter that has to be controlled.
An empty NTC housing is dimensional, a filled one is functional
First articles verifying the whole flow before the run is released. On an NTC housing supplied empty the inspection is dimensional; on one supplied with the element it is functional, and that difference is worth stating because it is the difference between a component and a sensor.
- Sealing face flatness and perpendicularity, on every part.
- Pocket geometry and concentricity, on every part, and a gauge check against the specified element where an element is involved.
- A functional test on a sampled basis where the housing is supplied with the element: a resistance check against the expected curve, which is the only test that verifies the element’s position and the housing’s thermal coupling together.
- And a leak test where the housing is a pressure boundary.
Empty housing or supplied with the element, and who calibrates it?
Is this housing supplied with the element in it, or empty – and if it is supplied with the element, is the calibration done in our facility or the customer’s? Three questions, and they change the product completely. An empty housing is a machined component with an inspection plan and a price that reflect that. A housing supplied with an element is a sensor, and it has requirements the empty one does not: a functional test, a calibration record, a stated tolerance on the assembly’s resistance at a reference temperature, and – where the element is bonded or potted – a cure time in the route that has to be respected before the part can be tested. And the calibration question decides who owns the accuracy: if we calibrate it, then the housing’s pocket depth and the element’s position are our responsibility and the assembly’s tolerance is ours to state; if the customer calibrates it, then the housing has to be dimensioned to their element and their process and the tolerance we quote is a component tolerance rather than a sensor tolerance. That last one is worth settling explicitly, because it determines what number goes on the drawing and what number the customer is going to measure. And there is a fourth question that is nearly always missed on an NTC housing: what happens to the reading when the adhesive or the potting fails? Not catastrophically – it drifts, slowly, over a year or two, and it will be diagnosed as a sensor fault rather than a housing fault. So whether that drift is acceptable should be decided before the housing is designed, because answering it usually points at a different way of holding the element.
Our Sensor Housings range is where this part sits. The sensor housings pages carry the process notes, common materials and inspection points behind every product in the family.
Specifications
| Item | NTC sensor housing (16) |
|---|---|
| Brand | AUNOV |
| Designing | Driven by your drawing or a physical sample – samples are reverse-measured into a controlled drawing; changes are priced before they are made. |
| Tooling | Die design and toolmaking stay in house, so a die can be re-cut against the approved drawing, and the charge is refundable against agreed volumes. |
| Samples | Approval is in writing, and the signed sample is kept as the reference for repeats. |
| Materials | Stock covers carbon steel (SPCC / DC01), 304 / 316 stainless steel, aluminium and brass; special grades are sourced to the drawing when volumes justify. |
| Surface finish | Surface treatment is matched to the duty: plating, coating or polishing; alternatives are quoted with the quotation and samples approved in writing. |
| Processing | Deep drawing comes first, then CNC finishing on the critical faces; first articles verify the whole flow before the run is released. |
| Equipment | Hydraulic presses for drawing, with CNC turning for finishing, with in-house toolmaking to keep dies and fixtures maintained. |
| Tolerance | +/-0.02 mm on machined seats, sealing faces flat to drawing; capability is checked on the first article before the run continues. |
| Delivery terms | FOB, with DDP offered for EU and US addresses, payment by T/T or L/C, quoted in USD or EUR; price breaks tie to annual volume. |
Related Products


Frequently Asked Questions
How does the way the element is held change the NTC housing?
Bonded, crimped, potted or simply pressed, that one decision determines whether the housing is a two-part assembly or a single part, whether it can be serviced, and how it fails. Those are different products, one a sensor and one a housing, with different tolerance schemes, inspection plans and prices. Deep drawing followed by CNC finishing on critical faces runs at +/-0.02 mm on machined seats and sealing faces flat to the drawing.
Why is the pocket the dimension most often left on a general tolerance?
On a loose or a crimped element the pocket’s geometry is the element’s positioning, and three of its dimensions are functional. The pocket is the one that is functionally most important and functionally most likely to be a general tolerance, which is the mismatch to catch. If the element is bonded in the pocket, the pocket’s interior becomes the finish that matters.
Is the housing inspected dimensionally or functionally?
Whether the housing is supplied empty or filled changes the inspection entirely: an empty shell is inspected as a component, a filled one as a sensor, and that is the difference between a component and a sensor. On an NTC housing the wall is a pressure boundary if the process is pressurised, a thermal path always, and a structural member if the part is handled. Stock covers carbon steel, 304 and 316 stainless steel, aluminium and brass.
What happens to the reading if the adhesive or the potting fails?
That fourth question is nearly always missed, and it is the failure mode of a bonded or potted build. The answer decides whether the design needs a mechanical retention as well as a chemical one. It is cheaper to resolve at enquiry than after the element is in the housing.
Request a Quote for This Part
Send a drawing or sketch — get material advice, tooling cost and a per-piece price within 24 hours (working days).