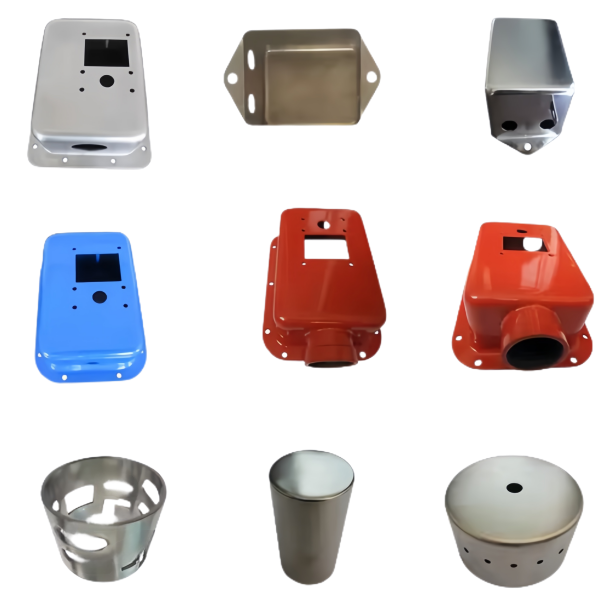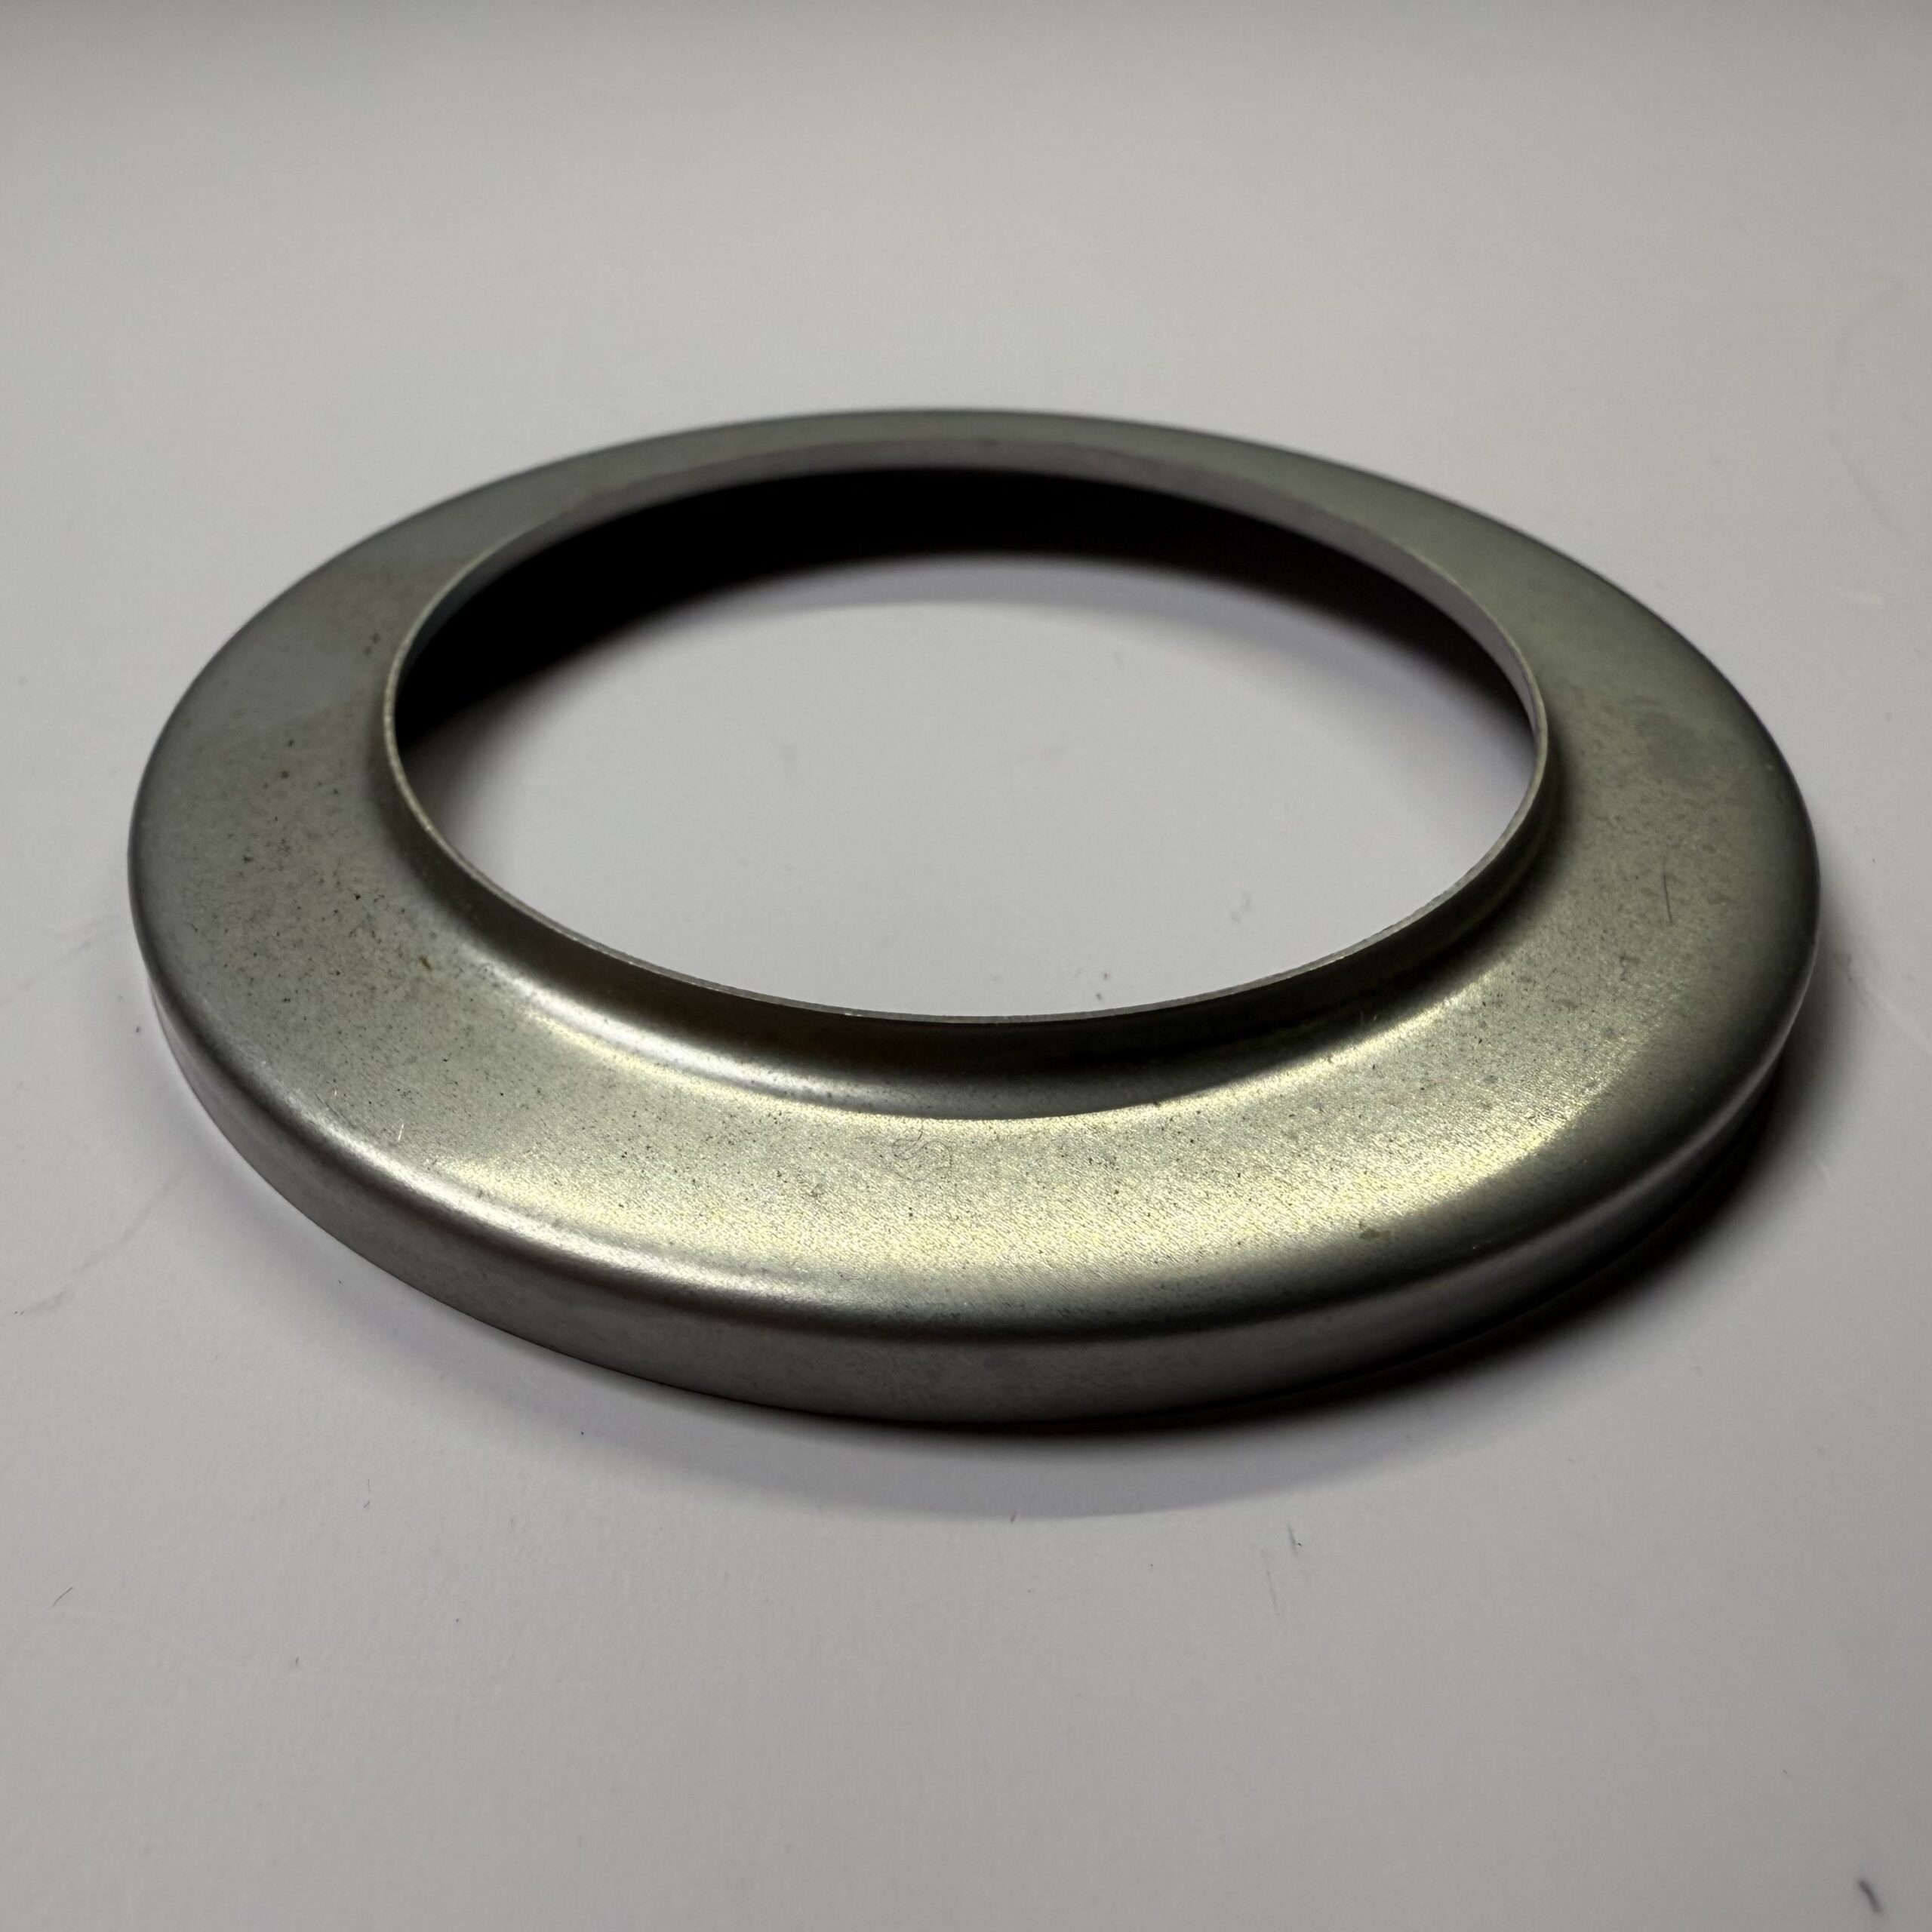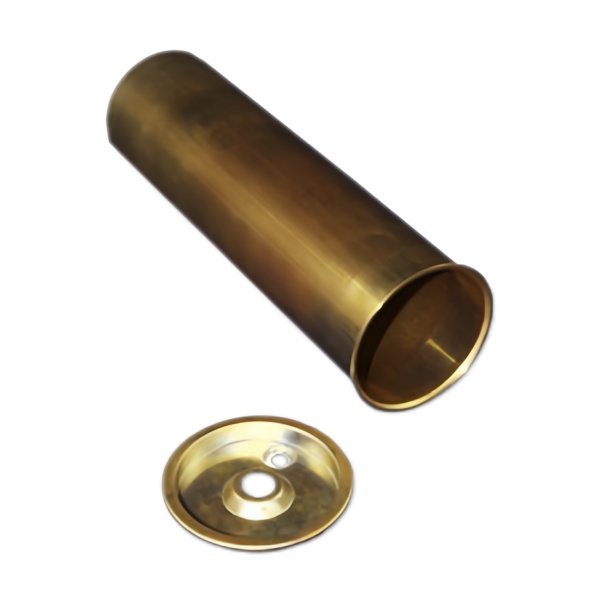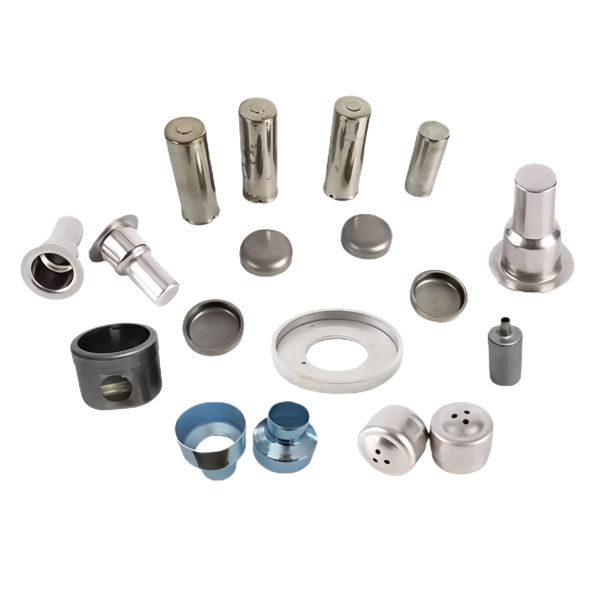
Produced in stainless steel by Aunov Tech, the Oil pump electric motor enclosure is formed and machined on the same floor. Once installed, the drawn housing encloses the sensitive internals and carries the mounting interface. Drawing, cutting and measurement sit on one floor, so repeat orders stay aligned with the approved sample with no third party in the loop.
Product overview
This metal enclosure is defined by, wall thinning, concentricity and the finished mating faces, all held to the drawing and verified at first article.
Die building, pressing and machining for this metal enclosure are all in house, so a change of wall or hole does not restart the programme, with the tooling history retained in house.
How it is manufactured
The route for this metal enclosure is fixed and repeatable: Drawing runs from flat blank to finished envelope in one controlled sequence; wall thickness is checked at the thinnest section after forming.
Repeat oil pump electric orders are measured against the approved sample, so neither material nor finish drifts between lots. Mill certificates are filed per heat, so oil pump electric traceability survives a change of material batch.
Materials and surface finish
Materials kept on the floor cover cold-rolled steel (SPCC / DC01), 304 / 316 stainless, aluminium, brass, copper and bronze and this metal enclosure is costed in carbon steel or stainless.
Coating selection follows the duty – indoor, outdoor or under-hood: electrophoresis, powder coating, anodising and zinc / nickel plating. The choice is recorded on the drawing for this metal enclosure, so the decision never has to be made twice.
Repeat oil pump electric orders are measured against the approved sample, so neither material nor finish drifts between lots. The signed oil pump electric sample remains the reference and is kept with the job file.
Quality control
Production runs under an ISO 9001 certified quality system: stock arrivals are checked against mill certificates, first articles are measured on a CMM, and production batches are inspected on a sampling plan. Cavity depth and seal face finish of the oil pump electric are measured at first article. Tests for torque, leakage or pressure can be arranged when the service demands them, and results travel with the batch paperwork.
Applications
You will find this metal enclosure inside pump, valve and fluid handling assemblies across automotive, appliance and industrial programmes.
The same metal enclosure is used across several platforms, so the tightest tolerance in the family sets the spec, and no re-tooling is needed.
Specifications
| Item | Oil pump electric motor enclosure |
|---|---|
| Brand | AUNOV |
| Designing | Your drawing sets the part – unusual walls, threads or tolerances are feasibility-checked first; changes are priced before they are made. |
| Tooling | Dies, fixtures and gauges are made in our own toolroom, so tooling lead time stays under our control, and the charge is refundable against agreed volumes. |
| Samples | Samples are issued for approval before the run, so the sample is retained as the master, and production starts only after your written sign-off. |
| Materials | Carbon steel (SPCC / DC01), 304 / 316 stainless, aluminium, brass and copper – the grade is matched to the duty of this enclosure. |
| Surface finish | Plating, powder coating, anodising or polishing, per the print; the agreed finish travels with the part number. |
| Processing | Multi-stage deep drawing with interstage annealing, trimmed and pierced in following dies; in-process checks sit between stages, not only at the end. |
| Equipment | Mechanical presses from 5 to 250 T and hydraulic presses 250-500 T, with in-line annealing furnaces; secondary ops run on CNC turning centres, inspection on the CMM. |
| Tolerance | +/-0.05 mm on drawn diameters, tighter bands confirmed against the drawing; capability is checked on the first article before the run continues. |
| Delivery terms | FOB Ningbo or Shanghai, payment by T/T, L/C at sight or D/P; call-off schedules are supported. |