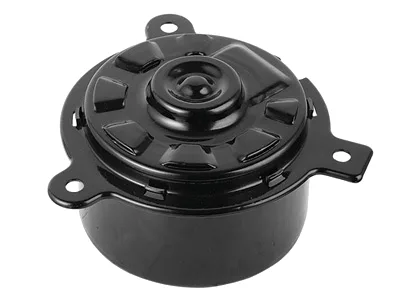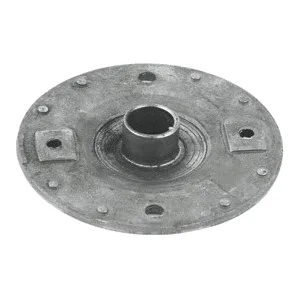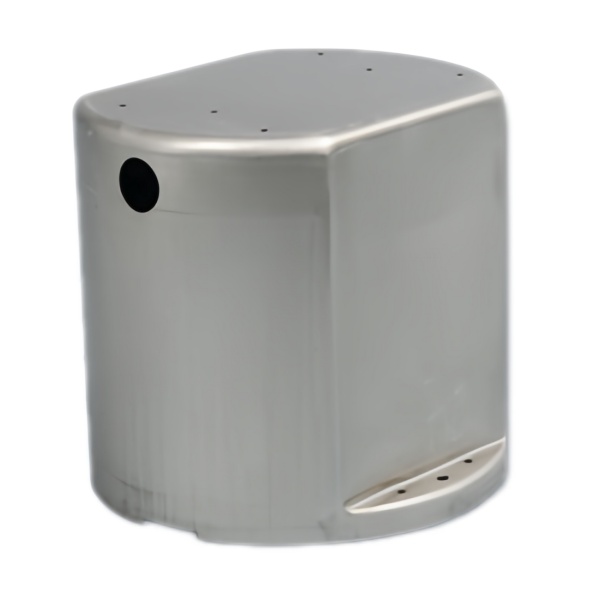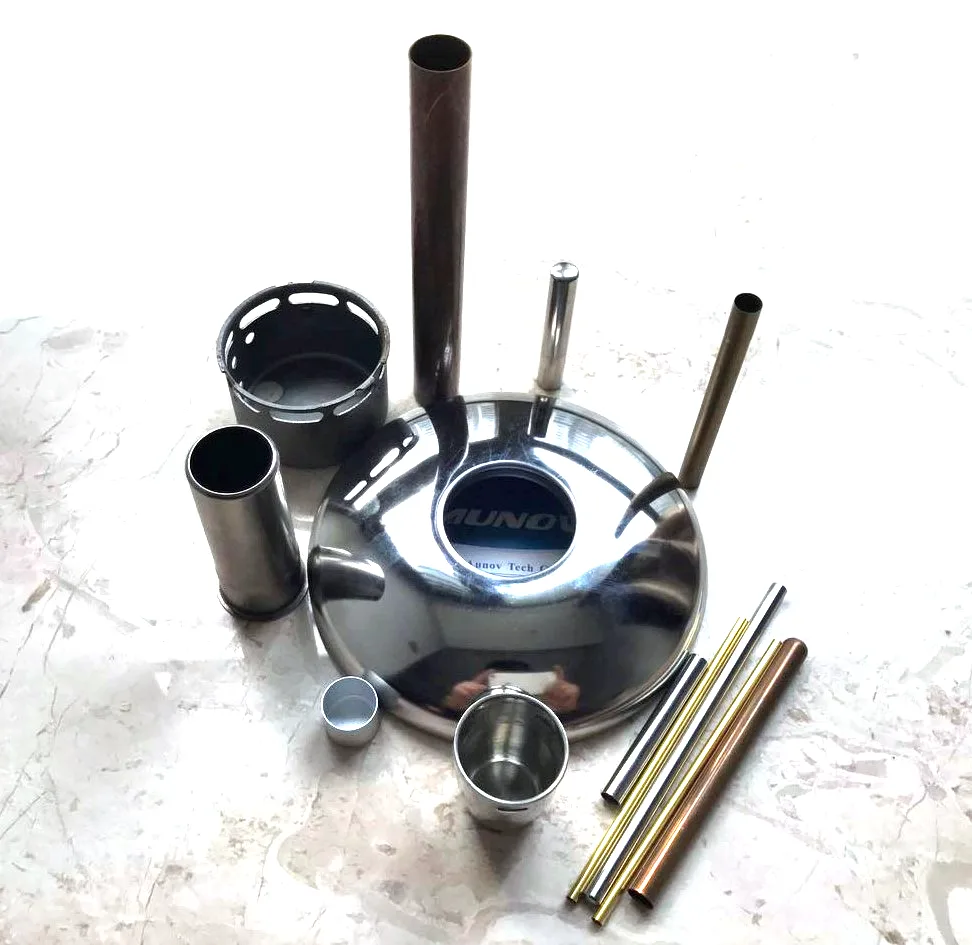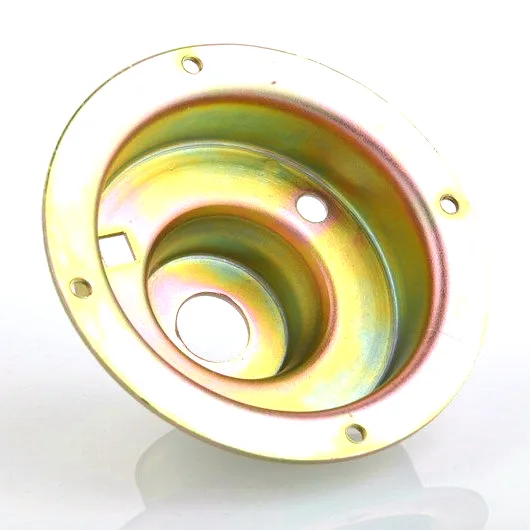
Produced in stainless steel by Aunov Tech, the Deep drawn cup is formed and machined on the same floor. In operation, the drawn housing shields the assembly from dust, moisture and handling while locating it in place. Forming, machining and inspection share one floor, so first-article dimensions hold through volume batches with no third party in the loop.
Product overview
What matters most on this metal component is, wall thinning, concentricity and the finished mating faces, recorded on the inspection report for every batch.
Forming, machining and finishing for this metal component happen on one site, which keeps the sample loop inside our own schedule, and the die record stays with your part number.
Production route
Manufacturing runs on a controlled process path: The drawn envelope is produced in stages with anneals between them; threads are single-pointed or rolled and seats bored in one setup where possible.
The cup manufacturing record is archived together with the drawing revision that produced it. Deviations on the cup are reported before shipment rather than found on your assembly line.
Materials and surface finish
Working stock covers cold-rolled steel (SPCC / DC01), 304 / 316 stainless, aluminium, brass, copper and bronze and this metal component is costed in carbon steel or stainless.
The surface treatment is picked to match the service conditions: electrophoresis, powder coating, anodising and zinc / nickel plating. The choice is recorded on the drawing for this metal component, so the decision never has to be made twice.
Batch records for the cup are filed against the part number, so process settings are reused instead of re-invented. The approved cup sample governs later runs, and any grade change is agreed in writing first.
Quality control
The plant is ISO 9001 certified: incoming material is verified against mill certificates, a full CMM report approves the first article, and every production run is inspected against the first-article report. The cup first article records cavity depth and seal face finish. Tests for torque, leakage or pressure can be arranged when the service demands them, and the inspection report ships with each batch.
Applications
The metal component sits in industrial and appliance assemblies in both OEM and aftermarket supply.
This metal component is supplied to several positions in the same machine, so the finish is chosen to cover the harshest of them, and cost per piece stays at the volume tier.
Specifications
| Item | Deep drawn cup |
|---|---|
| Brand | AUNOV |
| Designing | Made to your 2D/3D drawings (PDF, DWG, STEP, IGS) – DFM notes are returned before any tooling is cut; revisions are re-quoted once rather than silently absorbed. |
| Tooling | Tooling is built and held under your part number, so tooling lead time stays under our control, and first-article timing is measured from the tooling start date. |
| Samples | Production does not start until the sample report has been signed off. |
| Materials | Materials held include carbon steel, 304 / 316 stainless, aluminium and brass; mill certificates and heat numbers accompany the first article. |
| Surface finish | Zinc, nickel or chrome plating, anodising, passivation or e-coat; alternatives quoted with the quotation, samples approved in writing. |
| Processing | Progressive drawing through several stages, annealed between draws, then trim and pierce; first articles verify the whole flow before the run is released. |
| Equipment | Mechanical presses from 5 to 250 T and hydraulic presses 250-500 T, with in-line annealing furnaces; secondary ops run on CNC turning centres, inspection on the CMM. |
| Tolerance | +/-0.05 mm to +/-0.1 mm across the part, wall thickness held to print; finer bands confirmed from capability data before quoting. |
| Delivery terms | FOB Ningbo or Shanghai, T/T with deposit and L/C for larger runs; price breaks tie to annual volume. |