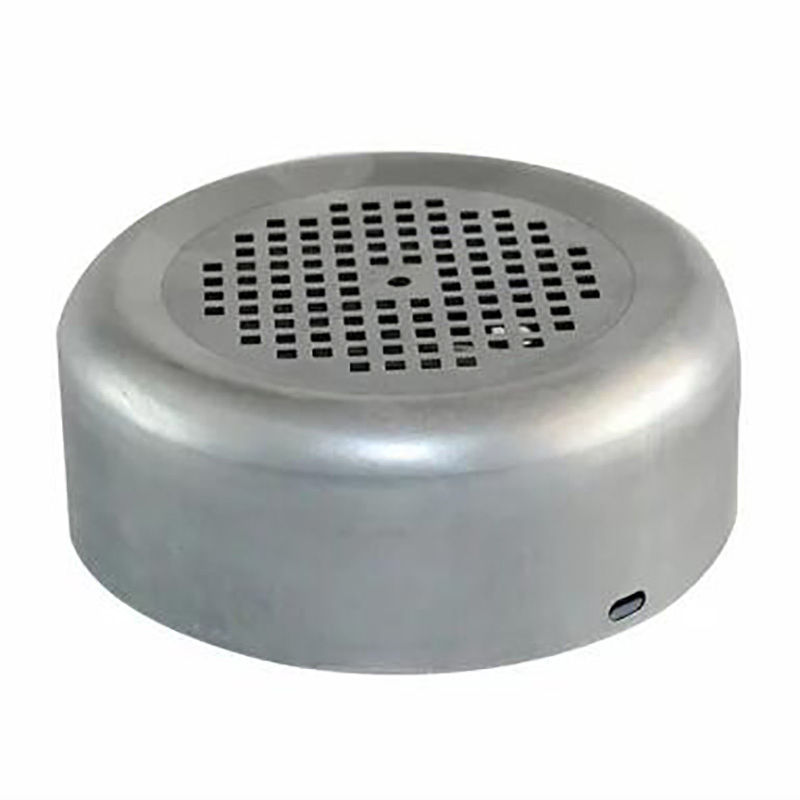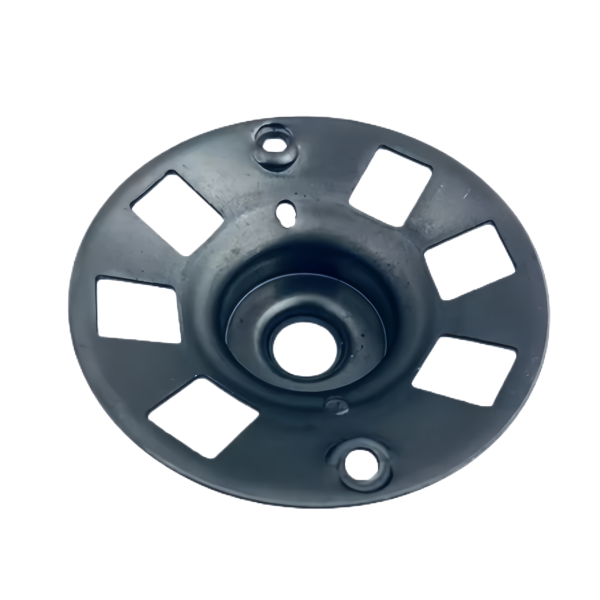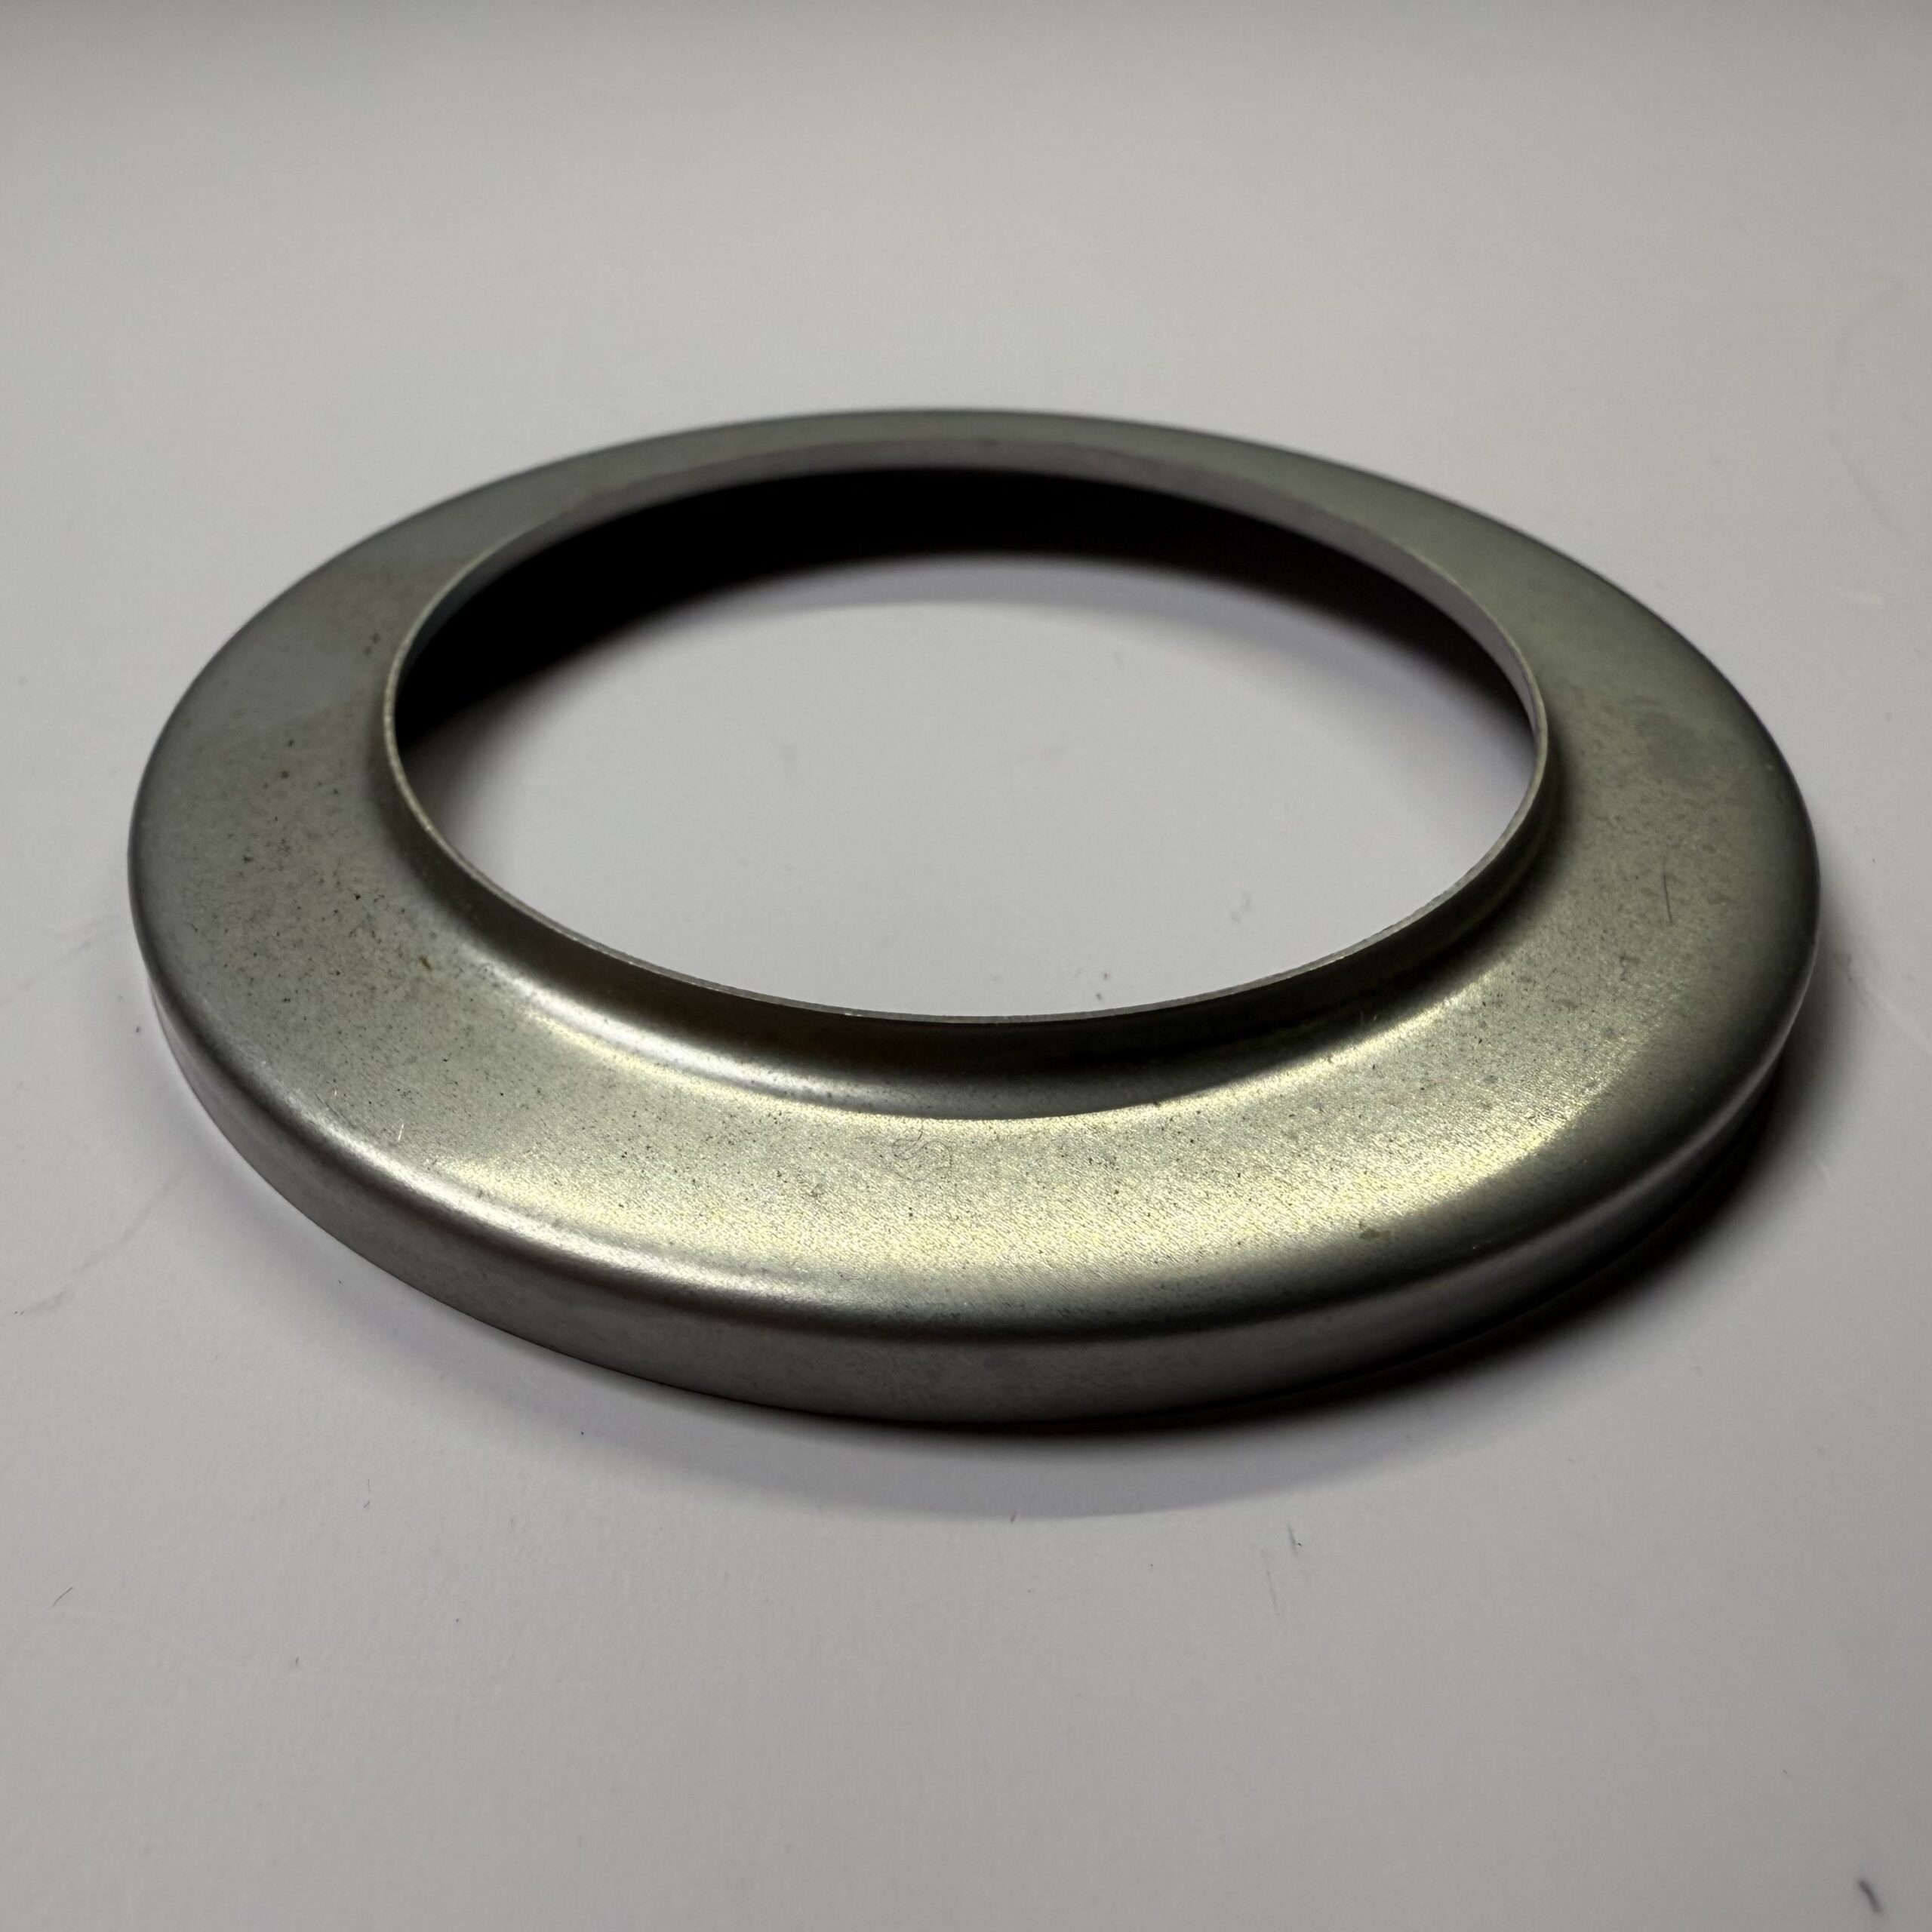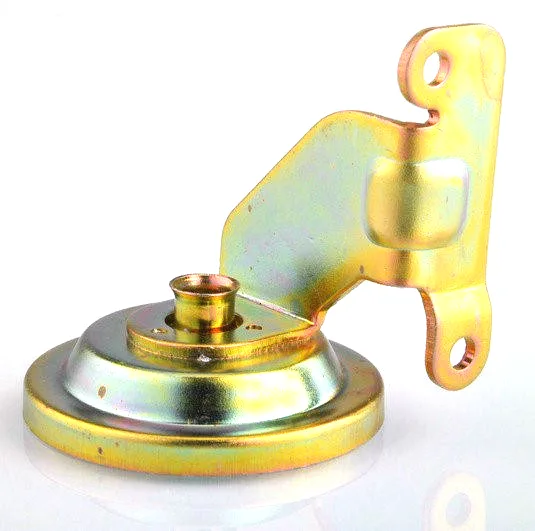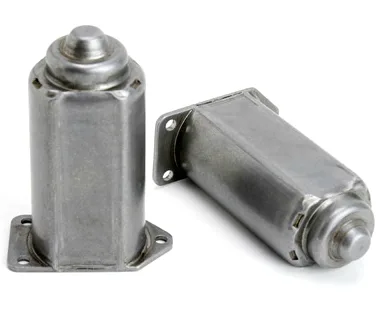
This Deep Drawn Connector is an Aunov Tech production part in brass or stainless steel, quoted and built to customer print. In operation, the CNC machined part provides the finished surfaces, threads and seats the mating parts locate on. One production floor covers forming, finishing and inspection, so first-article dimensions hold through volume batches under one roof.
Product overview
This metal component is defined by, wall thinning, concentricity and the finished mating faces, controlled from the approved first article onward.
The whole route from die to finished metal component stays in house, which keeps revision loops short and samples fast, and nothing about the route depends on a third party.
How the part is produced
Production of this metal component is locked to one route: Drawing converts a flat blank into the finished envelope in one controlled sequence; flanges and rims are formed in the same line, then trimmed to length.
The tooling record is stored against the part number, and the same setup is reused on the next call-off.
Materials and finishing
Everything is drawn from a fixed stock list: SPCC / DC01 carbon steel, 304 / 316 stainless, aluminium, brass, copper and bronze with carbon steel or stainless specified on the drawing for this metal component.
Because the part works in contact with media, the coating is chosen for cleanliness: zinc, nickel or chrome plating, anodising, powder coating, electrophoresis and passivation. It is written into the drawing for this metal component, so it cannot drift between batches.
The connector tooling and setup record is stored against the part number, so nothing depends on someone remembering. The signed connector sample remains the reference and is kept with the job file.
Quality control
The factory operates with ISO 9001 certification: certificates verify each incoming batch of material, the CMM measures the first article dimension by dimension, and routine sampling keeps batches aligned with the first article. The connector first article is measured on the CMM and thread gauges confirm class. If the assembly calls for torque, leak or pressure proof, the test is built into the quality plan, and results travel with the batch paperwork.
Applications
The metal component is specified into electronic and power conversion equipment for OEM and Tier-1 customers.
One drawing for this metal component is commonly applied to several programmes, so the finish is chosen to cover the harshest of them, and the same first article applies throughout.
Specifications
| Item | Deep Drawn Connector |
|---|---|
| Brand | AUNOV |
| Designing | Drawings are reviewed for feasibility, and the agreed version is what production runs against. |
| Tooling | Tooling is built and held under your part number, so tooling lead time stays under our control, and the die remains dedicated to your part. |
| Samples | Pre-production samples come with a full inspection report, so the part is proven before it is made in volume, and later batches are gauged back to the signed sample. |
| Materials | Standard stock: carbon steel (SPCC / DC01), 304 / 316 stainless, aluminium, brass; mill certificates and heat numbers accompany the first article. |
| Surface finish | Finish selected from the drawing: plating, coating, anodising or passivation; the finish is inspected with the dimensional report on the first article. |
| Processing | Deep drawing from coil or blank, with in-process annealing so walls thin evenly; first articles verify the whole flow before the run is released. |
| Equipment | Press shop running 5-250 T mechanical and 250-500 T hydraulic presses, annealing ovens on site, with CNC turning centres for secondary operations and CMM inspection. |
| Tolerance | +/-0.05 mm on formed features, with capability data on critical dimensions; finer bands confirmed from capability data before quoting. |
| Delivery terms | CIF or DDP, with FOB available, payment by T/T or L/C, quoted in USD or EUR; repeat orders reuse the approved first article. |