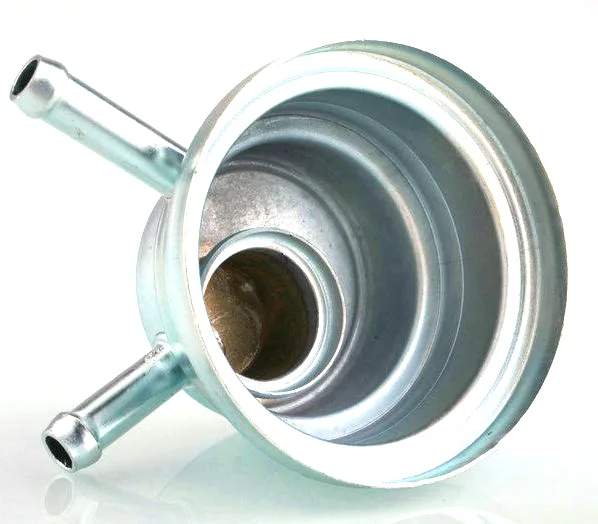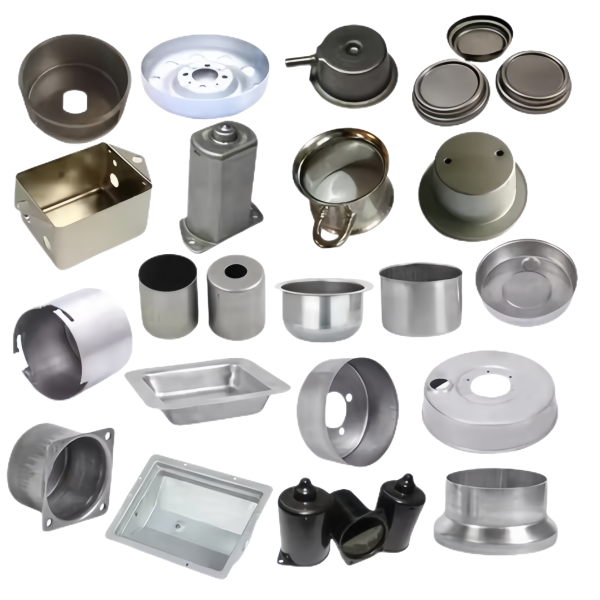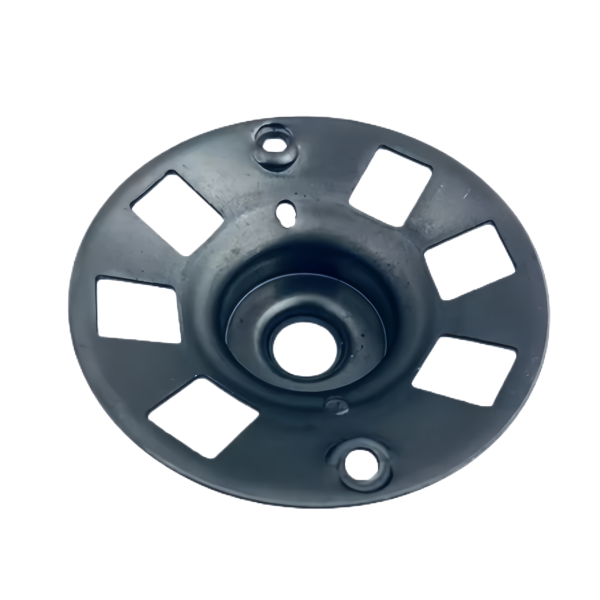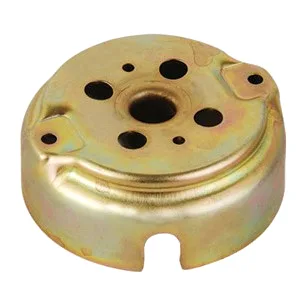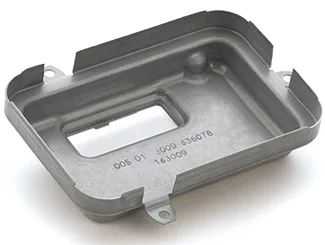
Aunov Tech manufactures the Deep Drawn Aluminum Power Supply in aluminum on a single production floor. In the assembly, the deep drawn part replaces a machined-from-solid body with a lighter, faster drawn shell. One production floor covers forming, finishing and inspection, so the approved sample defines every later batch with no third party in the loop.
Product overview
The critical features of this aluminium component are, the formed envelope, flatness and hole location, all held to the drawing and verified at first article.
The press shop and machine shop that make this aluminium component share one floor, which keeps the sample loop inside our own schedule, and every step is logged against the part number.
How it is manufactured
The route for this aluminium component is fixed and repeatable: Drawing converts a flat blank into the finished envelope in one controlled sequence; secondary machining holds the seats, threads and faces that forming cannot produce.
The power supply chassis tooling and setup record is stored against the part number, so nothing depends on someone remembering. The signed power supply chassis sample remains the reference and is kept with the job file.
Materials and finishing
Standard stock includes carbon steel SPCC / DC01, 304 and 316 stainless, aluminium, brass and copper and this aluminium component runs in aluminium.
The surface treatment is picked to match the service conditions: electrophoresis, powder coating, anodising and zinc / nickel plating. Once approved, the finish for this aluminium component is fixed and does not get re-decided.
Every power supply chassis order keeps its trace back to the approved first article, and a reorder is a repeat rather than a new start. First article, drawing revision and material cert travel with each power supply chassis batch.
Quality control
Production runs under an ISO 9001 certified quality system: stock arrivals are checked against mill certificates, the CMM measures the first article dimension by dimension, and every production run is inspected against the first-article report. The power supply chassis first article is CMM measured – threads gauged to class, diameters on the record. Tests for torque, leakage or pressure can be arranged when the service demands them, and the report is packed with the shipment.
Applications
The aluminium component is fitted into industrial and appliance assemblies under schedules that run for years at a time.
This aluminium component is supplied to several positions in the same machine, so one tooling set serves every position, and the same first article applies throughout.
Customization and options
Options changed most often
Options customers tend to adapt on this aluminium component: material and coating for the duty, wall bands, flange forms, threads and bosses, closed ends and finishes matched to the working environment, and how the order is released – sample, pilot run or scheduled call-off.
Tooled and untooled options for this aluminium component are listed separately, so you can see which options are free and which need new tooling. The power supply chassis quotation states the tooling ownership term explicitly.
Specifications
| Item | Deep Drawn Aluminum Power Supply |
|---|---|
| Brand | AUNOV |
| Designing | Send drawings, or send a sample to be measured – unusual walls, threads or tolerances are feasibility-checked first; changes are priced before they are made. |
| Tooling | Dies, fixtures and gauges are made in our own toolroom, so a die can be re-cut against the approved drawing, and maintenance is tracked against the part number. |
| Samples | Sample parts are measured and reported before submission, so the approved first article becomes the gauge reference, and mass production is gated on that approval. |
| Materials | Materials held include carbon steel, 304 / 316 stainless, aluminium and brass; special grades are sourced to the drawing when volumes justify. |
| Surface finish | Plating, powder coating, anodising or polishing, per the print; alternatives quoted with the quotation, samples approved in writing. |
| Processing | Progressive drawing through several stages, annealed between draws, then trim and pierce; in-process checks sit between stages, not only at the end. |
| Equipment | Mechanical presses from 5 to 250 T and hydraulic presses 250-500 T, with in-line annealing furnaces; secondary ops run on CNC turning centres, inspection on the CMM. |
| Tolerance | +/-0.1 mm general on drawn sections, +/-0.03 mm on machined seats; finer bands confirmed from capability data before quoting. |
| Delivery terms | FOB Ningbo or Shanghai, T/T or L/C, with D/P accepted on repeat business; sea or air freight is quoted to your door. |
Packing and shipment
Finish comes first when packing this aluminium component: interleaving, individual bags or trays are chosen by finish type, in sealed cartons on export pallets, documented and marked to your instruction.