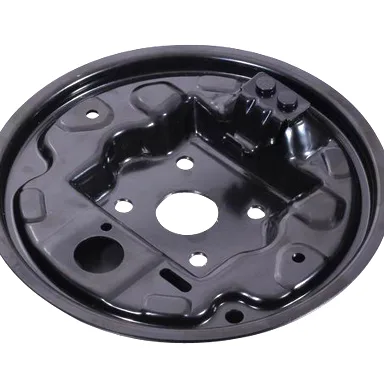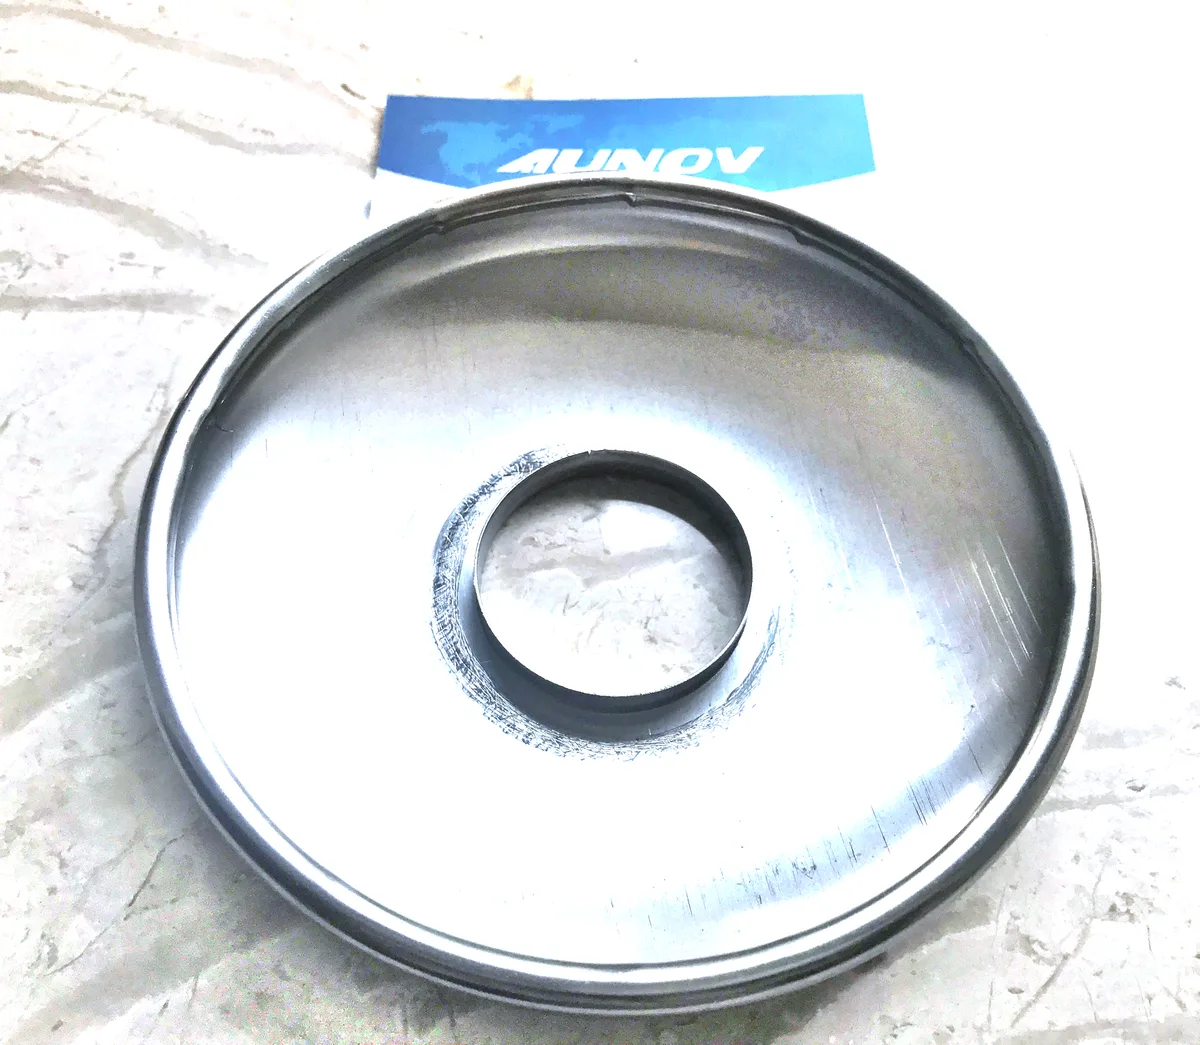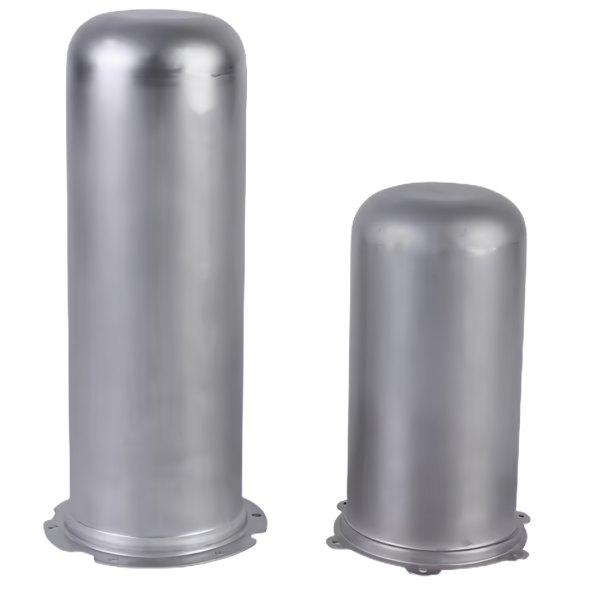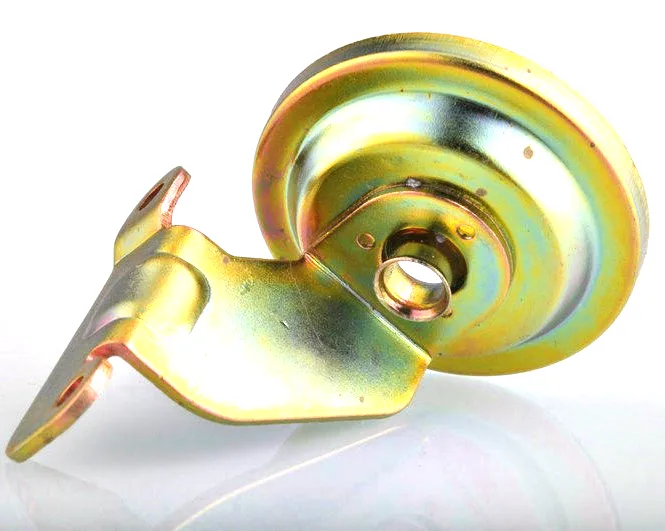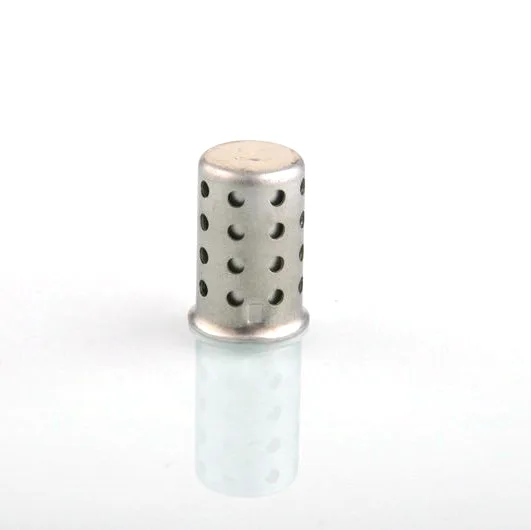
Produced in stainless steel by Aunov Tech, the Custom Stamped Stainless Steel Deep Drawn Filter Cup Perforated Bottom is formed and machined on the same floor. In the assembly, the drawn housing provides a closed, seam-free body the customer builds into. Die work, machining and CMM inspection are all in-house, so first-article dimensions hold through volume batches on one production route.
Product overview
What matters most on this stainless steel component is, wall thickness control, flange geometry and the sealing surface, checked by CMM at first article and by gauge in production.
Die work and machining for this stainless steel component sit on the same floor, so a drawing change is absorbed in one step, and the approved sample is kept as the master.
Production route
Production of this stainless steel component is locked to one route: The drawn envelope is produced in stages with anneals between them; piercing and trimming are done in the same die line.
The ss filter cup manufacturing record is archived together with the drawing revision that produced it. Deviations on the ss filter cup are reported before shipment rather than found on your assembly line.
Materials and finishing
Standard stock includes carbon steel SPCC / DC01, 304 and 316 stainless, aluminium, brass and copper and the grade agreed for this stainless steel component is 304 / 316 stainless steel.
Finish selection follows the working environment: zinc, nickel or chrome plating, anodising, powder coating, electrophoresis and passivation. The agreed finish for this stainless steel component travels with the part number on every reorder.
Repeat ss filter cup orders are measured against the approved sample, so neither material nor finish drifts between lots. The approved ss filter cup sample governs later runs, and any grade change is agreed in writing first.
Quality control
Quality management is certified to ISO 9001: certificates verify each incoming batch of material, the CMM measures the first article dimension by dimension, and production batches are inspected on a sampling plan. For the ss filter cup, cavity depth and seal face finish are checked at first article. Functional testing – torque, leak or pressure – can be written into the plan, and the batch file carries the results.
Where the part is used
You will find this stainless steel component inside industrial machinery and equipment assemblies under schedules that run for years at a time.
This stainless steel component is supplied to several positions in the same machine, so one approved version covers the whole range, without a second tooling round.
Customization and options
The options customers tune most
The options most often changed on this stainless steel component: material and coating for the duty, wall bands, flange forms, threads and bosses, closed ends and finishes matched to the working environment, with orders run as prototypes, pilot lots or scheduled call-offs.
The quote for this stainless steel component separates tooled options from new work, so the effect of a revision on price is clear up front. Quoted ss filter cup prices are firm for the agreed validity window.
Specifications
| Item | Custom Stamped Stainless Steel Deep Drawn Filter Cup Perforated Bottom |
|---|---|
| Brand | AUNOV |
| Designing | Send drawings, or send a sample to be measured – DFM notes are returned before any tooling is cut; the agreed version governs every later batch. |
| Tooling | Dies are maintained by stroke count, so tooling condition does not drift mid-order. |
| Samples | Samples are produced on the production tooling, so what you approve is what you get. |
| Materials | Stock covers carbon steel (SPCC / DC01), 304 / 316 stainless, aluminium and brass; special grades are sourced to the drawing when volumes justify. |
| Surface finish | Finish selected from the drawing: plating, coating, anodising or passivation; masking and laser marking available where needed. |
| Processing | Multi-stage deep drawing with interstage annealing, trimmed and pierced in following dies; first articles verify the whole flow before the run is released. |
| Equipment | Mechanical presses from 5 to 250 T and hydraulic presses 250-500 T, with in-line annealing furnaces, with in-house toolmaking to keep dies and fixtures maintained. |
| Tolerance | +/-0.05 mm to +/-0.1 mm across the part, wall thickness held to print; GD&T per drawing, PPAP-style reports on request. |
| Delivery terms | FOB, CIF or DDP per Incoterms 2020, payment by T/T, L/C at sight or D/P; sea or air freight is quoted to your door. |
Packaging and delivery
Finish comes first when packing this stainless steel component: each coating gets its own packing – interleaves, bags or trays, then cartons are sealed and palletised, with marks and documents as you specify.