
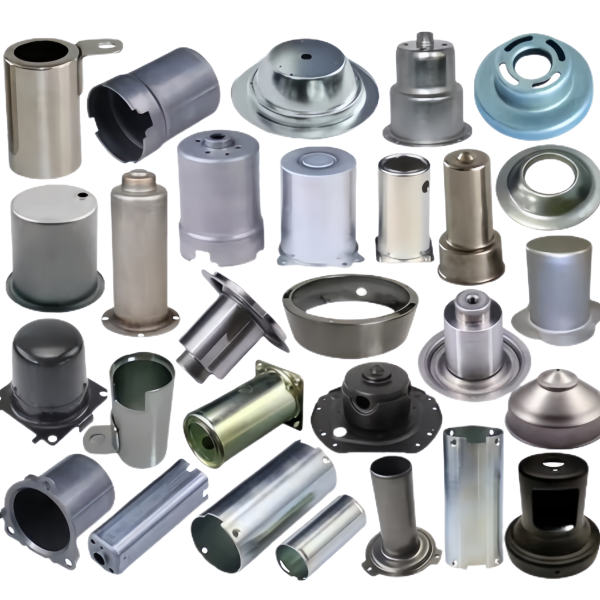
The Assorted Deep Drawn Shells and Sensor Cups are thin-wall drawn cylinders whose only job is to house a sensor, a transducer or a small mechanism, and their shared problem is that thin walls go out of round the moment the draw is not perfect. Because they are quoted as an assortment, the engineering below covers grouping them by draw depth, drawing the thin wall without sinking the base, and holding the sensor seat that the assembly actually reads against.
Grouping sensor cups by draw depth and wall spec
An assortment of sensor cups is really several draw depths sharing one wall spec, and we group them by depth before we touch steel, because a 20 mm deep cup and an 80 mm deep cup need different stage plans even at the same 0.5 mm wall. We bracket the assortment into shallow (under 30 mm), medium (30-60 mm) and deep (over 60 mm) and assign each bracket its own redraw schedule, so a shallow cup is not forced through a deep-cup die that would wrinkle its wall.
Within each depth bracket we group by wall thickness – 0.4 mm, 0.5 mm, 0.6 mm – because the punch and die clearance changes with wall and the same die cannot hold roundness across a 0.2 mm wall swing. The result is a set of mini-runs, each with a documented stage plan, and the carton is labelled by depth and wall so the reorder pulls the right one.
- Bracket by depth: shallow under 30 mm, medium 30-60 mm, deep over 60 mm.
- Group by wall: 0.4, 0.5, 0.6 mm; do not mix across a die.
- Label the carton by depth and wall so the reorder matches the stage plan.
Grouping also drives the quotation honestly. A deep, 0.4 mm cup costs more per piece than a shallow, 0.6 mm one because it needs an extra redraw and an anneal, and quoting them as one blended price hides that from both sides. We price per depth-and-wall group so the customer sees why the thin deep cup costs what it does, and so a later change to one group does not reprice the others. The assortment is one order to ship but several processes to plan.
Drawing thin-wall sensor shells without sinking the base
A 0.5 mm wall drawn to 80 mm deep is on the edge of what a single redraw will hold, and the failure is the sunk base – the bottom pulls down into a cone because the wall ironed faster than the base could feed. We draw thin sensor shells in three stages with a 40/30/10 reduction plan and an anneal between stages when the cumulative reduction passes 20 percent, because 304 stainless steel at 0.5 mm work-hardens fast and an unrelieved third stage sinks the base every time.
The base corner radius is opened to 5x the wall – 2.5 mm on a 0.5 mm shell – because a tight radius on thin stock is the surest way to split the base. We hold the base at the stock thickness and let the wall thin to 0.48 mm in the iron, so the base stays the strongest part of the shell instead of the weakest.
- Three stages at 40/30/10 percent; anneal past 20 percent cumulative.
- Base corner radius 5x wall (2.5 mm at 0.5 mm) to stop a base split.
- Hold the base at stock thickness; let only the wall iron.
Material choice for sensor cups that must read clean
304 stainless steel is the default for sensor cups because it draws thin, takes no coating, and does not contaminate the sensor with zinc or outgas like some plastics. Where the cup must be non-magnetic so it does not bias the sensor we use 316L, which draws almost identically to 304 but is austenitic and stays non-magnetic through the draw. We avoid plated mild steel for sensor cups that read a signal, because any coating thickness variation between cups shifts the sensor’s calibration.
Finish on stainless steel is a passivation only, at most a light electropolish where the cup faces a fluid, because anything thicker than a micron changes the dielectric the sensor sees. We state on the quotation that sensor cups are supplied clean and passivated, never coated, unless the signal budget allows it.
- 304 default; 316L where the cup must stay non-magnetic.
- Avoid plated steel for signal-reading cups; coating variation shifts calibration.
- Passivate only, or light electropolish; never coat a sensor cup.
Holding the sensor seat and lead-exit position
The sensor seat – the internal shoulder or the locating diameter the sensor presses into – is the cup’s true functional feature, so it is machined after drawing to +/-0.03 mm and held round within 0.03 mm TIR. The lead-exit hole, where the cable or pin leaves the cup, is pierced or machined to +/-0.1 mm from the seat axis, because a lead that exits off-position stresses the cable and reads as a failure in the field.
We machine the seat and the exit in one set-up indicated off the trimmed mouth, so the seat is square to the cup axis instead of to the drawn wall. The seat is air-gauged in production because a seat that goes 0.05 mm out of round is the hidden cause of a sensor that rattles and drifts in its reading.
- Sensor seat machined to +/-0.03 mm, round 0.03 mm TIR, after drawing.
- Lead exit +/-0.1 mm from seat axis; machined in the same set-up.
- Indicate off the trimmed mouth so the seat is square to the axis.
The lead-exit is often the feature customers forget to tolerance, and an untoleranced exit is where we get a cable that kinks at the cup. We ask for the exit position and the cable diameter at the quote and machine the exit to clear the cable by 0.3 mm minimum, because a tight exit chafes the cable and a loose one lets the cable pivot and pull the sensor off its seat. The exit is deburred on both faces so the cable jacket is not cut on insertion.
Where thin sensor cups go out of round and why
A thin sensor cup goes out of round for two reasons, and both show at the mouth or the seat. Uneven wall from a worn redraw die makes the cup oval at the mouth, because the wall that is thin on one side springs differently than the thick side; we map wall thickness at first article and catch it before the run. The second cause is a trim that was not square, which puts the mouth on a bias and the seat reads off-axis even though the bore is round; we trim to +/-0.1 mm and gauge the mouth squareness.
We keep a reference cup on the board showing a 0.1 mm out-of-round mouth next to an in-spec one, so the operator reads the difference by feel before it becomes a rejected lot. A cup that is 0.1 mm out at the seat is a sensor that drifts by that amount in its reading – unacceptable for a measurement device.
- Map wall thickness at first article; a worn redraw die ovals the mouth.
- Trim square to +/-0.1 mm so the seat does not read off-axis.
- Compare every first part to the reference cup before releasing the run.
How we verify assorted shells and sensor cups
An assortment of sensor cups is verified at first article per depth-and-wall group for the features that carry the signal – seat roundness, wall map and lead-exit position – and then gauged for seat and mouth roundness in production because the thin draw is the only thing that drifts late.
- First article: CMM on seat roundness and diameter, wall-thickness map at eight points, lead-exit position, plus a material certificate and a passivation record.
- Production: air gauge on the seat every run, ring gauge on mouth roundness, wall sample, and a visual on the base for sink on the first and last cup.
- Shipment file: dimensional report, wall and seat records, passivation cert, and material cert travel under your part number.
The draw dies and seat tooling are built and held in our own toolroom against your part number, with the redraw clearance and seat setting archived by depth and wall so a reorder reproduces the roundness. A reorder is a draw run, a seat machine pass and a gauge check, not a new development.
Drawing, machining and welding each win on different geometries; the guide to deep drawn covers works through those boundaries, and the full Precision Deep Drawn Parts range is reachable from the overview page.
Specifications
| Item | Assorted Deep Drawn Shells and Sensor Cups |
|---|---|
| Brand | AUNOV |
| Designing | Send the drawing, or a cup sample we can measure, you get a DFM review together with the quotation. |
| Tooling | Tooling designed and cut in house, held under your part number. |
| Samples | First-article samples of the cup ship with a full dimensional report and mill certificate. |
| Materials | The stock list runs carbon steel (SPCC / DC01), 304 / 316 stainless steel, aluminium, brass and copper, and the grade is fixed at the drawing review. |
| Surface finish | Surface treatment per the drawing: plating, e-coat, powder coating, anodising, passivation, per the drawing. |
| Processing | Deep drawing in stages, in-line annealing where needed, then pierced and machined in house. |
| Equipment | Our press floor runs 5-250 T mechanical and 250-500 T hydraulic presses, CNC cells plus a temperature-controlled CMM room. |
| Tolerance | Drawn tolerances held to +/-0.1 mm, +/-0.03 mm on machined surfaces. |
| Delivery terms | FOB is standard; DDP offered for EU and US, T/T or L/C, D/P on repeat business, call-off scheduling supported. |
Frequently Asked Questions
Why is the assortment grouped by draw depth before anything else?
A shallow cup and a deep cup need different stage plans even at the same wall thickness, and forcing a shallow part through a deep-cup die wrinkles its wall. We bracket the family by depth and assign each bracket its own redraw schedule, which is also what keeps the thin members of the set from sinking at the base.
Why can one die set not serve several wall thicknesses?
Punch and die clearance is set for a wall thickness, and the same tooling will not hold roundness across a meaningful swing in that dimension. Within each depth bracket we sub-group by wall so every member of a mini-run sees the clearance it was dimensioned for.
What goes wrong with the thinnest, deepest cups in a set?
They go out of round, and they do it for a structural reason: a deep thin wall has very little hoop stiffness, so it loses its circle to handling and to the residual stress of the last redraw rather than to a forming defect. Length-to-diameter and the final stage plan together decide whether a given member survives shipping.
How is a reorder kept identical to the first run?
Each mini-run ships against a documented stage plan, and the carton is labelled by depth and wall so the reorder pulls the correct one. A reorder therefore starts from recorded settings rather than from a retune, which is the difference between a repeat part and a new development.
Related Products


Request a Quote for This Part
Send a drawing or sketch — get material advice, tooling cost and a per-piece price within 24 hours (working days).