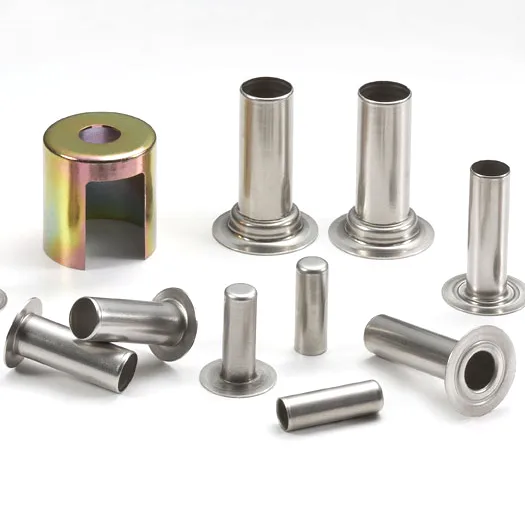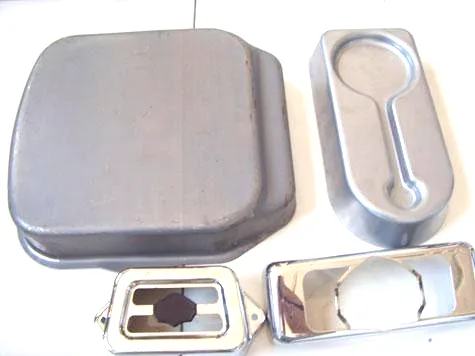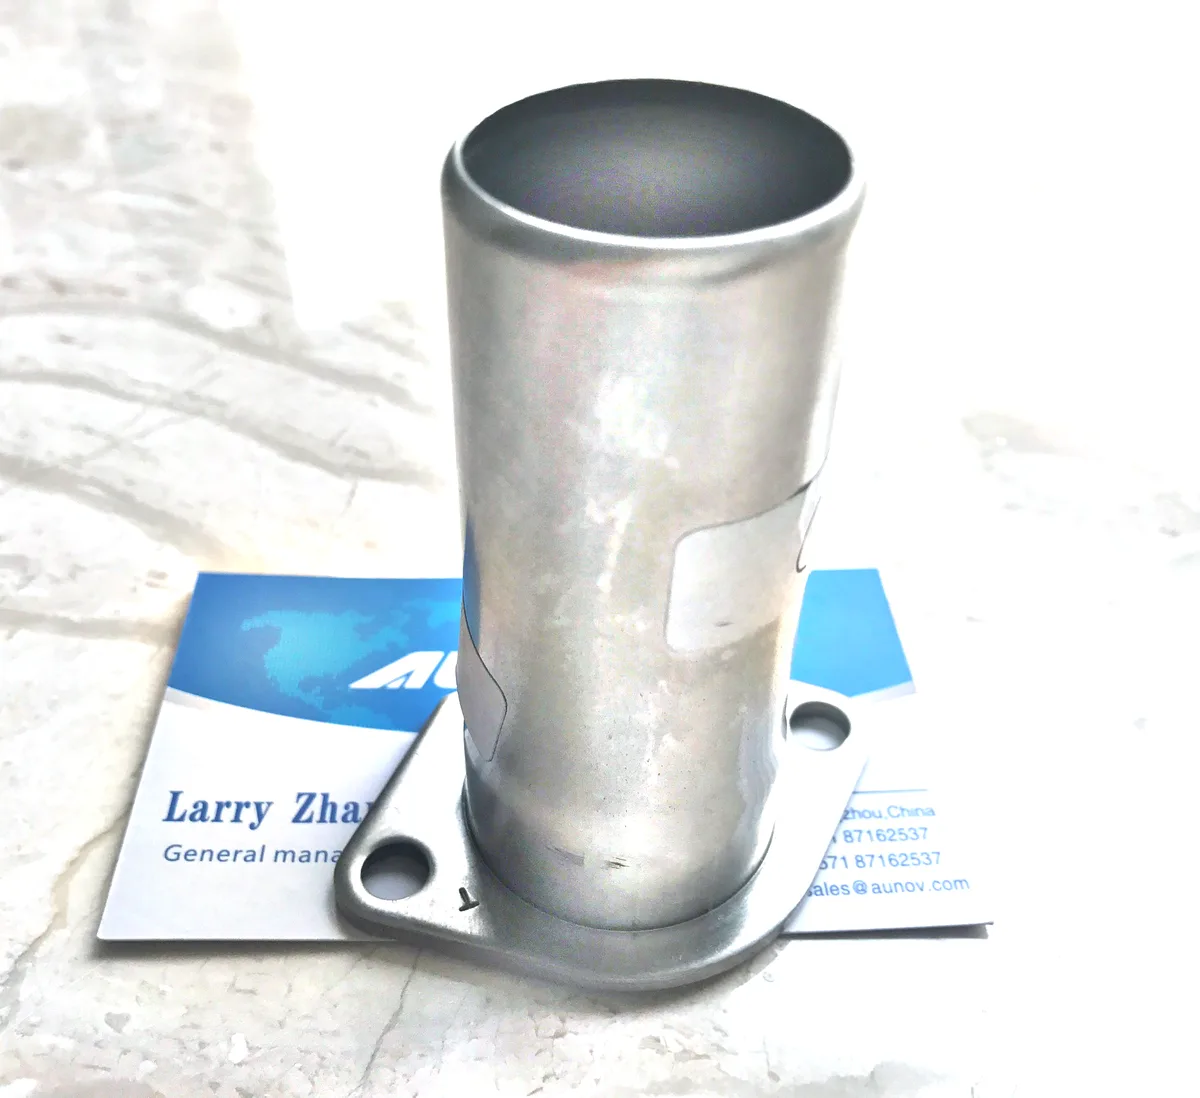
Aunov Tech manufactures the Hydroformed Camera Housing in stainless steel on a single production floor. On the product, the drawn housing encloses the sensitive internals and carries the mounting interface. Die work, machining and CMM inspection are all in-house, so repeat orders stay aligned with the approved sample without re-quoting the job elsewhere.
Product overview
For this metal housing, the drawing centres on, wall thinning, concentricity and the finished mating faces, controlled from the approved first article onward.
Die building, pressing and machining for this metal housing are all in house, so revisions do not wait on outside suppliers, with process data archived for repeat orders.
How it is manufactured
This is how the metal housing is built: The preform is hydroformed to the finished contour under high pressure; the die contour is maintained against the approved first article.
Each can shipment is verified against the master sample before it leaves the shop. The signed can sample remains the reference and is kept with the job file.
Materials and finishing
The standard stock list carries cold-rolled steel (SPCC / DC01), 304 / 316 stainless, aluminium, brass, copper and bronze and this metal housing runs in carbon steel or stainless.
The finish is chosen for the duty it will see: zinc, nickel or chrome plating, anodising, powder coating, electrophoresis and passivation. It is fixed on the drawing for this metal housing, so repeat orders never reopen the question.
Batch records for the can are filed against the part number, so process settings are reused instead of re-invented. The signed can sample remains the reference and is kept with the job file.
Quality control and inspection
An ISO 9001 certified system governs production: mill certificates cover every delivery of stock, a full CMM report approves the first article, and production batches are inspected on a sampling plan. For the can, cavity depth and seal face finish are checked at first article. If the assembly calls for torque, leak or pressure proof, the test is built into the quality plan, and the inspection report ships with each batch.
Applications
Typical installation of the metal housing is in industrial equipment and general assembly work for OEM and Tier-1 customers.
A single design of this metal housing is often reused across a product family, so the specification is set by the toughest of them, and approvals carry across programmes.
Customization and options
Options changed most often
Variations that come up most often on this metal housing: material grade, wall band, flange shape, thread size and finish for the working environment, with orders run as prototypes, pilot lots or scheduled call-offs.
Each quote for this metal housing states which variations are already tooled, so you can see which options are free and which need new tooling. Nothing is implied – on tooling, the quotation is the contract for the can.
Specifications
| Item | Hydroformed Camera Housing |
|---|---|
| Brand | AUNOV |
| Designing | Your drawing sets the part – samples are reverse-measured into a controlled drawing; the same drawing is used for every repeat order. |
| Tooling | Tooling is built and held under your part number, so tooling lead time stays under our control, and maintenance is tracked against the part number. |
| Samples | Sample parts are measured and reported before submission, so the approved first article becomes the gauge reference, and mass production is gated on that approval. |
| Materials | Stock covers carbon steel (SPCC / DC01), 304 / 316 stainless, aluminium and brass; special grades are sourced to the drawing when volumes justify. |
| Surface finish | Plating, powder coating, anodising or polishing, per the print; finish thickness and adhesion checked on the first article. |
| Processing | Multi-stage deep drawing with interstage annealing, trimmed and pierced in following dies; in-process checks sit between stages, not only at the end. |
| Equipment | Press shop running 5-250 T mechanical and 250-500 T hydraulic presses, annealing ovens on site; first articles and batch samples are checked on the CMM. |
| Tolerance | +/-0.1 mm general on drawn sections, +/-0.03 mm on machined seats; GD&T per drawing, PPAP-style reports on request. |
| Delivery terms | CIF or DDP, with FOB available, T/T or L/C, with D/P accepted on repeat business; call-off schedules are supported. |
Packaging and delivery
Packaging protects the finished surfaces of this metal housing: the coating decides whether parts are interleaved, bagged or tray-packed, then cartons are sealed and palletised, with marks and documents as you specify.