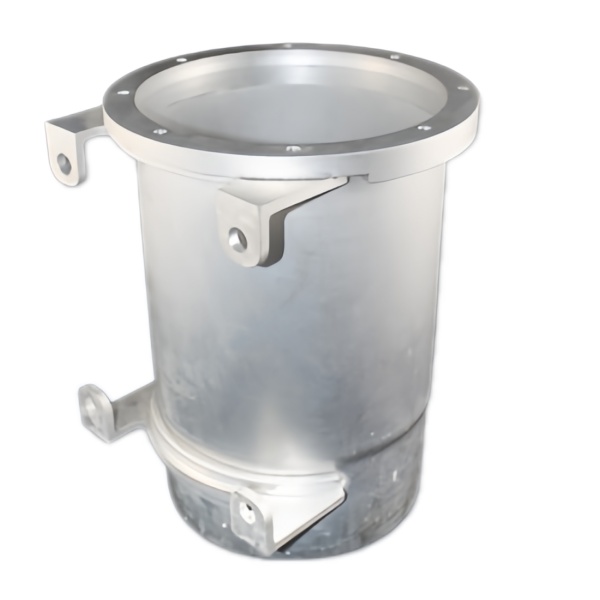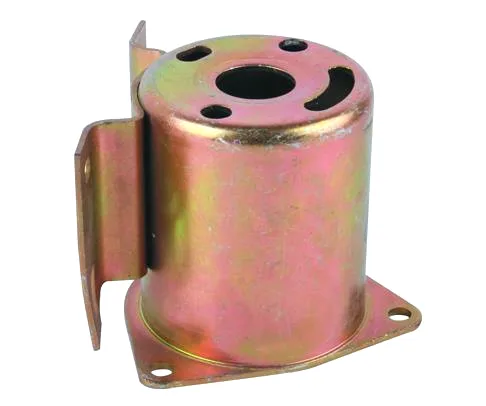
The Custom Deep Drawn Sheet Metal Deep Drawing Stator Motor Housing is produced by Aunov Tech from stainless steel, formed and finished under one roof. On the product, the drawn housing encloses the sensitive internals and carries the mounting interface. One production floor covers forming, finishing and inspection, so repeat orders stay aligned with the approved sample with no third party in the loop.
Product overview
This metal housing is defined by, draw depth, wall band and the surfaces that forming cannot hold, each measured at first article and gauged on production batches.
Toolroom, presses and machining centres used on this metal housing operate on the same site, so revisions do not wait on outside suppliers, and every step is logged against the part number.
Production route
Production of this metal housing is locked to one route: Drawing converts a flat blank into the finished envelope in one controlled sequence; threads are single-pointed or rolled and seats bored in one setup where possible.
A stator motor housing looks like the simplest item in a catalogue and is often the most demanding to make consistently. Our answer on the stator motor housing is process control: fixed setups, recorded parameters and sampling through the run.
Materials and finishing
Everything is drawn from a fixed stock list: carbon steel SPCC / DC01, 304 and 316 stainless, aluminium, brass and copper with this metal housing costed in carbon steel or stainless.
The surface treatment is picked to match the service conditions: zinc and nickel plating, chrome, anodising, powder coating and passivation. The finish on this metal housing is locked to the drawing revision, so later orders match.
Batch records for the stator motor housing are filed against the part number, so process settings are reused instead of re-invented. That record is what every stator motor housing reorder is built on, so nothing changes silently between shipments.
Quality control
Production runs under an ISO 9001 certified quality system: material traceability starts with mill certificates, first articles are measured on a CMM, and production batches are inspected on a sampling plan. Cavity depth and seal face finish on the stator motor housing are verified at first article. Where the application asks for it, torque, leak or pressure testing is added to the plan, and the inspection report ships with each batch.
Applications
Typical installation of the metal housing is in industrial and appliance assemblies in both OEM and aftermarket supply.
A single design of this metal housing is often reused across a product family, so wall bands and finishes are selected to cover the widest duty, and the same first article applies throughout.
Options and variations
Options that vary most in this stator motor housing family
Commonly varied points: material and finish for the environment, draw depths, flange and thread features, vent holes, sealed exits and finishes matched to the environment, and batch size from first prototypes to call-off schedules.
The quotation separates what existing tooling already covers from what a change would add, keeping the trade-offs visible from the start.
Specifications
| Item | Custom Deep Drawn Sheet Metal Deep Drawing Stator Motor Housing |
|---|---|
| Brand | AUNOV |
| Designing | Your drawing sets the part – unusual walls, threads or tolerances are feasibility-checked first; the approved drawing is kept as the controlled master. |
| Tooling | Tooling is built and held under your part number, so no tooling step is outsourced, and the die remains dedicated to your part. |
| Samples | Pre-production samples come with a full inspection report, so the approved first article becomes the gauge reference, and production starts only after your written sign-off. |
| Materials | Stock runs to carbon steel, 304 / 316 stainless, aluminium and brass; material substitutes are proposed only with your written approval. |
| Surface finish | Natural, plated or coated – the print decides, and the agreed finish is logged; alternatives quoted with the quotation, samples approved in writing. |
| Processing | Deep drawing on maintained presses, blank size and lubrication logged per run; batch records are filed so a repeat order starts from approved data. |
| Equipment | Mechanical presses 5-250 T plus 250-500 T hydraulics, with in-line annealing, with CNC turning centres for secondary operations and CMM inspection. |
| Tolerance | +/-0.05 mm on drawn diameters, tighter bands confirmed against the drawing; capability is checked on the first article before the run continues. |
| Delivery terms | FOB Ningbo or Shanghai, payment by T/T, L/C at sight or D/P; each volume tier carries its own quoted price. |
Packaging and delivery
Packing for this metal housing is chosen around the coating: interleaving, bagging or tray packing is matched to the surface, in sealed cartons on export pallets; shipping documents and carton marks follow your instructions.