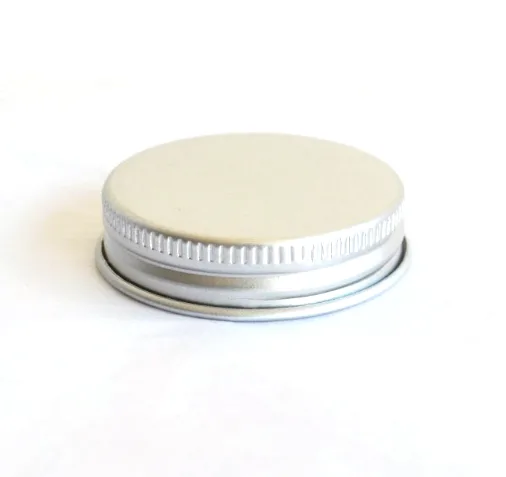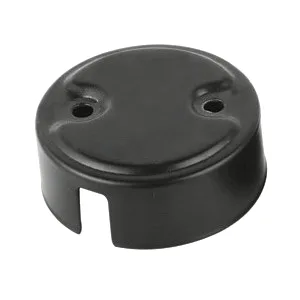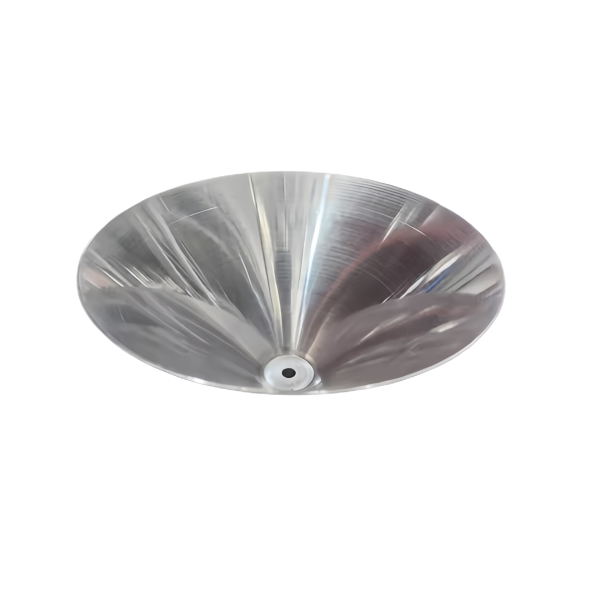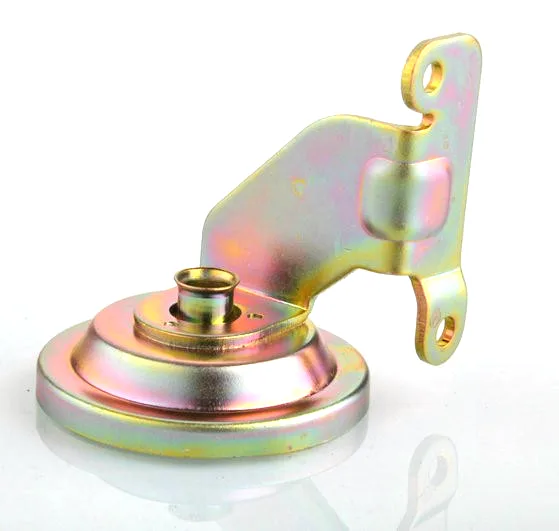
Produced in carbon steel by Aunov Tech, the Carbon Steel Deep Drawn Metal Stamped Part Stamping Parts With Zinc is formed and machined on the same floor. In service, the deep drawn part carries the formed geometry the assembly needs at volume. Forming, machining and inspection share one floor, so first-article dimensions hold through volume batches on one production route.
Product overview
The critical features of this carbon steel component are, draw depth, wall band and the surfaces that forming cannot hold, controlled from the approved first article onward.
Die building, pressing and machining for this carbon steel component are all in house, so feasibility questions are answered on the shop floor, with the tooling history retained in house.
Production route
Every carbon steel component follows the same routed path: The shell starts as coil or blank and is drawn through single and progressive dies; after drawing, critical faces are machined and the part is degreased and gauged.
The -plated pivot bracket manufacturing record is archived together with the drawing revision that produced it. Deviations on the -plated pivot bracket are reported before shipment rather than found on your assembly line.
Materials and finishing
Materials kept on the floor cover SPCC / DC01 carbon steel, 304 / 316 stainless, aluminium, brass, copper and bronze and the grade agreed for this carbon steel component is cold-rolled carbon steel.
The finish is chosen for the duty it will see: zinc and nickel plating, chrome, anodising, powder coating and passivation. The agreed finish for this carbon steel component travels with the part number on every reorder.
Production batches of the -plated pivot bracket are gauged back to the signed first article, not to a memory of it. Any change to the -plated pivot bracket drawing is re-approved and re-verified before production continues.
Quality control
Quality management is certified to ISO 9001: incoming material is verified against mill certificates, the CMM measures the first article dimension by dimension, and routine sampling keeps batches aligned with the first article. For the -plated pivot bracket, first articles are CMM measured and threads are gauged to class. Functional testing – torque, leak or pressure – can be written into the plan, and the report is packed with the shipment.
Applications
This carbon steel component is used in industrial machinery and equipment assemblies in volume programmes as well as aftermarket supply.
Drawings for this carbon steel component are adapted across programmes, so wall bands and finishes are selected to cover the widest duty, and approvals carry across programmes.
Customization and options
What customers usually vary
The parts of the print for this carbon steel component that get adjusted: material and coating for the duty, wall bands, flange forms, threads and bosses, closed ends and finishes matched to the working environment, and the batch pattern – prototype, pilot lot or scheduled production.
Options for this carbon steel component already covered by the die are shown on the quote, so you are not charged twice for a feature the die already makes. The -plated pivot bracket drawing revision, once signed, governs all later batches.
Specifications
| Item | Carbon Steel Deep Drawn Metal Stamped Part Stamping Parts With Zinc |
|---|---|
| Brand | AUNOV |
| Designing | Made to your 2D/3D drawings (PDF, DWG, STEP, IGS) – samples are reverse-measured into a controlled drawing; the agreed version governs every later batch. |
| Tooling | Die design and toolmaking stay in house, so no tooling step is outsourced, and first-article timing is measured from the tooling start date. |
| Samples | Prototype and pre-production samples are provided against the drawing, so the approved first article becomes the gauge reference, and the signed sample is kept for future reorders. |
| Materials | SPCC / DC01 cold-rolled carbon steel, 0.5-3.0 mm, the standard stock for formed component; pickled (SPHC) or galvanised alternatives. |
| Surface finish | Natural, plated or coated – the print decides, and the agreed finish is logged; finish thickness and adhesion checked on the first article. |
| Processing | Die stamping with in-press forming and piercing; every stage is logged against your part number. |
| Equipment | Press shop with 5-250 T mechanical presses and dedicated dies; secondary ops run on CNC turning centres, inspection on the CMM. |
| Tolerance | +/-0.03 mm on pierced holes, +/-0.1 mm on formed sections; critical dimensions carry CMM data with the shipment. |
| Delivery terms | Terms are FOB by default, with CIF and DDP quoted on request and freight priced to your door. |
Packaging and delivery
For this carbon steel component, protection starts at the surface: interleaving, bagging or tray packing is matched to the surface, then sealed cartons are palletised for export, with documents and marks to your instruction.