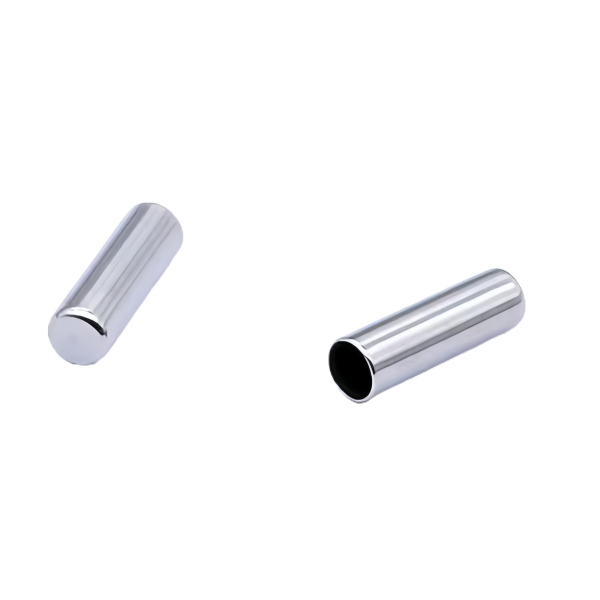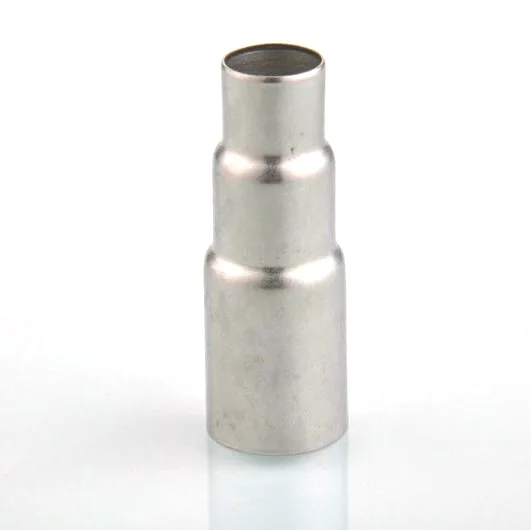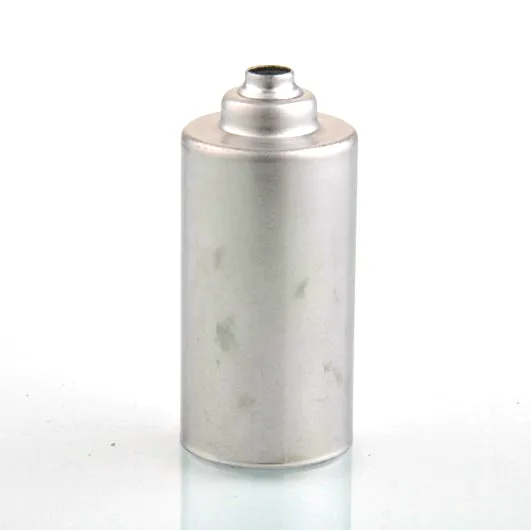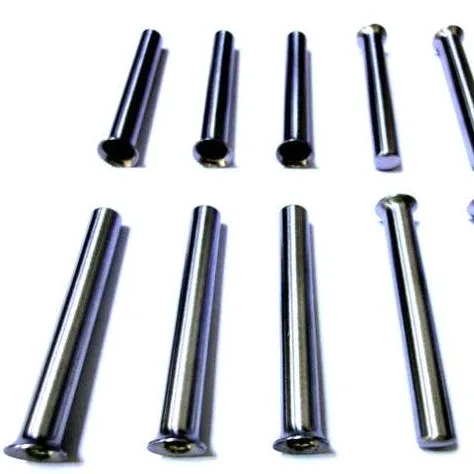
The Oxygen sensor housing is produced by Aunov Tech from stainless steel, formed and finished under one roof. In service, the sensor housing carries the active element while passing the signal through a sealed exit. The same floor forms, machines and inspects the part, which keeps tolerances consistent from sample to volume under one roof.
Product overview
For this metal sensor, the drawing centres on, draw depth, wall band and the surfaces that forming cannot hold, audited against the approved sample at each production release.
Tooling and finishing for this metal sensor run under one roof, so revisions do not wait on outside suppliers, and the approved sample is kept as the master.
How it is manufactured
Production follows a defined route: Drawing runs from flat blank to finished envelope in one controlled sequence; flanges and rims are formed in the same line, then trimmed to length.
Production batches of the oxygen sensor housing are gauged back to the signed first article, not to a memory of it. That record is what every oxygen sensor housing reorder is built on, so nothing changes silently between shipments.
Materials and finishing
Working stock covers cold-rolled steel (SPCC / DC01), 304 / 316 stainless, aluminium, brass, copper and bronze with carbon steel or stainless specified on the drawing for this metal sensor.
The finish is chosen for a clean working surface: plating, anodising, powder coating, electrophoresis and passivation. It is fixed on the drawing for this metal sensor, so repeat orders never reopen the question.
Every oxygen sensor housing order keeps its trace back to the approved first article, and a reorder is a repeat rather than a new start. First article, drawing revision and material cert travel with each oxygen sensor housing batch.
Quality control
Production runs under an ISO 9001 certified quality system: certificates verify each incoming batch of material, a full CMM report approves the first article, and every production run is inspected against the first-article report. Threads are gauged and seal faces inspected on each oxygen sensor housing batch. Torque, leak and pressure tests are available where the assembly needs them, and results travel with the batch paperwork.
Applications
Typical installation of the metal sensor is in thermal sensing and appliance control assemblies for customers who own the drawing and the tooling.
One drawing for this metal sensor is commonly applied to several programmes, so wall bands and finishes are selected to cover the widest duty, and the die does not have to change.
Specifications
| Item | Oxygen sensor housing |
|---|---|
| Brand | AUNOV |
| Designing | Send drawings, or send a sample to be measured – samples are reverse-measured into a controlled drawing; changes are priced before they are made. |
| Tooling | Tooling is quoted once and held – reorders are priced on the part, not on the die. |
| Samples | Pre-production samples come with a full inspection report, so the approved first article becomes the gauge reference, and production starts only after your written sign-off. |
| Materials | Materials held include carbon steel, 304 / 316 stainless, aluminium and brass; special grades are sourced to the drawing when volumes justify. |
| Surface finish | Plating, powder coating, anodising or polishing, per the print; the finish is inspected with the dimensional report on the first article. |
| Processing | Drawn shell with machined seats and threads where the print calls for them; batch records are filed so a repeat order starts from approved data. |
| Equipment | Press line for drawing, CNC cells for finishing, backed by CNC turning centres and a climate-controlled inspection room. |
| Tolerance | +/-0.02 mm on machined seats, sealing faces flat to drawing; finer bands confirmed from capability data before quoting. |
| Delivery terms | FOB, CIF or DDP per Incoterms 2020, T/T with deposit and L/C for larger runs; each volume tier carries its own quoted price. |