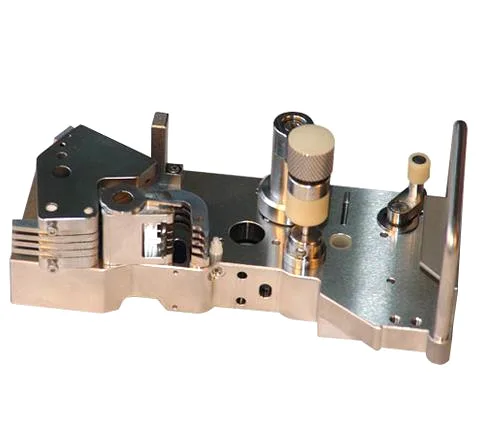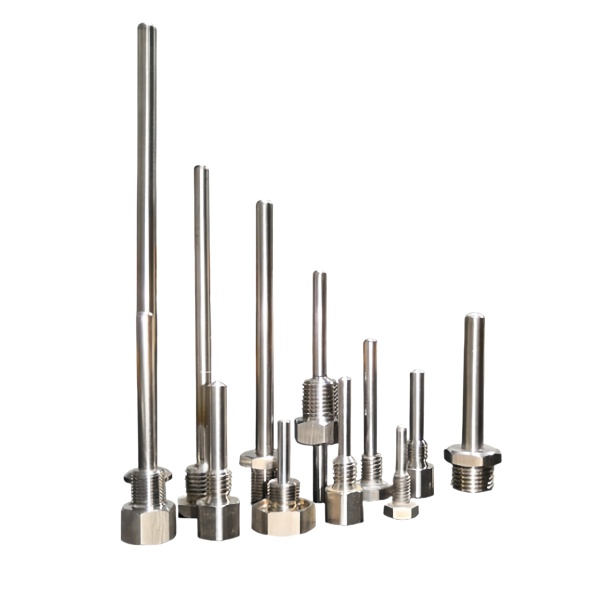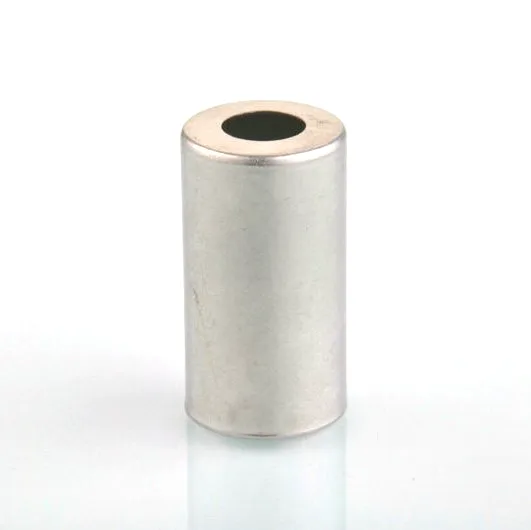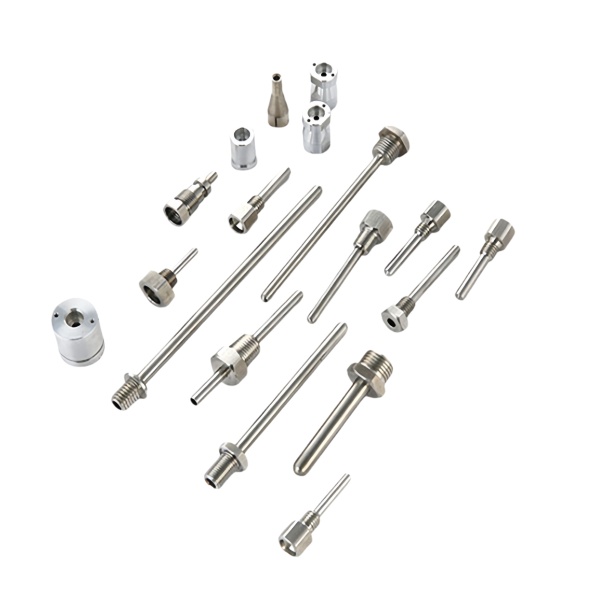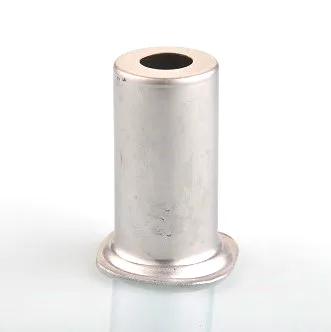
Produced in stainless steel by Aunov Tech, the deep drawing sensor housings is formed and machined on the same floor. Once installed, the sensor housing protects the electronics from vibration, fluid and electromagnetic noise. One production floor covers forming, finishing and inspection, and a design change is re-sampled in one place without a second supplier involved.
Product overview
The drawing for this metal sensor fixes, wall thickness control, flange geometry and the sealing surface, checked by CMM at first article and by gauge in production.
The whole route from die to finished metal sensor stays in house, so feasibility questions are answered on the shop floor, with the tooling history retained in house.
From coil to finished part
Production follows a defined route: Drawing converts a flat blank into the finished envelope in one controlled sequence; after drawing, critical faces are machined and the part is degreased and gauged.
The deep drawing sensor manufacturing record is archived together with the drawing revision that produced it. Deviations on the deep drawing sensor are reported before shipment rather than found on your assembly line.
Materials and surface finish
Standard stock includes carbon steel SPCC / DC01, 304 and 316 stainless, aluminium, brass and copper and this metal sensor runs in carbon steel or stainless.
With the working face exposed, the finish is selected for cleanliness: plating, anodising, powder coating, electrophoresis and passivation. Once approved, the finish for this metal sensor is fixed and does not get re-decided.
Each shipment is verified against the master sample, so material and finish stay consistent between shipments.
Quality control
Production runs under an ISO 9001 certified quality system: stock arrivals are checked against mill certificates, a full CMM report approves the first article, and every production run is inspected against the first-article report. On the deep drawing sensor, thread gauging and seal face inspection run on every batch. Where the application asks for it, torque, leak or pressure testing is added to the plan, with certificates included in the shipment file.
Applications
The metal sensor is fitted into sensor and thermostat assemblies for OEM and Tier-1 customers.
A single design of this metal sensor is often reused across a product family, so one tooling set serves every position, and approvals carry across programmes.
Specifications
| Item | deep drawing sensor housings |
|---|---|
| Brand | AUNOV |
| Designing | Made to your 2D/3D drawings (PDF, DWG, STEP, IGS) – DFM notes are returned before any tooling is cut; the agreed version governs every later batch. |
| Tooling | Die design and toolmaking stay in house, so die cost stays transparent, and first-article timing is measured from the tooling start date. |
| Samples | Production does not start until the sample report has been signed off. |
| Materials | Standard stock: carbon steel (SPCC / DC01), 304 / 316 stainless, aluminium, brass; the final grade is fixed with the drawing review. |
| Surface finish | Plating, coating or polishing to suit the drawing; finish thickness and adhesion checked on the first article. |
| Processing | Drawn shell with machined seats and threads where the print calls for them; batch records are filed so a repeat order starts from approved data. |
| Equipment | Deep drawing presses plus CNC turning centres for machined faces; first articles and batch samples are checked on the CMM. |
| Tolerance | +/-0.01 mm on sealing faces, +/-0.05 mm on drawn profiles; critical dimensions carry CMM data with the shipment. |
| Delivery terms | FOB, CIF or DDP per Incoterms 2020, T/T with deposit and L/C for larger runs; each volume tier carries its own quoted price. |