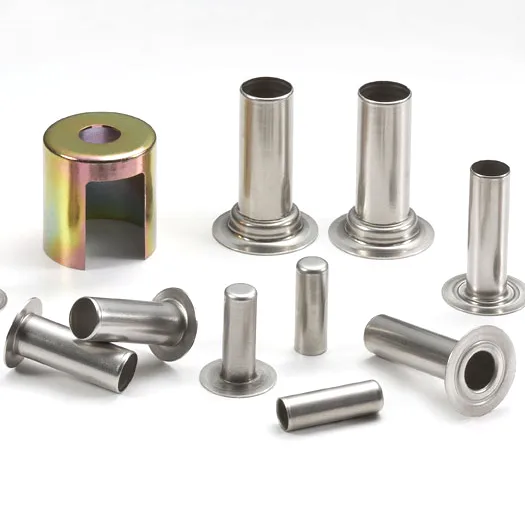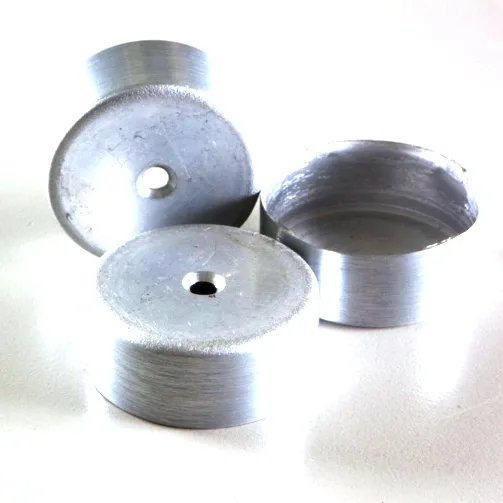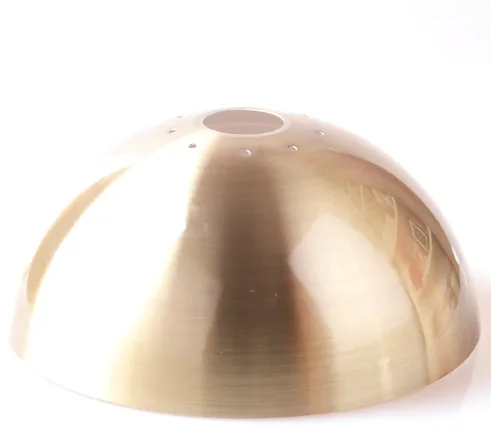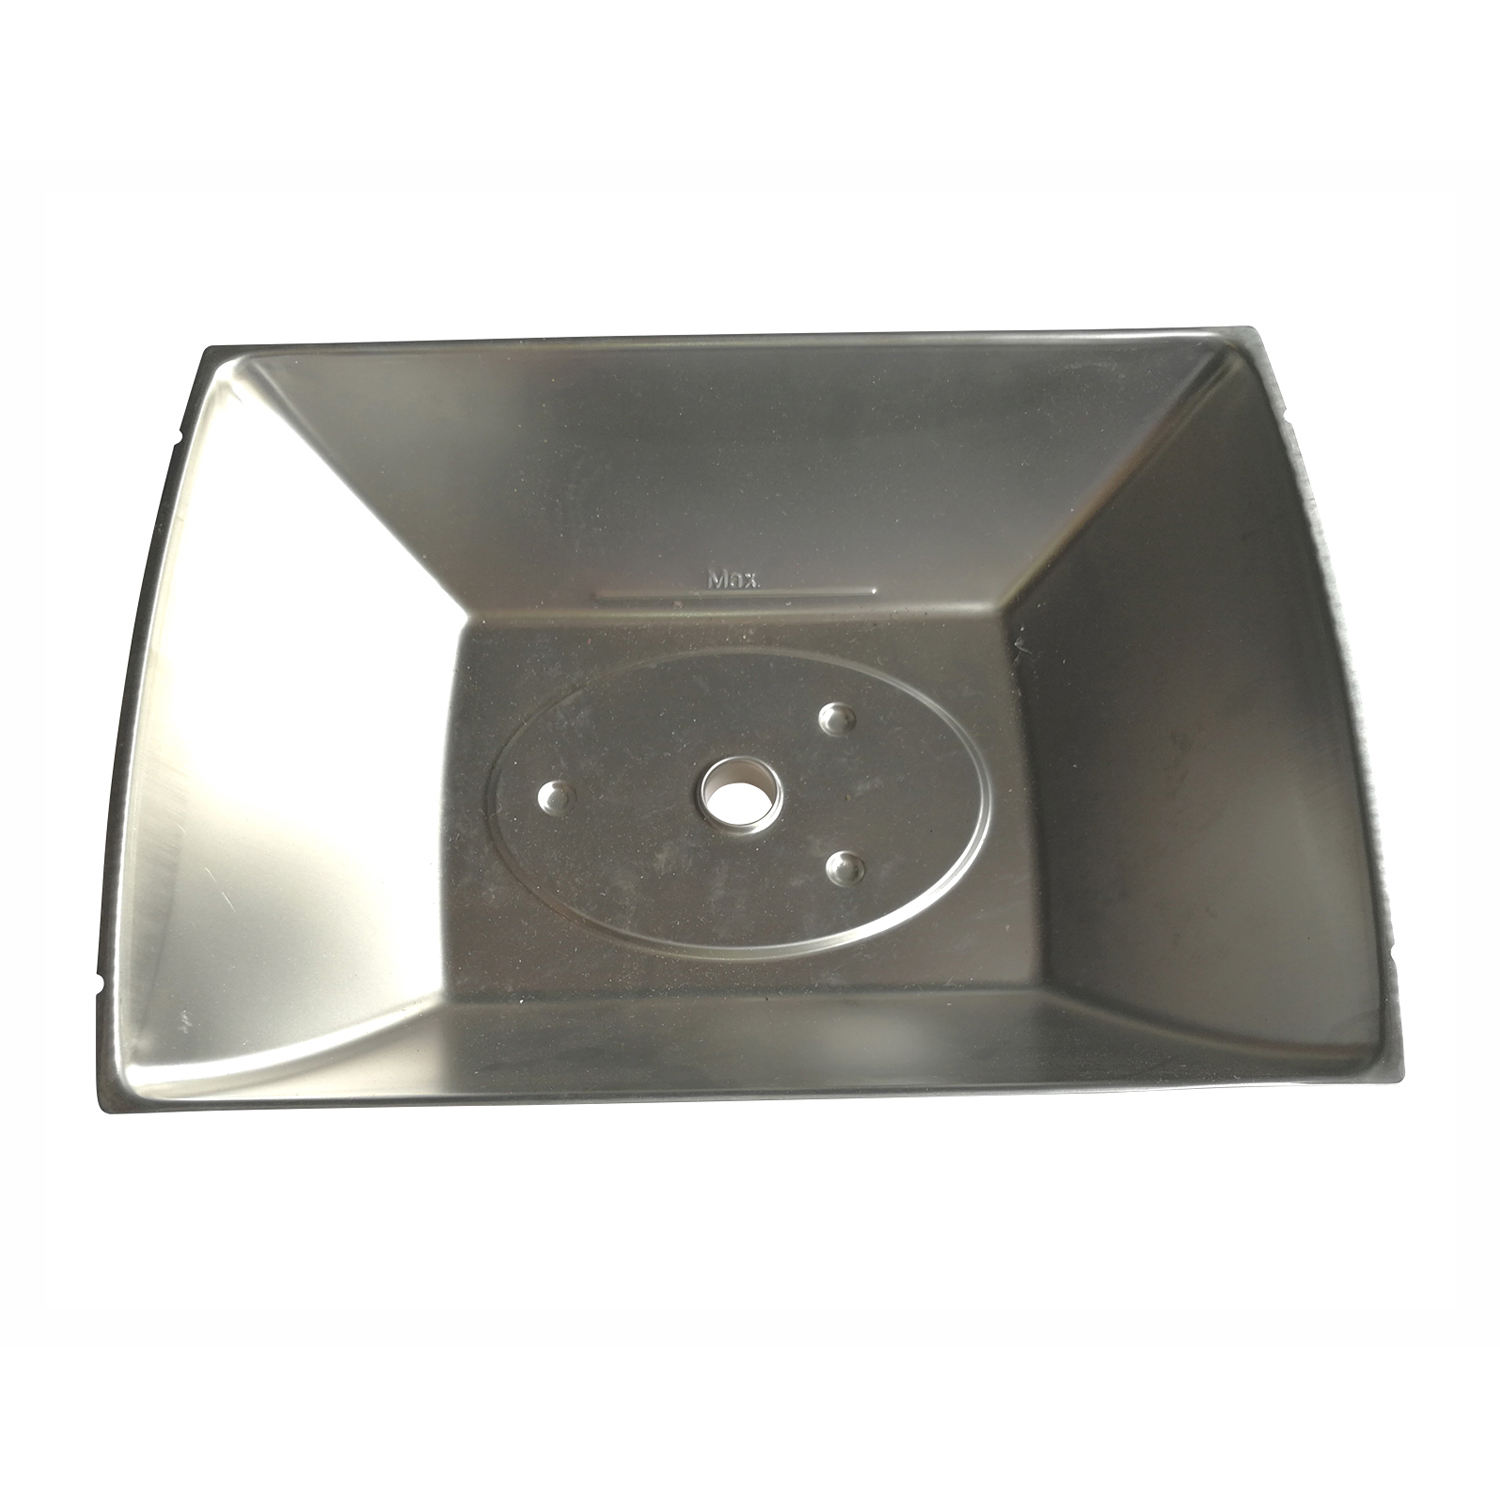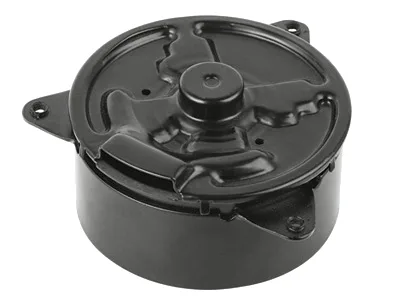
Aunov Tech builds this Warm wind motor enclosure in stainless steel, from coil or bar through to the finished surfaces. In the assembly, the HVAC motor housing carries the blower motor internals and guides the cooling airflow. Die work, machining and CMM inspection are all in-house, and a design change is re-sampled in one place with no third party in the loop.
Product overview
The critical features of this metal enclosure are, the formed envelope, flatness and hole location, audited against the approved sample at each production release.
Tooling and finishing for this metal enclosure run under one roof, which keeps the sample loop inside our own schedule, and the same die can be re-cut from the original data.
From coil to finished part
Every metal enclosure follows the same routed path: The shell starts as coil or blank and is drawn through single and progressive dies; flanges and rims are formed in the same line, then trimmed to length.
Every warm wind motor order keeps its trace back to the approved first article, and a reorder is a repeat rather than a new start. First article, drawing revision and material cert travel with each warm wind motor batch.
Materials and finishing
Everything is drawn from a fixed stock list: carbon steel SPCC / DC01, 304 and 316 stainless, aluminium, brass and copper with this metal enclosure costed in carbon steel or stainless.
Coating and polishing are matched to the end use: plating, anodising, powder coating, electrophoresis and passivation. The agreed finish for this metal enclosure travels with the part number on every reorder.
The warm wind motor tooling and setup record is stored against the part number, so nothing depends on someone remembering. First article, drawing revision and material cert travel with each warm wind motor batch.
Quality control and inspection
An ISO 9001 certified system governs production: incoming material is verified against mill certificates, the first article is CMM-measured against the print, and later batches follow the sampling plan agreed at approval. On the HVAC motor housing itself, shaft-bore runout is measured at first article, and salt-spray testing backs the coating choice for wet locations. If the assembly calls for torque, leak or pressure proof, the test is built into the quality plan, and the batch file carries the results.
Applications
The metal enclosure sits in industrial equipment and general assembly work for customers who own the drawing and the tooling.
The same metal enclosure is used across several platforms, so wall bands and finishes are selected to cover the widest duty, and no re-tooling is needed.
Specifications
| Item | Warm wind motor enclosure |
|---|---|
| Brand | AUNOV |
| Designing | Quotation follows the print, not a catalogue – samples are reverse-measured into a controlled drawing; changes are priced before they are made. |
| Tooling | Dies, fixtures and gauges are made in our own toolroom, so a die can be re-cut against the approved drawing, and maintenance is tracked against the part number. |
| Samples | Samples are issued for approval before the run, and production starts only after written sign-off. |
| Materials | Standard stock: carbon steel (SPCC / DC01), 304 / 316 stainless, aluminium, brass; grade and temper are confirmed in writing before tooling. |
| Surface finish | Natural, plated or coated – the print decides, and the agreed finish is logged; finish thickness and adhesion checked on the first article. |
| Processing | Multi-stage deep drawing with interstage annealing, trimmed and pierced in following dies; in-process checks sit between stages, not only at the end. |
| Equipment | Mechanical presses from 5 to 250 T and hydraulic presses 250-500 T, with in-line annealing furnaces; first articles and batch samples are checked on the CMM. |
| Tolerance | +/-0.05 mm on drawn diameters, tighter bands confirmed against the drawing; critical dimensions carry CMM data with the shipment. |
| Delivery terms | Incoterms FOB as standard with DDP on request; sea and air options priced with the order. |