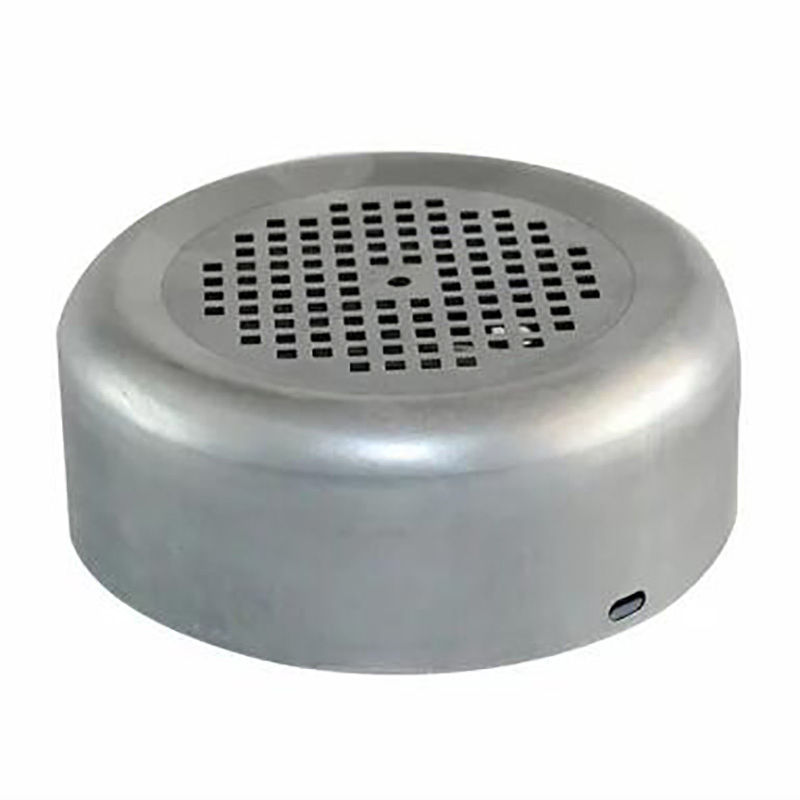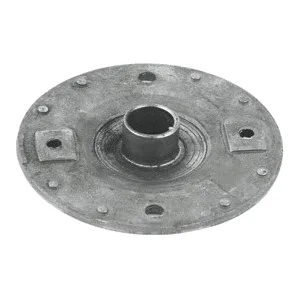
The Stamping DC motor cover is produced by Aunov Tech from stainless steel, formed and finished under one roof. In the assembly, the motor end cover closes the motor stack and carries the bearing seat. Die work, machining and CMM inspection are all in-house, so repeat orders stay aligned with the approved sample without re-quoting the job elsewhere.
Product overview
This metal cover is defined by, wall thickness control, flange geometry and the sealing surface, audited against the approved sample at each production release.
Toolroom, presses and machining centres used on this metal cover operate on the same site, so a drawing change is absorbed in one step, with process data archived for repeat orders.
How the part is produced
The process for this metal cover runs in a fixed sequence: The strip is blanked, formed and pierced in a progressive die; secondary tapping, bending and deburring follow on the same site.
The tooling record is stored against the part number, so a repeat order starts from the same approved data.
Materials and finishing
Our stock list runs to carbon steel SPCC / DC01, 304 and 316 stainless, aluminium, brass and copper and this metal cover runs in carbon steel or stainless.
Coating and polishing are matched to the end use: plating, anodising, powder coating, electrophoresis and passivation. Once approved, the finish for this metal cover is fixed and does not get re-decided.
Route cards follow each stamping dc motor batch through the shop, so the next run starts from the data that already worked. Process settings for the stamping dc motor are archived, so later runs can be compared with the one you approved.
Quality control
The factory operates with ISO 9001 certification: material traceability starts with mill certificates, a full CMM report approves the first article, and routine sampling keeps batches aligned with the first article. On the motor end cover itself, bearing-bore size and spigot runout are measured at first article and gauged on production runs. Where the application asks for it, torque, leak or pressure testing is added to the plan, with certificates included in the shipment file.
Applications
The metal cover is specified into industrial machinery and equipment assemblies in both OEM and aftermarket supply.
One drawing for this metal cover is commonly applied to several programmes, so one tooling set serves every position, and no re-tooling is needed.
Specifications
| Item | Stamping DC motor cover |
|---|---|
| Brand | AUNOV |
| Designing | Send drawings, or send a sample to be measured – samples are reverse-measured into a controlled drawing; the approved drawing is kept as the controlled master. |
| Tooling | Dies, fixtures and gauges are made in our own toolroom, so a die can be re-cut against the approved drawing, and maintenance is tracked against the part number. |
| Samples | First-article samples ship with a dimensional report and material certificate. |
| Materials | Carbon steel (SPCC / DC01), 304 / 316 stainless, aluminium, brass and copper – the grade is matched to the duty of this cover. |
| Surface finish | Surface treatment matched to the duty: plating, coating or polishing; the agreed finish travels with the part number. |
| Processing | Deep drawing from coil or blank, with in-process annealing so walls thin evenly; batch records are filed so a repeat order starts from approved data. |
| Equipment | Mechanical presses from 5 to 250 T and hydraulic presses 250-500 T, with in-line annealing furnaces, backed by CNC turning centres and a climate-controlled inspection room. |
| Tolerance | +/-0.03 mm on turned secondary features, +/-0.1 mm on as-drawn walls; GD&T per drawing, PPAP-style reports on request. |
| Delivery terms | FOB, CIF or DDP per Incoterms 2020, payment by T/T, L/C at sight or D/P; price breaks tie to annual volume. |
Also known as: flanged conical stamped covers — same part, same tooling, only the drawing reference differs.