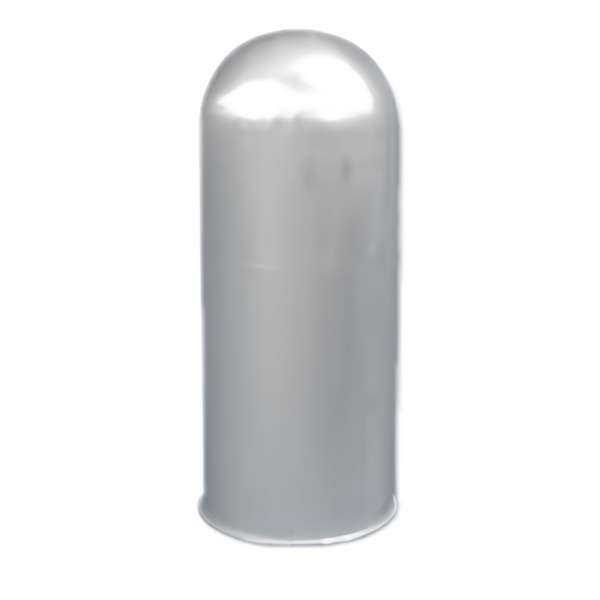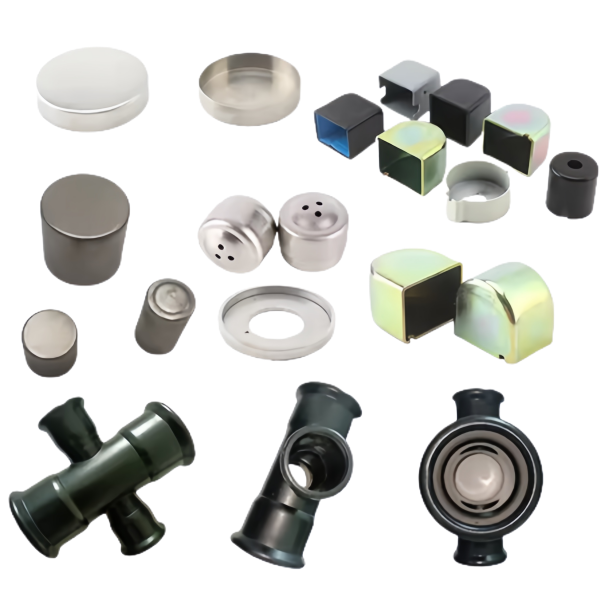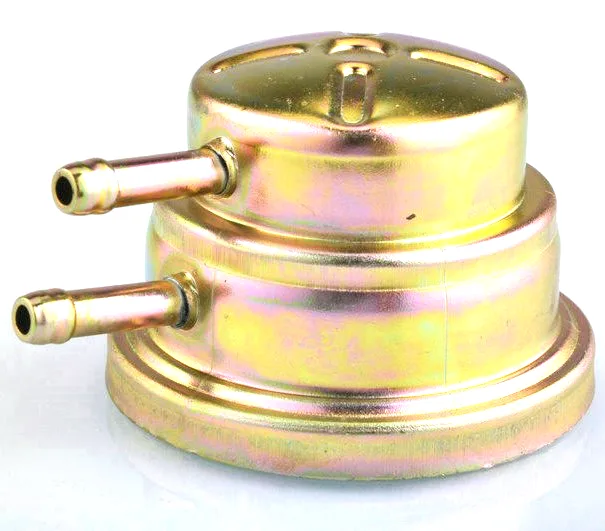
Aunov Tech supplies the Deep Drawn Nickel Fuel Housing as a stainless steel component manufactured entirely in house. In service, the drawn housing encloses the sensitive internals and carries the mounting interface. Forming, machining and inspection share one floor, and a design change is re-sampled in one place without a second supplier involved.
Product overview
For this nickel-plated steel housing, the drawing centres on, wall thinning, concentricity and the finished mating faces, audited against the approved sample at each production release.
The press shop and machine shop that make this nickel-plated steel housing share one floor, which keeps revision loops short and samples fast, and every step is logged against the part number.
How it is manufactured
This is how the nickel-plated steel housing is built: Coil is blanked and drawn through progressive and single-stage dies; after drawing, critical faces are machined and the part is degreased and gauged.
Repeat -plated two-tier housing orders are measured against the approved sample, so neither material nor finish drifts between lots. First article, drawing revision and material cert travel with each -plated two-tier housing batch.
Materials and surface finish
Materials kept on the floor cover carbon steel SPCC / DC01, 304 and 316 stainless, aluminium, brass and copper with this nickel-plated steel housing costed in nickel-plated steel.
The finish is chosen for the environment the part sees: zinc, nickel or chrome plating, anodising, powder coating, electrophoresis and passivation. The finish on this nickel-plated steel housing is locked to the drawing revision, so later orders match.
Repeat -plated two-tier housing orders are measured against the approved sample, so neither material nor finish drifts between lots. First article, drawing revision and material cert travel with each -plated two-tier housing batch.
Quality control and inspection
Production runs under an ISO 9001 certified quality system: mill certificates cover every delivery of stock, first articles are measured on a CMM, and later batches follow the sampling plan agreed at approval. Cavity depth and seal face finish of the -plated two-tier housing are measured at first article. Torque, leak and pressure tests are available where the assembly needs them, and the report is packed with the shipment.
Applications
You will find this nickel-plated steel housing inside automotive assemblies and under-hood equipment in both OEM and aftermarket supply.
The same nickel-plated steel housing is used across several platforms, so the finish is chosen to cover the harshest of them, and the die does not have to change.
Customization and options
Where designs usually differ
Points customers normally tailor on this nickel-plated steel housing: wall thickness bands, flange geometry, thread call-outs and the surface finish, and whether the first order is a prototype, a pilot lot or a production release.
The quotation for this nickel-plated steel housing marks what the existing tooling can do, so there are no surprise tooling charges after approval. The -plated two-tier housing quotation carries a validity period and the price is held to it.
Specifications
| Item | Deep Drawn Nickel Fuel Housing |
|---|---|
| Brand | AUNOV |
| Designing | Made to your 2D/3D drawings (PDF, DWG, STEP, IGS) – DFM notes are returned before any tooling is cut; revisions are re-quoted once rather than silently absorbed. |
| Tooling | Progressive and drawing dies are designed and built in house, so a die can be re-cut against the approved drawing, and maintenance is tracked against the part number. |
| Samples | Samples are issued for approval before the run, so the approved first article becomes the gauge reference, and later batches are gauged back to the signed sample. |
| Materials | Nickel 200 / 201 and nickel-plated steel, 0.8-4.0 mm; selected where conductivity and oxidation resistance both matter. |
| Surface finish | Plating, coating or polishing to suit the drawing; masking and laser marking available where needed. |
| Processing | Deep drawing on maintained presses, blank size and lubrication logged per run; in-process checks sit between stages, not only at the end. |
| Equipment | Press shop running 5-250 T mechanical and 250-500 T hydraulic presses, annealing ovens on site; first articles and batch samples are checked on the CMM. |
| Tolerance | +/-0.05 mm on drawn diameters, tighter bands confirmed against the drawing; dimensional reports accompany the first article. |
| Delivery terms | FOB, CIF or DDP per Incoterms 2020, T/T with deposit and L/C for larger runs; repeat orders reuse the approved first article. |
Packaging and delivery
The packing method protects the surfaces of this nickel-plated steel housing: interleaves, bags or trays are matched to the surface treatment, then sealed cartons are palletised for export, with documents and marks to your instruction.