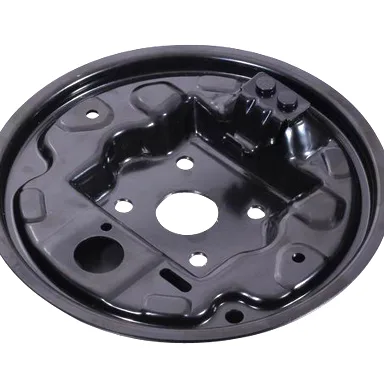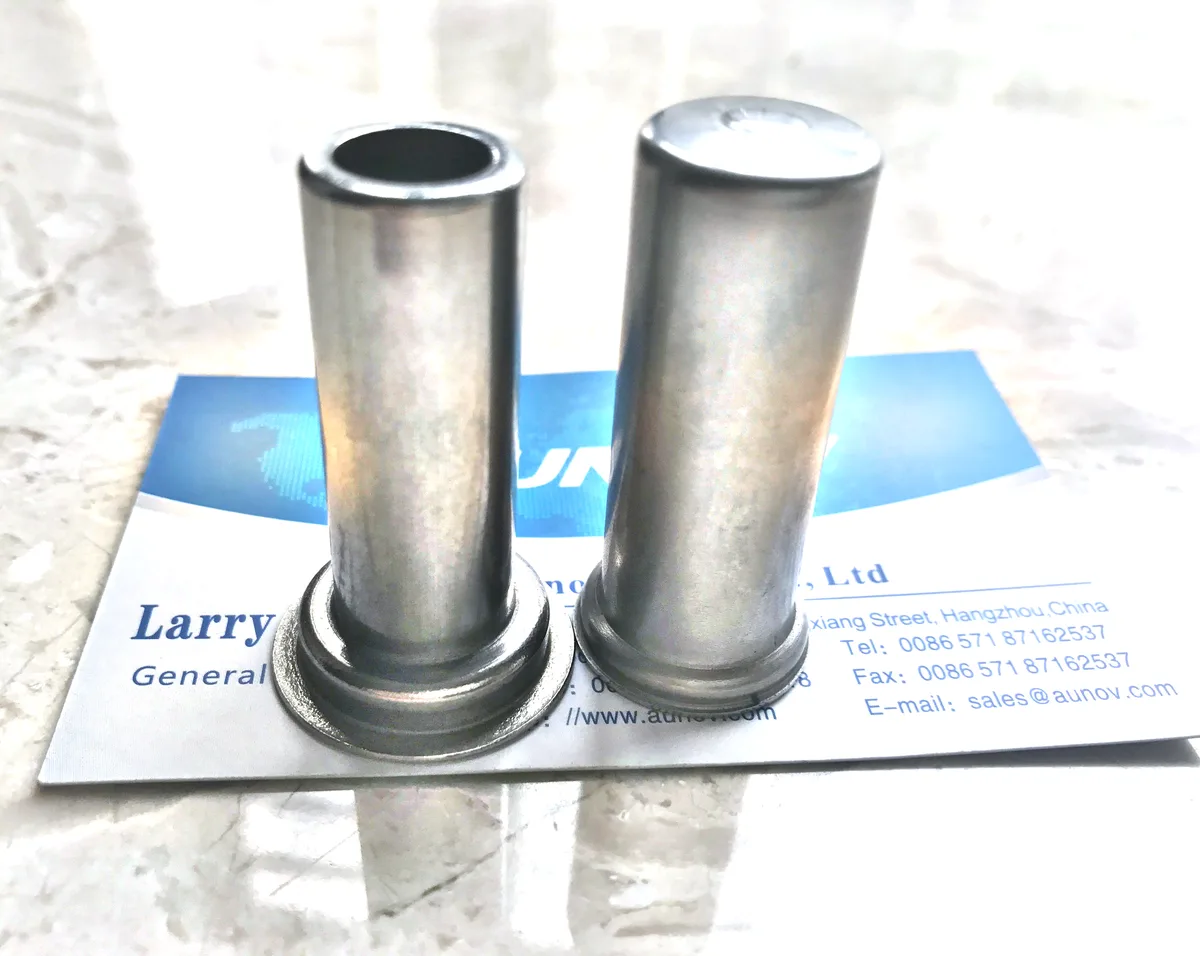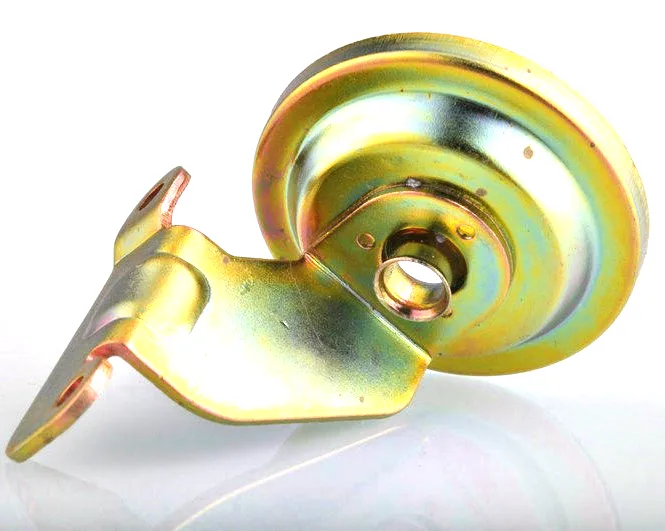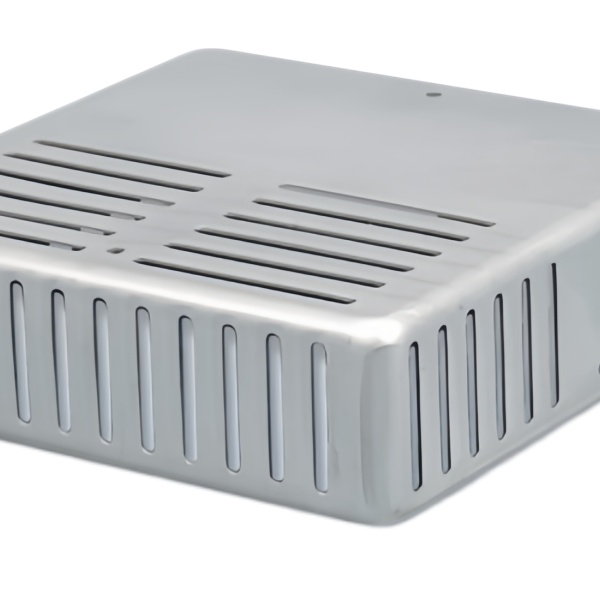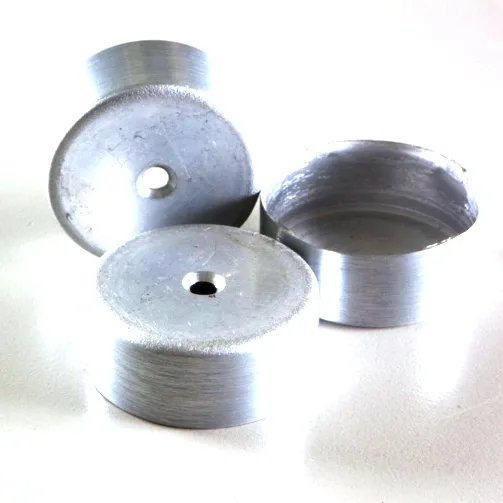
The Deep Drawn Blood Analyzer Liner is produced by Aunov Tech from stainless steel, formed and finished under one roof. On the product, the deep drawn part replaces a machined-from-solid body with a lighter, faster drawn shell. The same floor forms, machines and inspects the part, which keeps tolerances consistent from sample to volume with no third party in the loop.
Product overview
For this metal component, the drawing centres on, the draw ratio, corner radii and the faces that must stay flat, each measured at first article and gauged on production batches.
Die building, pressing and machining for this metal component are all in house, so revisions do not wait on outside suppliers, and the die record stays with your part number.
From coil to finished part
Every metal component follows the same routed path: Blanks are drawn in stages, with interstage annealing where the wall thins; after drawing, critical faces are machined and the part is degreased and gauged.
The analyzer liner cups, is judged by the dimension nobody checks until a failure – fit, seal or concentricity. The analyzer liner cups, is produced to print, with the features that carry function inspected first.
Materials and finishing
Our stock list runs to SPCC / DC01 carbon steel, 304 / 316 stainless, aluminium, brass, copper and bronze and this metal component is costed in carbon steel or stainless.
The surface treatment is picked to match the service conditions: polishing, zinc / nickel / chrome plating, anodising or powder coating. The choice is recorded on the drawing for this metal component, so the decision never has to be made twice.
Every analyzer liner cups, order keeps its trace back to the approved first article, and a reorder is a repeat rather than a new start. Deviations on the analyzer liner cups, are reported before shipment rather than found on your assembly line.
Quality control and inspection
The factory operates with ISO 9001 certification: stock arrivals are checked against mill certificates, first articles are measured on a CMM, and every production run is inspected against the first-article report. The analyzer liner cups, first article is CMM measured – threads gauged to class, diameters on the record. Where the application asks for it, torque, leak or pressure testing is added to the plan, and results travel with the batch paperwork.
Typical applications
The metal component is fitted into industrial equipment and general assembly work across automotive, appliance and industrial programmes.
Drawings for this metal component are adapted across programmes, so the specification is set by the toughest of them, and the same first article applies throughout.
Customization and options
What customers usually vary
Typical decisions customers make on this metal component: coating, wall bands, flange profiles, threads and the degree of closure on the ends, and whether the programme starts as a sample or a full release.
Options for this metal component already covered by the die are shown on the quote, so the boundary between free and chargeable changes is explicit. Price validity for the analyzer liner cups, is stated on the quotation and respected.
Specifications
| Item | Deep Drawn Blood Analyzer Liner |
|---|---|
| Brand | AUNOV |
| Designing | Your drawing sets the part – DFM notes are returned before any tooling is cut; the approved drawing is kept as the controlled master. |
| Tooling | Our toolroom covers die design, wire-cut EDM and maintenance, so tooling lead time stays under our control, and the die remains dedicated to your part. |
| Samples | Samples are produced on the production tooling, so what you approve is what you get. |
| Materials | Stock covers carbon steel (SPCC / DC01), 304 / 316 stainless, aluminium and brass; the final grade is fixed with the drawing review. |
| Surface finish | Zinc, nickel or chrome plating, anodising, passivation or e-coat; alternatives quoted with the quotation, samples approved in writing. |
| Processing | Coil blanking and progressive drawing, coining on the final station where the print calls for it; every stage is logged against your part number. |
| Equipment | 5-250 T mechanical presses, 250-500 T hydraulic presses and annealing furnaces in line, with in-house toolmaking to keep dies and fixtures maintained. |
| Tolerance | +/-0.05 mm to +/-0.1 mm across the part, wall thickness held to print; capability is checked on the first article before the run continues. |
| Delivery terms | Terms are FOB by default, with CIF and DDP quoted on request and freight priced to your door. |
Packaging and delivery
The finish on this metal component dictates how it is packed: interleaves, polybags or formed trays are selected according to the coating, in sealed cartons on export pallets, with documents issued to your instructions.