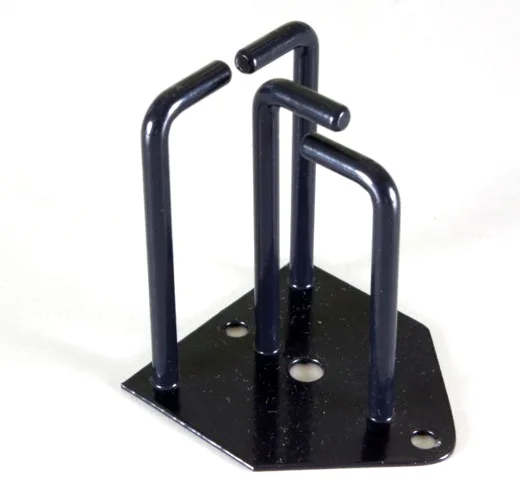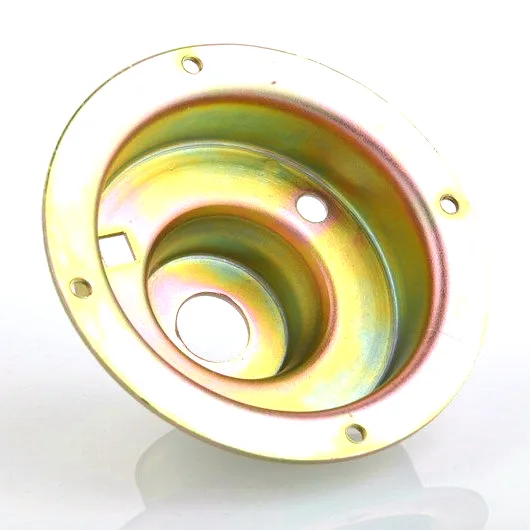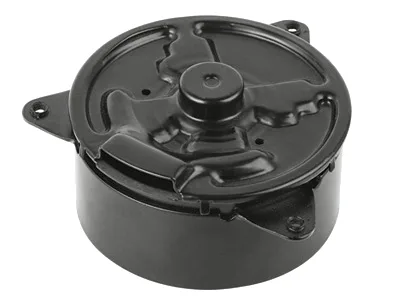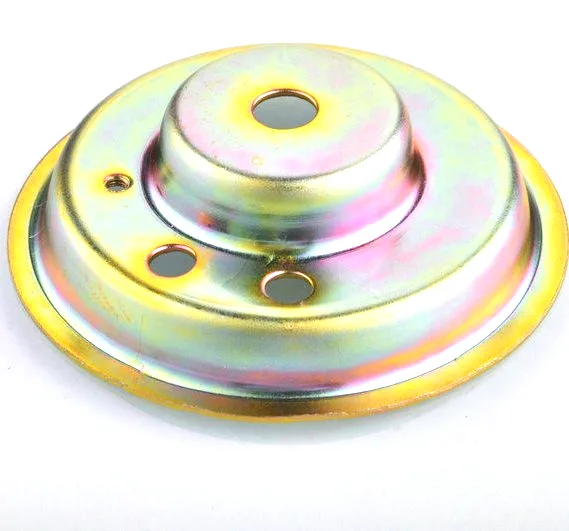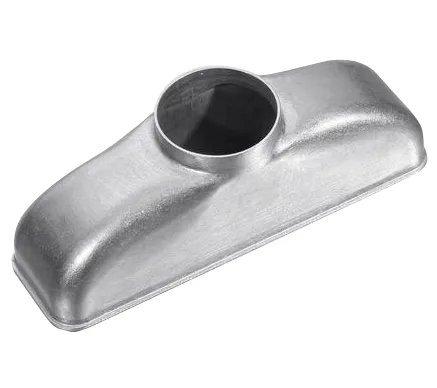
Aunov Tech builds this Stainless Steel Deep Drawn Parts Metal Deep Drawing Forming Cups Sheet in stainless steel, from coil or bar through to the finished surfaces. In service, the drawn housing encloses the sensitive internals and carries the mounting interface. One production floor covers forming, finishing and inspection, so first-article dimensions hold through volume batches without handing the part to another vendor.
Product overview
The drawing for this stainless steel component fixes, draw depth, wall band and the surfaces that forming cannot hold, re-checked whenever the drawing is revised.
Die building, pressing and machining for this stainless steel component are all in house, so the route from print to sample stays short, and the die record stays with your part number.
From coil to finished part
Every stainless steel component follows the same routed path: Drawing runs from flat blank to finished envelope in one controlled sequence; threads are single-pointed or rolled and seats bored in one setup where possible.
Every housing cover order keeps its trace back to the approved first article, and a reorder is a repeat rather than a new start. The signed housing cover sample remains the reference and is kept with the job file.
Materials and finishing
Everything is drawn from a fixed stock list: cold-rolled steel (SPCC / DC01), 304 / 316 stainless, aluminium, brass, copper and bronze and the grade agreed for this stainless steel component is 304 / 316 stainless steel.
The surface treatment is picked to match the service conditions: zinc and nickel plating, chrome, anodising, powder coating and passivation. It is fixed on the drawing for this stainless steel component, so repeat orders never reopen the question.
Each housing cover shipment is verified against the master sample before it leaves the shop. Any change to the housing cover drawing is re-approved and re-verified before production continues.
Quality control and inspection
The plant is ISO 9001 certified: material traceability starts with mill certificates, the first article is CMM-measured against the print, and routine sampling keeps batches aligned with the first article. Seal face finish and cavity depth are measured on the housing cover first article. Torque, leak and pressure tests are available where the assembly needs them, and results travel with the batch paperwork.
Applications
You will find this stainless steel component inside industrial and appliance assemblies in volume programmes as well as aftermarket supply.
The same stainless steel component is used across several platforms, so the tightest tolerance in the family sets the spec, and no re-tooling is needed.
Customization and options
Options changed most often
The parts of the print for this stainless steel component that get adjusted: wall thickness bands, flange geometry, thread call-outs and the surface finish, with orders run as prototypes, pilot lots or scheduled call-offs.
Tooled and untooled options for this stainless steel component are listed separately, so you are not charged twice for a feature the die already makes. No change is made to the housing cover without a written revision.
Specifications
| Item | Stainless Steel Deep Drawn Parts Metal Deep Drawing Forming Cups Sheet |
|---|---|
| Brand | AUNOV |
| Designing | Made to your 2D/3D drawings (PDF, DWG, STEP, IGS) – DFM notes are returned before any tooling is cut; the same drawing is used for every repeat order. |
| Tooling | Tooling is built and held under your part number, so a die can be re-cut against the approved drawing, and ownership is confirmed on the quotation. |
| Samples | Prototype and pre-production samples are provided against the drawing, so the sample is retained as the master, and mass production is gated on that approval. |
| Materials | Stock covers carbon steel (SPCC / DC01), 304 / 316 stainless, aluminium and brass; the final grade is fixed with the drawing review. |
| Surface finish | Zinc, nickel or chrome plating, anodising, passivation or e-coat; alternatives quoted with the quotation, samples approved in writing. |
| Processing | Multi-stage deep drawing with interstage annealing, trimmed and pierced in following dies; first articles verify the whole flow before the run is released. |
| Equipment | Mechanical presses from 5 to 250 T and hydraulic presses 250-500 T, with in-line annealing furnaces, backed by CNC turning centres and a climate-controlled inspection room. |
| Tolerance | +/-0.05 mm on formed features, with capability data on critical dimensions; GD&T per drawing, PPAP-style reports on request. |
| Delivery terms | FOB with DDP offered for EU and US addresses; payment T/T or L/C, freight quoted to destination. |
Packing and shipment
For this stainless steel component, protection starts at the surface: the coating decides whether parts are interleaved, bagged or tray-packed, in sealed export cartons, palletised and marked as you direct.