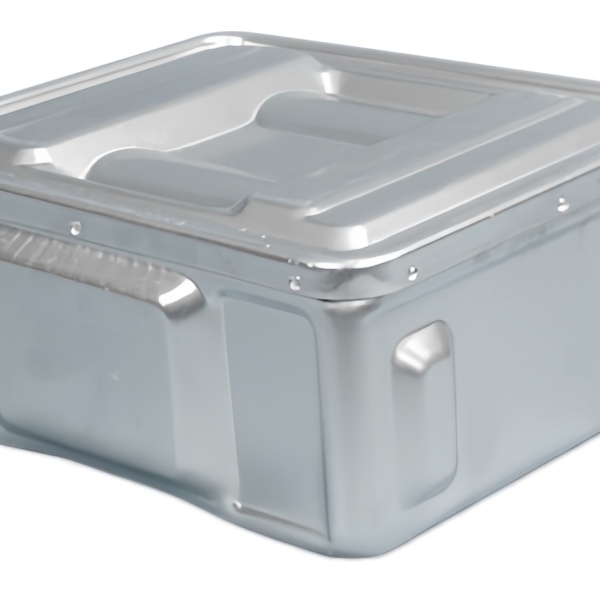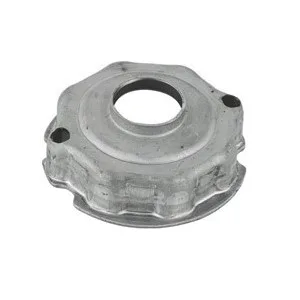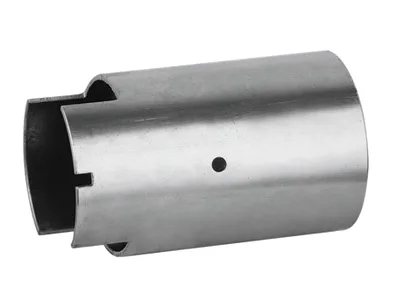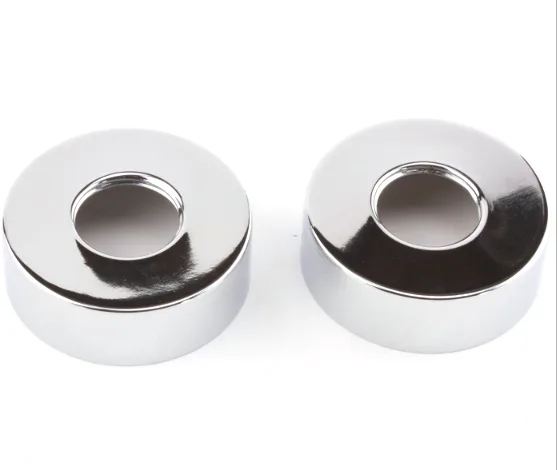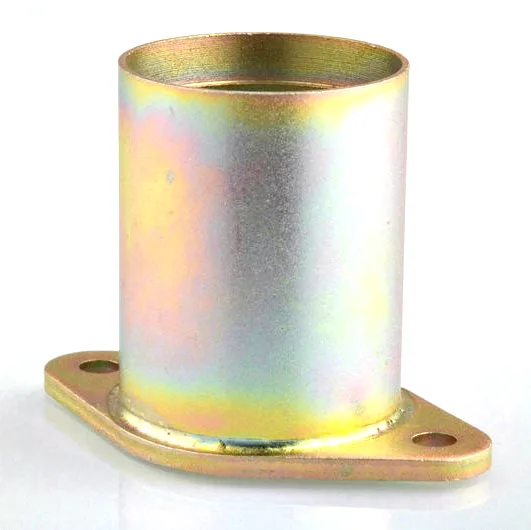
Produced in stainless steel by Aunov Tech, the Deep drawn housing is formed and machined on the same floor. In operation, the drawn housing shields the assembly from dust, moisture and handling while locating it in place. Die work, machining and CMM inspection are all in-house, which keeps tolerances consistent from sample to volume without re-quoting the job elsewhere.
Product overview
What matters most on this metal housing is, the forming route, the tolerance band and the sealing faces, recorded on the inspection report for every batch.
The press shop and machine shop that make this metal housing share one floor, so a drawing change is absorbed in one step, and nothing about the route depends on a third party.
How the part is produced
The route for this metal housing is fixed and repeatable: Coil is blanked and then drawn down in successive stages; after drawing, critical faces are machined and the part is degreased and gauged.
Production batches of the housing are gauged back to the signed first article, not to a memory of it. Process settings for the housing are archived, so later runs can be compared with the one you approved.
Materials and finishing
Everything is drawn from a fixed stock list: carbon steel SPCC / DC01, 304 and 316 stainless, aluminium, brass and copper and this metal housing runs in carbon steel or stainless.
Finish selection follows the working environment: polishing, plating in zinc, nickel or chrome, anodising, powder coating, electrophoresis and passivation. It is written into the drawing for this metal housing, so it cannot drift between batches.
Batch records for the housing are filed against the part number, so process settings are reused instead of re-invented. Any change to the housing drawing is re-approved and re-verified before production continues.
Quality control and inspection
Quality management is certified to ISO 9001: incoming material is verified against mill certificates, the CMM measures the first article dimension by dimension, and run inspections follow an agreed sampling plan. Cavity depth and seal face finish on the housing are verified at first article. If the assembly calls for torque, leak or pressure proof, the test is built into the quality plan, and the inspection report ships with each batch.
Applications
Typical installation of the metal housing is in industrial and appliance assemblies for customers who buy to drawing.
A single design of this metal housing is often reused across a product family, so one tooling set serves every position, and the same first article applies throughout.
Specifications
| Item | Deep drawn housing |
|---|---|
| Brand | AUNOV |
| Designing | Your drawing sets the part – a manufacturability review comes back with the quotation; the same drawing is used for every repeat order. |
| Tooling | Tooling is built and held under your part number, so the die charge appears as its own quotation line, and the die remains dedicated to your part. |
| Samples | Samples are issued for approval before the run, and production starts only after written sign-off. |
| Materials | Standard stock: carbon steel (SPCC / DC01), 304 / 316 stainless, aluminium, brass; special grades are sourced to the drawing when volumes justify. |
| Surface finish | Plating, powder coating, anodising or polishing, per the print; the agreed finish travels with the part number. |
| Processing | Deep drawing from coil or blank, with in-process annealing so walls thin evenly; every stage is logged against your part number. |
| Equipment | Mechanical presses 5-250 T plus 250-500 T hydraulics, with in-line annealing, backed by CNC turning centres and a climate-controlled inspection room. |
| Tolerance | +/-0.05 mm on flange and rim dimensions, wall controlled by the draw; dimensional reports accompany the first article. |
| Delivery terms | CIF or DDP, with FOB available, T/T with deposit and L/C for larger runs; call-off schedules are supported. |
Also known as: deep drawn parts — same part, same tooling, only the drawing reference differs.