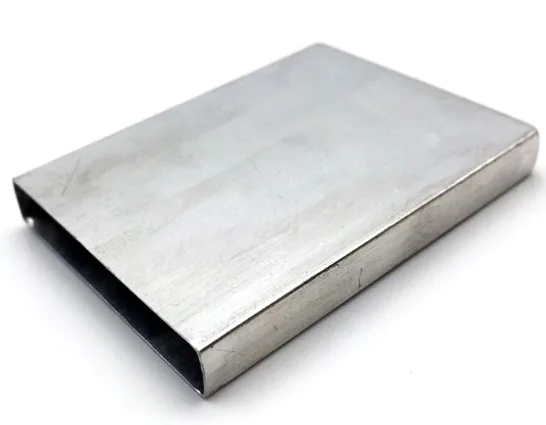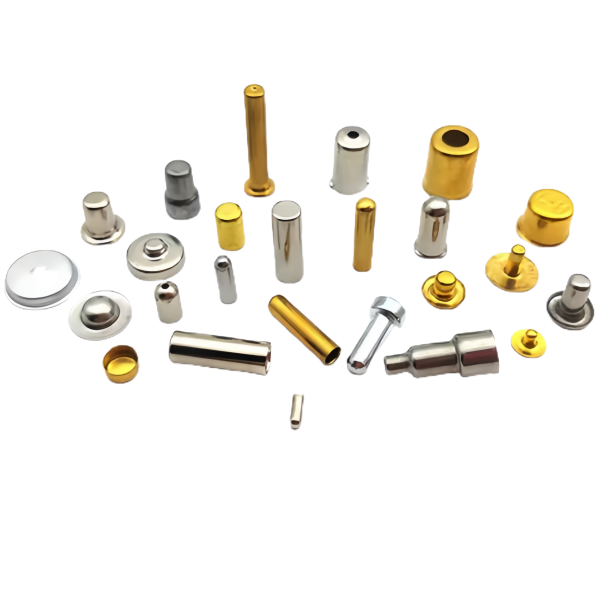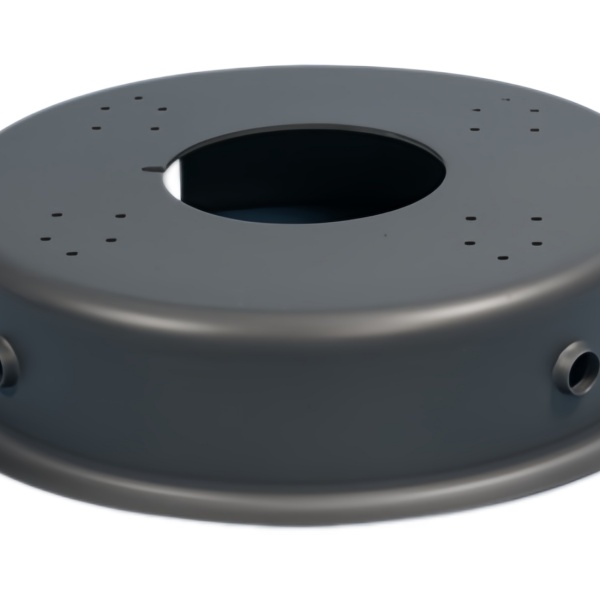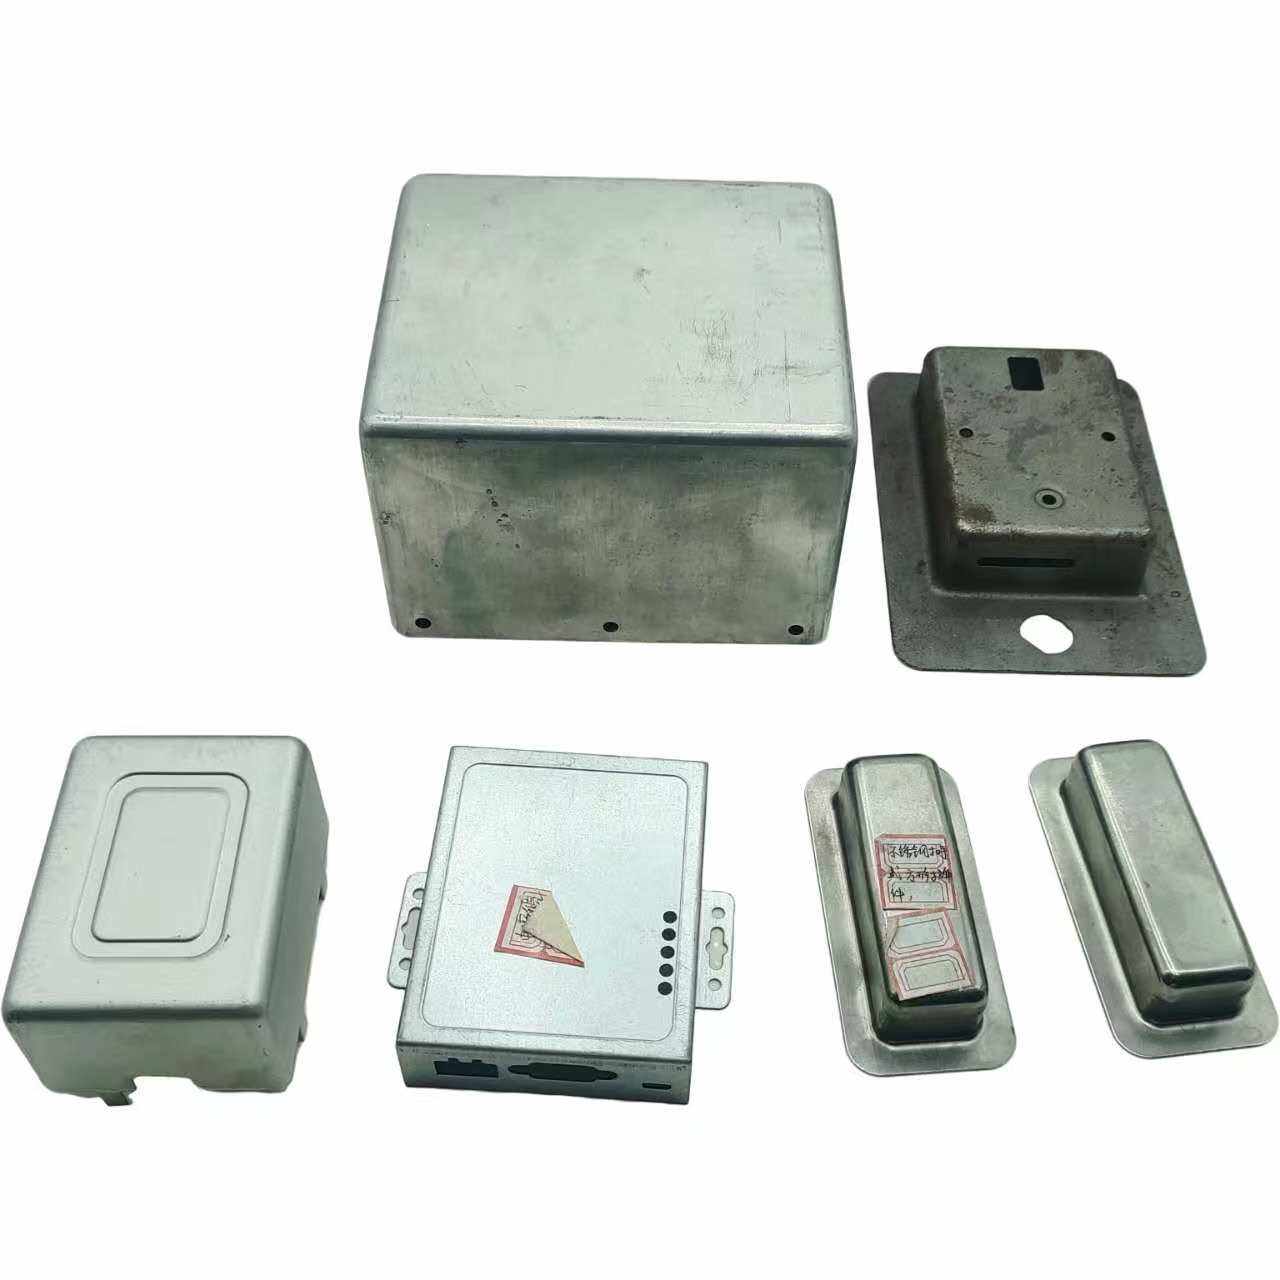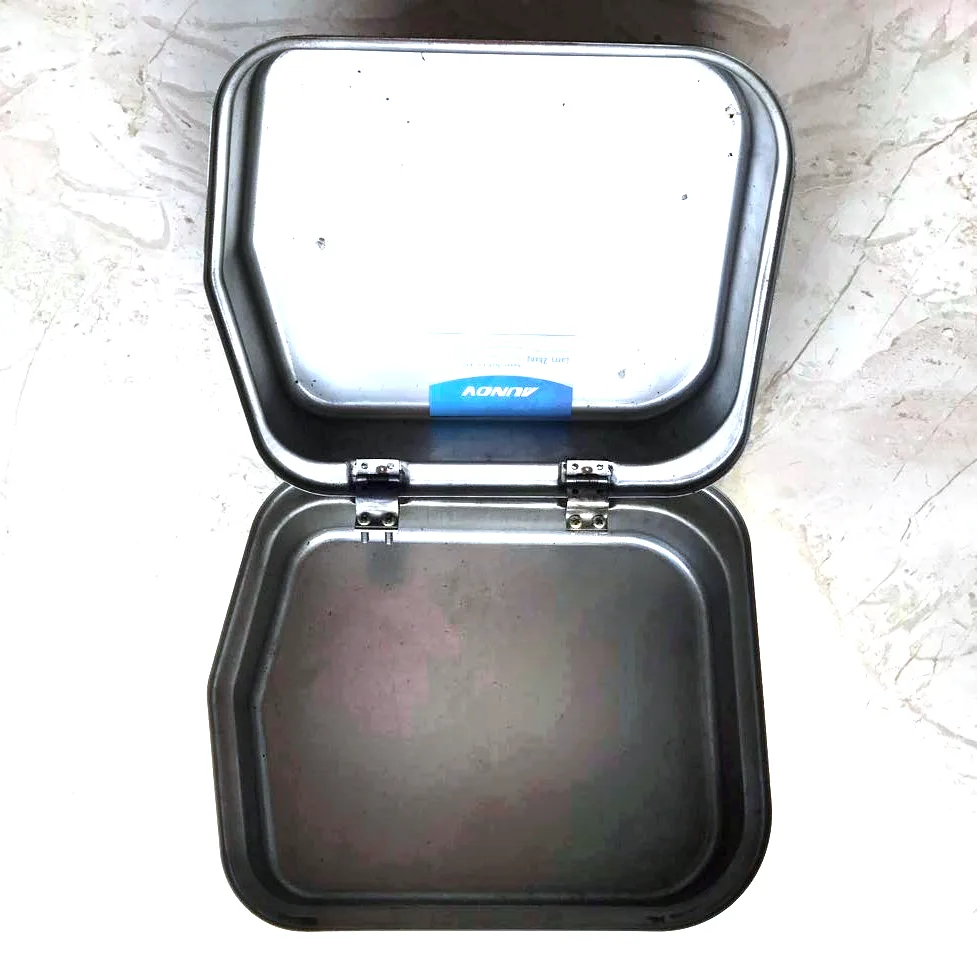
The Deep Drawn Sheet Metal Electronic Enclosure Box Stamping Drawing Parts is produced by Aunov Tech from stainless steel, formed and finished under one roof. On the product, the drawn housing shields the assembly from dust, moisture and handling while locating it in place. Die work, machining and CMM inspection are all in-house, which keeps tolerances consistent from sample to volume with no third party in the loop.
Product overview
For this metal enclosure, the drawing centres on, draw depth, wall band and the surfaces that forming cannot hold, checked by CMM at first article and by gauge in production.
Die work and machining for this metal enclosure sit on the same floor, so the route from print to sample stays short, and nothing about the route depends on a third party.
How it is manufactured
This is how the metal enclosure is built: Blanks are drawn in stages, with interstage annealing where the wall thins; after drawing, critical faces are machined and the part is degreased and gauged.
The enclosure box tooling and setup record is stored against the part number, so nothing depends on someone remembering. Mill certificates are filed per heat, so enclosure box traceability survives a change of material batch.
Materials and finishing
Everything is drawn from a fixed stock list: SPCC / DC01 carbon steel, 304 / 316 stainless, aluminium, brass, copper and bronze and this metal enclosure is costed in carbon steel or stainless.
Cleanliness drives the finish here: polishing, zinc / nickel / chrome plating, anodising or powder coating. It is written into the drawing for this metal enclosure, so it cannot drift between batches.
Batch records for the enclosure box are filed against the part number, so process settings are reused instead of re-invented. Process settings for the enclosure box are archived, so later runs can be compared with the one you approved.
Quality control
The factory operates with ISO 9001 certification: incoming material is verified against mill certificates, first articles are measured on a CMM, and production batches are inspected on a sampling plan. First-article measurement of the enclosure box covers cavity depth and seal face finish. Functional testing – torque, leak or pressure – can be written into the plan, and the report is packed with the shipment.
Where the part is used
The metal enclosure is specified into power supplies, antennas and electronic housings for customers who buy to drawing.
Drawings for this metal enclosure are adapted across programmes, so one approved version covers the whole range, and no re-tooling is needed.
Customization and options
Common variation points across this enclosure box family
Points customers normally tailor on this metal enclosure: material and coating for the duty, wall bands, flange forms, threads and bosses, closed ends and finishes matched to the working environment, and whether the first order is a prototype, a pilot lot or a production release.
The quotation for this metal enclosure is explicit about what the die already covers, so the boundary between free and chargeable changes is explicit. Price breaks for the enclosure box are shown against quantities on the quote.
Specifications
| Item | Deep Drawn Sheet Metal Electronic Enclosure Box Stamping Drawing Parts |
|---|---|
| Brand | AUNOV |
| Designing | Send drawings, or send a sample to be measured – samples are reverse-measured into a controlled drawing; revisions are re-quoted once rather than silently absorbed. |
| Tooling | Tooling is quoted once and held – reorders are priced on the part, not on the die. |
| Samples | Pre-production samples come with a full inspection report, so the sample is retained as the master, and later batches are gauged back to the signed sample. |
| Materials | Carbon steel (SPCC / DC01), 304 / 316 stainless, aluminium, brass and copper – the grade is matched to the duty of this enclosure. |
| Surface finish | Natural, plated or coated – the print decides, and the agreed finish is logged; finish thickness and adhesion checked on the first article. |
| Processing | Deep drawing on maintained presses, blank size and lubrication logged per run; every stage is logged against your part number. |
| Equipment | 5-250 T mechanical presses, 250-500 T hydraulic presses and annealing furnaces in line; first articles and batch samples are checked on the CMM. |
| Tolerance | +/-0.1 mm general on drawn sections, +/-0.03 mm on machined seats; GD&T per drawing, PPAP-style reports on request. |
| Delivery terms | Incoterms FOB as standard with DDP on request; sea and air options priced with the order. |
Packing and shipment
Packaging protects the finished surfaces of this metal enclosure: interleaves, polybags or formed trays are selected according to the coating, in sealed cartons on export pallets, documented and marked to your instruction.