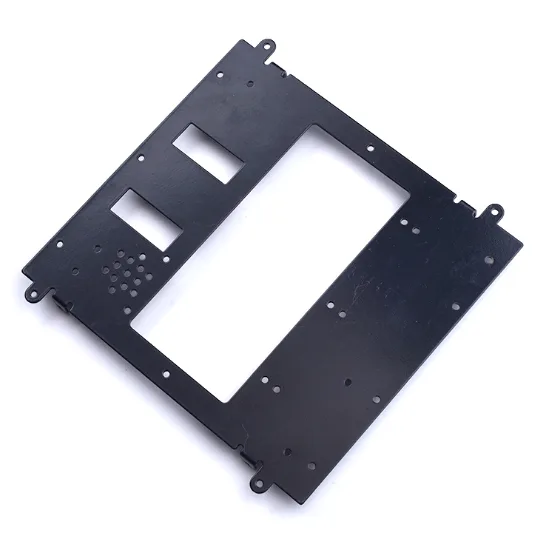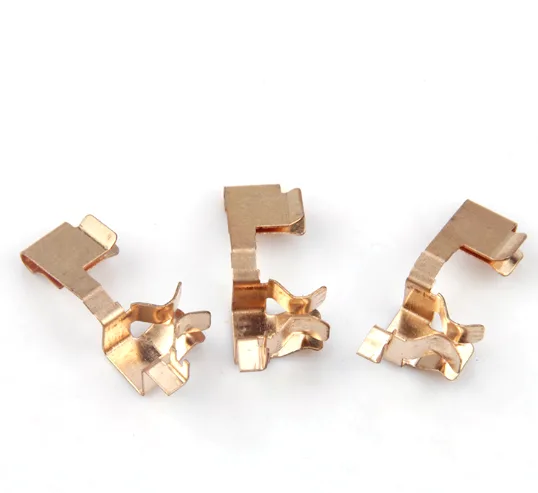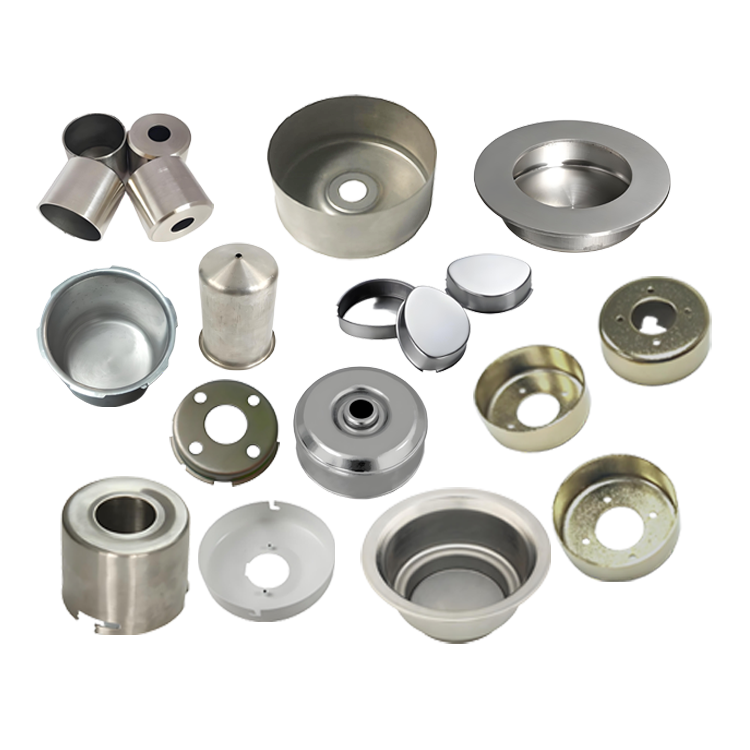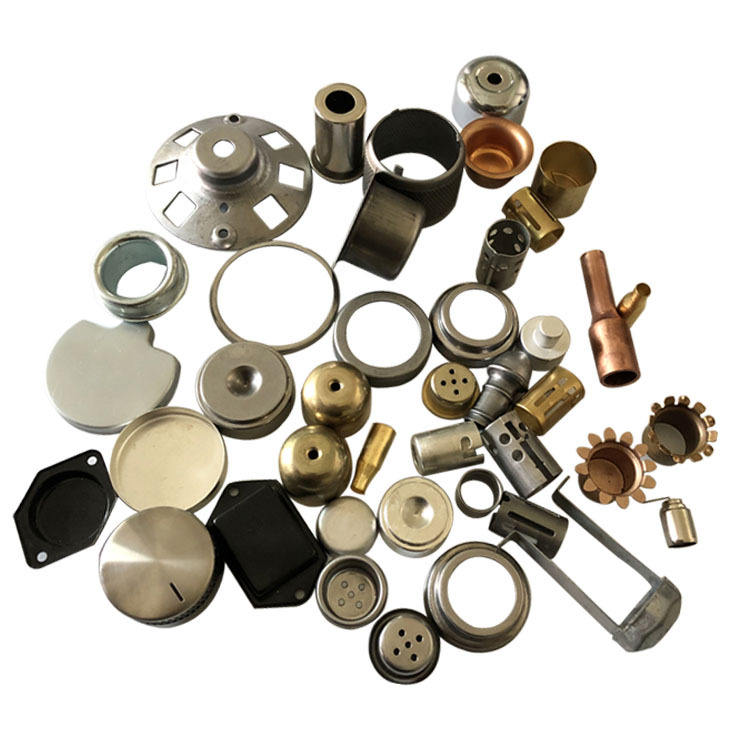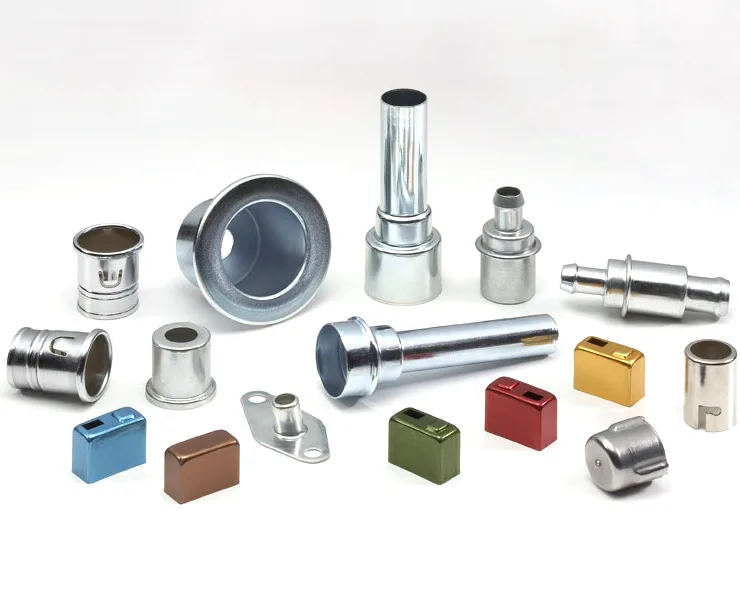
Aunov Tech builds this Sheet Metal Progressive Deep Drawn Stamped Parts Aluminum Brass Deep in brass or aluminum, from coil or bar through to the finished surfaces. In operation, the deep drawn part carries the formed geometry the assembly needs at volume. One production floor covers forming, finishing and inspection, which keeps tolerances consistent from sample to volume with no third party in the loop.
Product overview
The specification of this aluminium component turns on, the forming route, the tolerance band and the sealing faces, controlled from the approved first article onward.
Forming, machining and finishing for this aluminium component happen on one site, which keeps the sample loop inside our own schedule, and the approved sample is kept as the master.
How it is manufactured
Production follows a defined route: Coil is blanked and then drawn down in successive stages; the part is annealed between stages so the wall thins evenly.
Each shipment is traceable to the signed first article, and that record is what every reorder is built from.
Materials and surface finish
Everything is drawn from a fixed stock list: SPCC / DC01 carbon steel, 304 / 316 stainless, aluminium, brass, copper and bronze with aluminium specified on the drawing for this aluminium component.
Coating and polishing are matched to the end use: zinc and nickel plating, chrome, anodising, powder coating and passivation. The finish on this aluminium component is locked to the drawing revision, so later orders match.
Production batches of the connector sleeve are gauged back to the signed first article, not to a memory of it. First article, drawing revision and material cert travel with each connector sleeve batch.
Quality control
An ISO 9001 certified system governs production: stock arrivals are checked against mill certificates, first-article geometry is confirmed on the CMM, and run inspections follow an agreed sampling plan. For the connector sleeve, first articles are CMM measured and threads are gauged to class. If the assembly calls for torque, leak or pressure proof, the test is built into the quality plan, with certificates included in the shipment file.
Typical applications
You will find this aluminium component inside industrial machinery and equipment assemblies across automotive, appliance and industrial programmes.
One part number for this aluminium component frequently serves several assemblies, so wall bands and finishes are selected to cover the widest duty, without a second tooling round.
Options and variations
Frequently varied options
Typical customer decisions: material and coating for the duty, wall bands, flange forms, threads and bosses, closed ends and finishes matched to the working environment, and whether orders run as prototypes, pilot lots or scheduled batches.
Changes are quoted with their tooling impact stated explicitly, making the cost of each choice clear before you commit.
Specifications
| Item | Sheet Metal Progressive Deep Drawn Stamped Parts Aluminum Brass Deep |
|---|---|
| Brand | AUNOV |
| Designing | Driven by your drawing or a physical sample – DFM notes are returned before any tooling is cut; revisions are re-quoted once rather than silently absorbed. |
| Tooling | Progressive and drawing dies are designed and built in house, so the die charge appears as its own quotation line, and first-article timing is measured from the tooling start date. |
| Samples | Sample parts are measured and reported before submission, so the part is proven before it is made in volume, and later batches are gauged back to the signed sample. |
| Materials | Stock runs to carbon steel, 304 / 316 stainless, aluminium and brass; the final grade is fixed with the drawing review. |
| Surface finish | Plating, powder coating, anodising or polishing, per the print; finish thickness and adhesion checked on the first article. |
| Processing | Deep drawing on maintained presses, blank size and lubrication logged per run; batch records are filed so a repeat order starts from approved data. |
| Equipment | Press shop running 5-250 T mechanical and 250-500 T hydraulic presses, annealing ovens on site, with CNC turning centres for secondary operations and CMM inspection. |
| Tolerance | +/-0.03 mm on turned secondary features, +/-0.1 mm on as-drawn walls; critical dimensions carry CMM data with the shipment. |
| Delivery terms | FOB Ningbo or Shanghai, T/T or L/C, with D/P accepted on repeat business; repeat orders reuse the approved first article. |
Packaging and delivery
Packaging protects the finished surfaces of this aluminium component: interleaves, bags or trays are matched to the surface treatment, in sealed cartons on export pallets, with documents issued to your instructions.