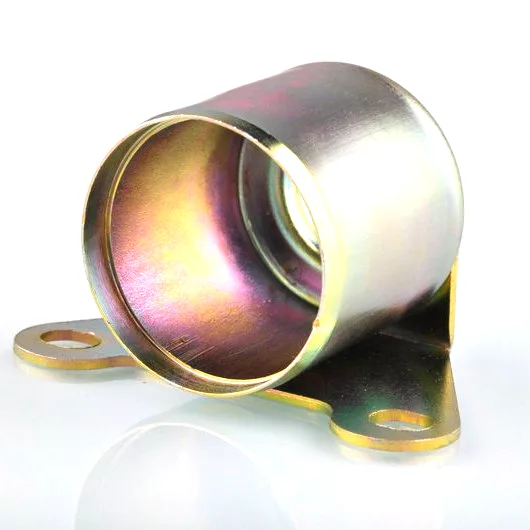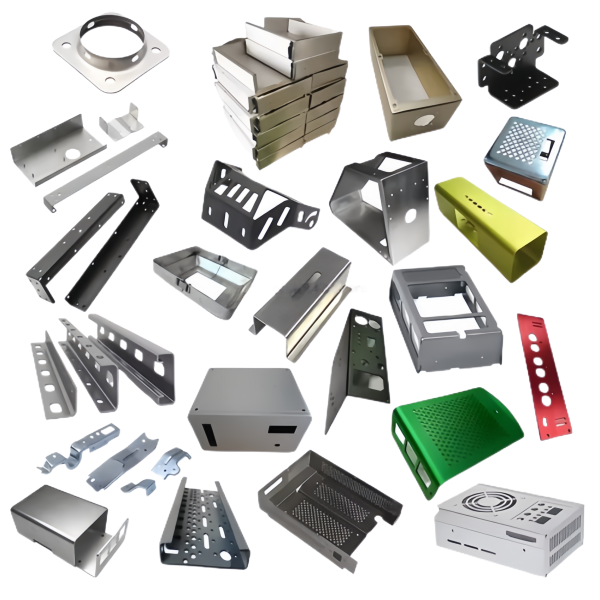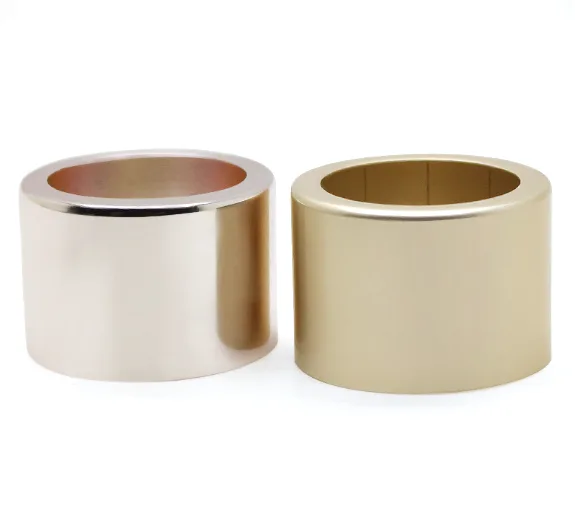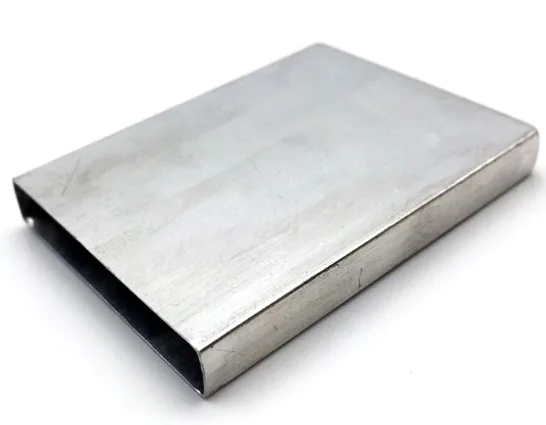
Produced in stainless steel by Aunov Tech, the Custom Stainless Steel Sheet Metal Deep Drawn Metal Stamping Spinning is formed and machined on the same floor. In duty, the CNC machined part provides the finished surfaces, threads and seats the mating parts locate on. The same floor forms, machines and inspects the part, so repeat orders stay aligned with the approved sample without a second supplier involved.
Product overview
The specification of this stainless steel component turns on, wall thinning, concentricity and the finished mating faces, all held to the drawing and verified at first article.
Die building, pressing and machining for this stainless steel component are all in house, which keeps the sample loop inside our own schedule, and every step is logged against the part number.
How the part is produced
Manufacturing runs on a controlled process path: The shell starts as coil or blank and is drawn through single and progressive dies; the finishing operations hold the concentricity the drawing calls for.
Every rectangular tray lid order keeps its trace back to the approved first article, and a reorder is a repeat rather than a new start. That record is what every rectangular tray lid reorder is built on, so nothing changes silently between shipments.
Materials and surface finish
The standard stock list carries carbon steel SPCC / DC01, 304 and 316 stainless, aluminium, brass and copper with this stainless steel component costed in 304 / 316 stainless steel.
The surface treatment is picked to match the service conditions: polishing, plating in zinc, nickel or chrome, anodising, powder coating, electrophoresis and passivation. Once approved, the finish for this stainless steel component is fixed and does not get re-decided.
Each rectangular tray lid shipment is verified against the master sample before it leaves the shop. First article, drawing revision and material cert travel with each rectangular tray lid batch.
Quality control and inspection
The factory operates with ISO 9001 certification: incoming material is verified against mill certificates, first articles are measured on a CMM, and run inspections follow an agreed sampling plan. The rectangular tray lid first article goes on the CMM, with threads gauged to class. If the assembly calls for torque, leak or pressure proof, the test is built into the quality plan, and the report is packed with the shipment.
Where the part is used
Typical installation of the stainless steel component is in industrial and appliance assemblies for customers who buy to drawing.
The same stainless steel component is often run in more than one assembly, so the finish is chosen to cover the harshest of them, and no re-tooling is needed.
Customization and options
Where designs usually differ
The parts of the print for this stainless steel component that get adjusted: coating, wall bands, flange profiles, threads and the degree of closure on the ends, with orders run as prototypes, pilot lots or scheduled call-offs.
Options for this stainless steel component already covered by the die are shown on the quote, so the effect of a revision on price is clear up front. After approval the new rectangular tray lid drawing revision is the controlling document.
Specifications
| Item | Custom Stainless Steel Sheet Metal Deep Drawn Metal Stamping Spinning |
|---|---|
| Brand | AUNOV |
| Designing | The drawing is reviewed first; the agreed version then governs every batch. |
| Tooling | Die design and toolmaking stay in house, so a die can be re-cut against the approved drawing, and the charge is refundable against agreed volumes. |
| Samples | Approval is in writing, and the signed sample is kept as the reference for repeats. |
| Materials | Materials held include carbon steel, 304 / 316 stainless, aluminium and brass; special grades are sourced to the drawing when volumes justify. |
| Surface finish | Finish selected from the drawing: plating, coating, anodising or passivation; the finish is inspected with the dimensional report on the first article. |
| Processing | Deep drawing on maintained presses, blank size and lubrication logged per run; every stage is logged against your part number. |
| Equipment | Press shop running 5-250 T mechanical and 250-500 T hydraulic presses, annealing ovens on site, with CNC turning centres for secondary operations and CMM inspection. |
| Tolerance | +/-0.05 mm on drawn diameters, tighter bands confirmed against the drawing; critical dimensions carry CMM data with the shipment. |
| Delivery terms | FOB Ningbo or Shanghai, T/T with deposit and L/C for larger runs; repeat orders reuse the approved first article. |
Packaging and delivery
Packaging protects the finished surfaces of this stainless steel component: interleaving, bagging or tray packing is matched to the surface, then sealed cartons are palletised for export, with documents and marks to your instruction.