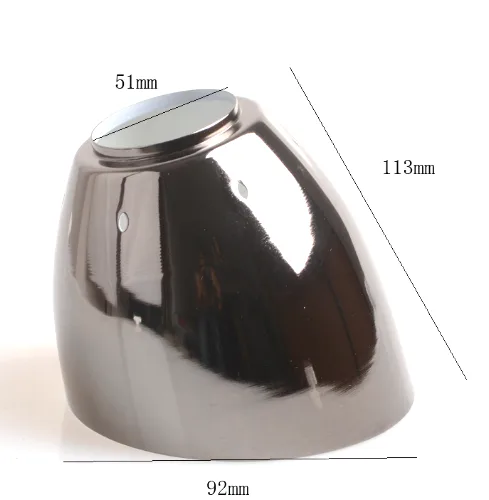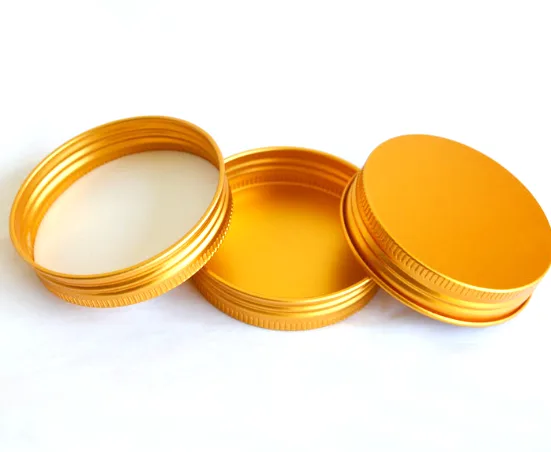
This Custom Sheet Metal Deep Drawn Process is an Aunov Tech production part in stainless steel, quoted and built to customer print. In the assembly, the deep drawn part replaces a machined-from-solid body with a lighter, faster drawn shell. Forming and machining share equipment, staff and batch records, so the approved sample defines every later batch under one roof.
Product overview
What defines this metal component is, material grade, wall uniformity and thread position, controlled from the approved first article onward.
Tooling and finishing for this metal component run under one roof, so a change of wall or hole does not restart the programme, and the same die can be re-cut from the original data.
How it is manufactured
Production of this metal component is locked to one route: Coil is blanked and drawn through progressive and single-stage dies; piercing and trimming are done in the same die line.
The screw-top jar manufacturing record is archived together with the drawing revision that produced it. Process settings for the screw-top jar are archived, so later runs can be compared with the one you approved.
Materials and finishing
Base materials in stock: cold-rolled steel (SPCC / DC01), 304 / 316 stainless, aluminium, brass, copper and bronze with carbon steel or stainless specified on the drawing for this metal component.
Finish selection follows the working environment: electrophoresis, powder coating, anodising and zinc / nickel plating. Once approved, the finish for this metal component is fixed and does not get re-decided.
The screw-top jar manufacturing record is archived together with the drawing revision that produced it. Process settings for the screw-top jar are archived, so later runs can be compared with the one you approved.
Quality control
The plant is ISO 9001 certified: mill certificates cover every delivery of stock, the first article is CMM-measured against the print, and every production run is inspected against the first-article report. The screw-top jar first article goes on the CMM, with threads gauged to class. Tests for torque, leakage or pressure can be arranged when the service demands them, and results travel with the batch paperwork.
Where the part is used
The metal component is fitted into industrial equipment and general assembly work in volume programmes as well as aftermarket supply.
The same metal component is often run in more than one assembly, so wall bands and finishes are selected to cover the widest duty, and no re-tooling is needed.
Customization and options
Options that vary most in this screw-top jar family
The parts of the print for this metal component that get adjusted: wall thickness bands, flange geometry, thread call-outs and the surface finish, and the batch pattern – prototype, pilot lot or scheduled production.
The quote for this metal component separates tooled options from new work, so new tooling is only quoted where it is genuinely required. The screw-top jar price is locked for the validity period on the quote.
Specifications
| Item | Custom Sheet Metal Deep Drawn Process |
|---|---|
| Brand | AUNOV |
| Designing | Driven by your drawing or a physical sample – unusual walls, threads or tolerances are feasibility-checked first; changes are priced before they are made. |
| Tooling | Progressive and drawing dies are designed and built in house, so the die charge appears as its own quotation line, and ownership is confirmed on the quotation. |
| Samples | First-article samples ship with a dimensional report and material certificate, so any deviation is corrected at sample stage, and mass production is gated on that approval. |
| Materials | Carbon steel (SPCC / DC01), 304 / 316 stainless, aluminium and brass are held on site; special grades are sourced to the drawing when volumes justify. |
| Surface finish | Plating, powder coating, anodising or polishing, per the print; the agreed finish travels with the part number. |
| Processing | Progressive drawing through several stages, annealed between draws, then trim and pierce; every stage is logged against your part number. |
| Equipment | Mechanical presses from 5 to 250 T and hydraulic presses 250-500 T, with in-line annealing furnaces, with CNC turning centres for secondary operations and CMM inspection. |
| Tolerance | +/-0.05 mm on formed features, with capability data on critical dimensions; GD&T per drawing, PPAP-style reports on request. |
| Delivery terms | FOB Ningbo or Shanghai, T/T with deposit and L/C for larger runs; each volume tier carries its own quoted price. |
Packaging and delivery
The finish on this metal component dictates how it is packed: interleaves, bags or trays are matched to the surface treatment, in sealed cartons on export pallets, with documents issued to your instructions.