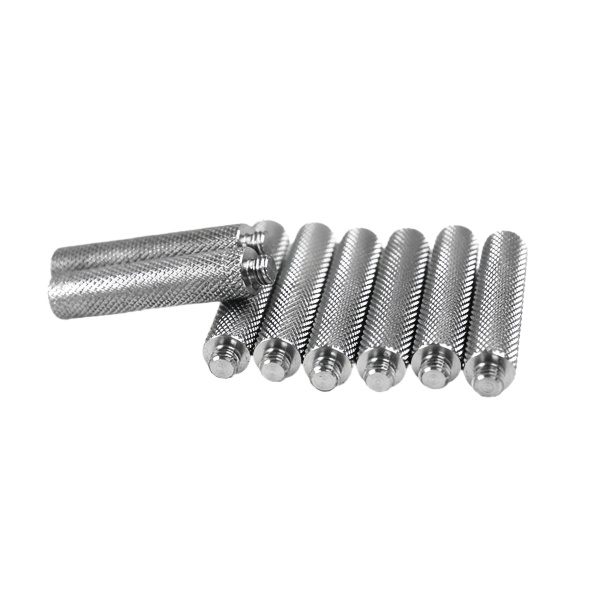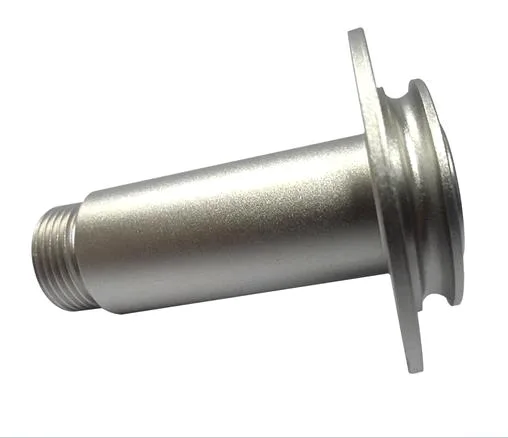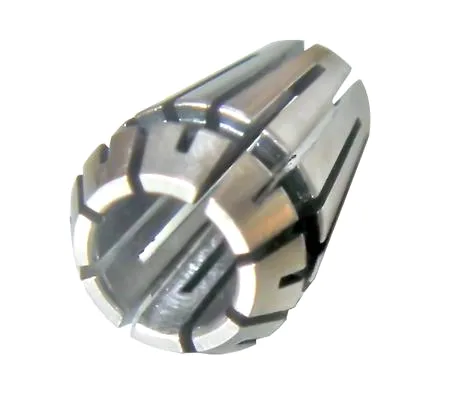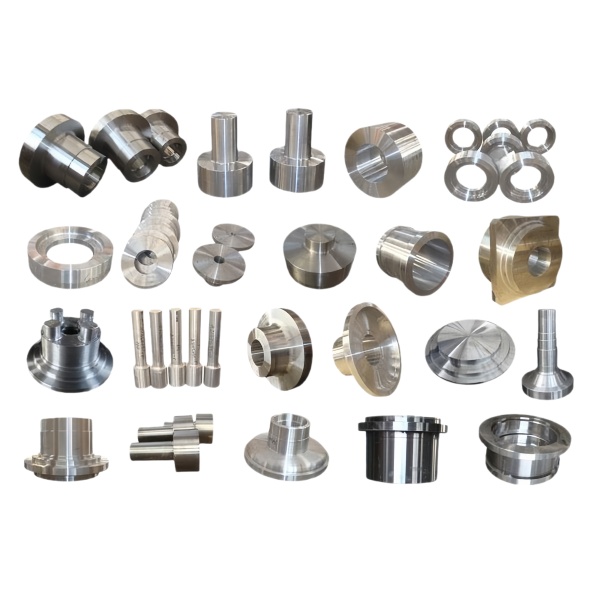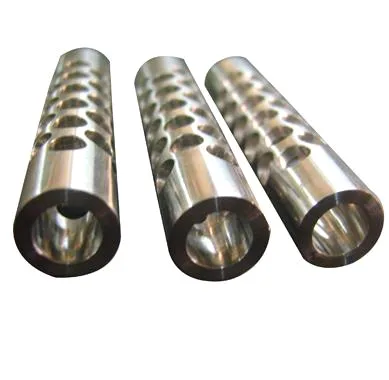
The Precision CNC Turning and Milling Components is produced by Aunov Tech from stainless steel, formed and finished under one roof. In service, the CNC machined part carries the controlled features that forming alone cannot hold. One production floor covers forming, finishing and inspection, which keeps tolerances consistent from sample to volume without re-quoting the job elsewhere.
Product overview
This metal component is defined by, draw depth, wall band and the surfaces that forming cannot hold, recorded on the inspection report for every batch.
Die work and machining for this metal component sit on the same floor, so a drawing change is absorbed in one step, with the tooling history retained in house.
How the part is produced
Manufacturing runs on a controlled process path: The part is machined from bar or plate on CNC lathes and mills; deburring and edge blending complete the operation before inspection.
Each drilled taper sleeves, shipment is verified against the master sample before it leaves the shop. The approved drilled taper sleeves, sample governs later runs, and any grade change is agreed in writing first.
Materials and finishing
Working stock covers carbon steel SPCC / DC01, 304 and 316 stainless, aluminium, brass and copper and the grade agreed for this metal component is carbon steel or stainless.
The surface treatment is picked to match the service conditions: zinc, nickel or chrome plating, anodising, powder coating, electrophoresis and passivation. It is fixed on the drawing for this metal component, so repeat orders never reopen the question.
The drilled taper sleeves, tooling and setup record is stored against the part number, so nothing depends on someone remembering. The signed drilled taper sleeves, sample remains the reference and is kept with the job file.
Quality control and inspection
An ISO 9001 certified system governs production: incoming material is verified against mill certificates, first-article geometry is confirmed on the CMM, and every production run is inspected against the first-article report. For the drilled taper sleeves,, first articles are CMM measured and threads are gauged to class. Functional testing – torque, leak or pressure – can be written into the plan, and the report is packed with the shipment.
Applications
This metal component normally works inside industrial machinery and equipment assemblies under schedules that run for years at a time.
One part number for this metal component frequently serves several assemblies, so the finish is chosen to cover the harshest of them, and approvals carry across programmes.
Customization and options
Where designs usually differ
Options customers tend to adapt on this metal component: material and coating for the duty, wall bands, flange forms, threads and bosses, closed ends and finishes matched to the working environment, and how the order is released – sample, pilot run or scheduled call-off.
Tooled and untooled options for this metal component are listed separately, so the effect of a revision on price is clear up front. Prices for the drilled taper sleeves, are held for the agreed validity period.
Specifications
| Item | Precision CNC Turning and Milling Components |
|---|---|
| Brand | AUNOV |
| Designing | Driven by your drawing or a physical sample – unusual walls, threads or tolerances are feasibility-checked first; the agreed version governs every later batch. |
| Tooling | Our toolroom covers die design, wire-cut EDM and maintenance, so a die can be re-cut against the approved drawing, and the die remains dedicated to your part. |
| Samples | Pre-production samples come with a full inspection report, so the part is proven before it is made in volume, and later batches are gauged back to the signed sample. |
| Materials | Standard stock: carbon steel (SPCC / DC01), 304 / 316 stainless, aluminium, brass; mill certificates and heat numbers accompany the first article. |
| Surface finish | Zinc, nickel or chrome plating, anodising, passivation or e-coat; the finish is inspected with the dimensional report on the first article. |
| Processing | Turning, milling and drilling sequenced to minimise handling and re-chucking; in-process checks sit between stages, not only at the end. |
| Equipment | 12 CNC turning centres with automatic bar feeders, with in-house toolmaking to keep dies and fixtures maintained. |
| Tolerance | +/-0.01 mm on turned and milled features; GD&T per drawing, PPAP-style reports on request. |
| Delivery terms | FOB, CIF or DDP per Incoterms 2020, T/T or L/C, with D/P accepted on repeat business; repeat orders reuse the approved first article. |
Packaging and delivery
Packing for this metal component is chosen around the coating: interleaving, individual bags or trays are chosen by finish type, in sealed export cartons, palletised and marked as you direct.