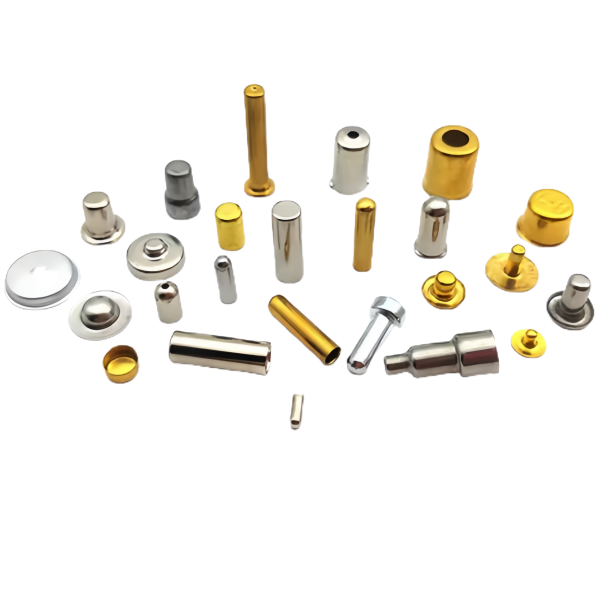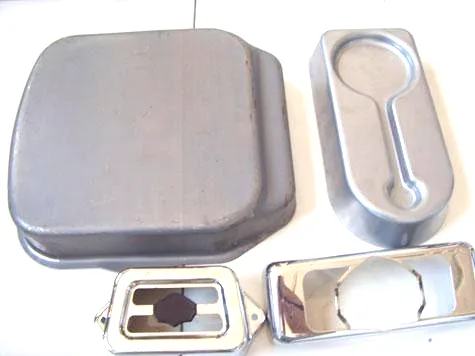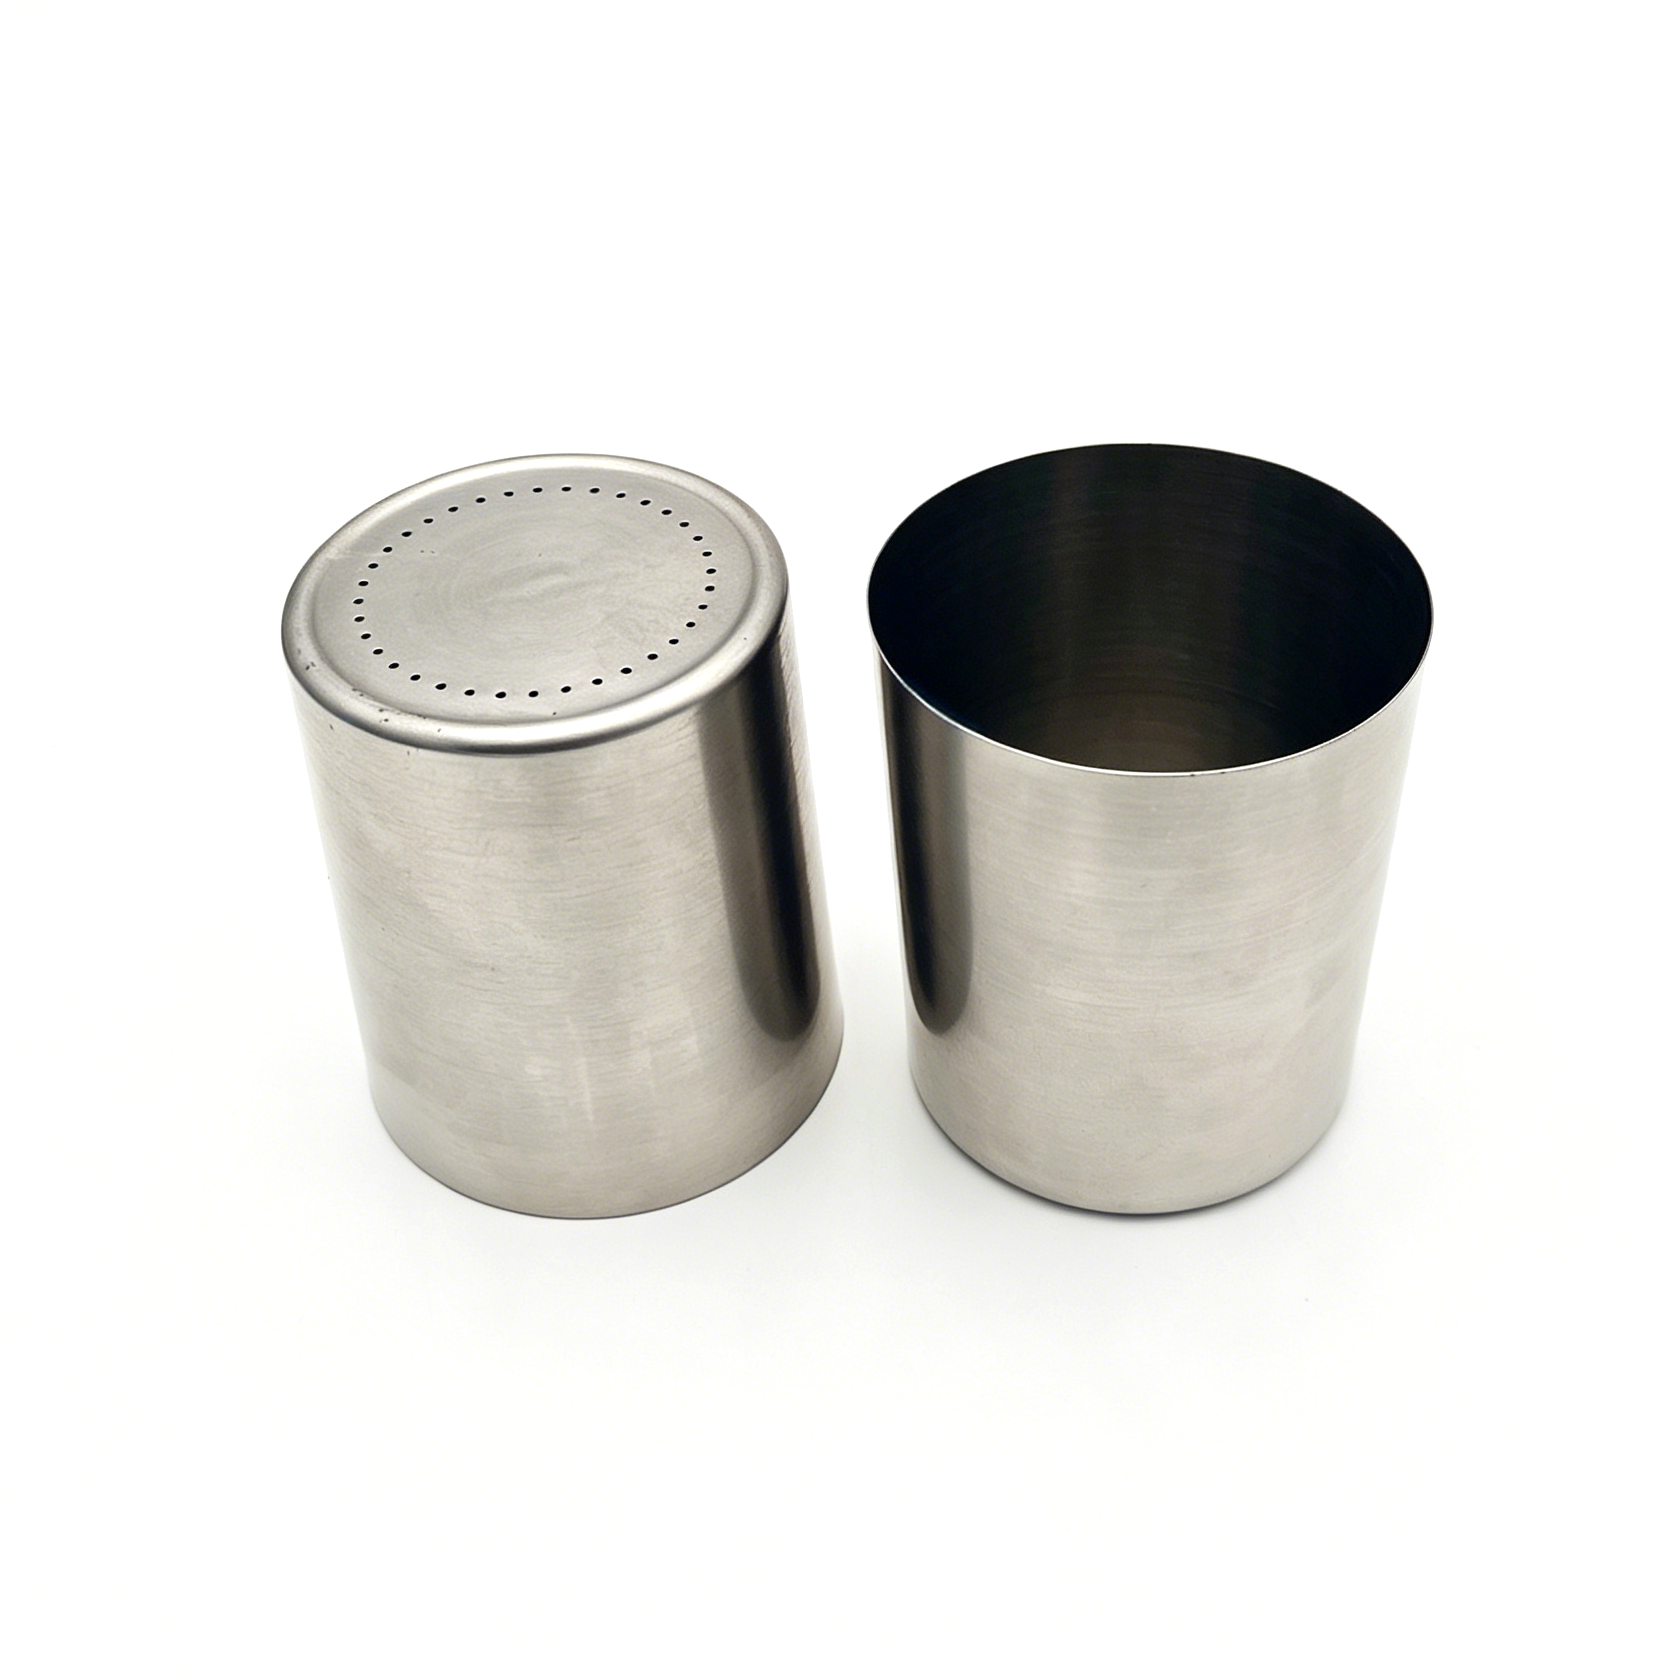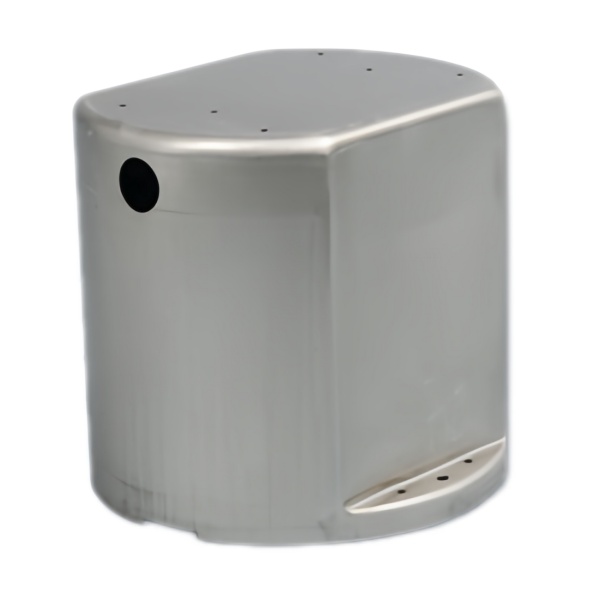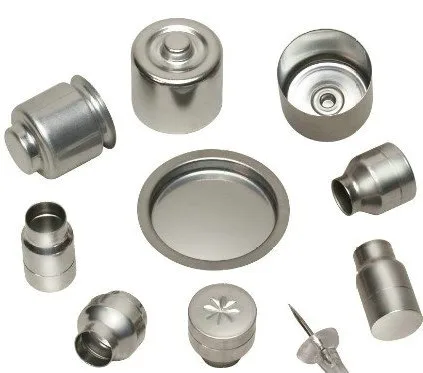
Produced in brass or stainless steel by Aunov Tech, the Sales Deep Drawn Motor Parts Metal Brass Stainless Steel Sheet Metal is formed and machined on the same floor. Once installed, the deep drawn part combines forming and machining to reach the print on every controlled face. Die work, machining and CMM inspection are all in-house, keeping first-article quality through scheduled runs with no third party in the loop.
Product overview
For this stainless steel component, the drawing centres on, wall thinning, concentricity and the finished mating faces, recorded on the inspection report for every batch.
Toolroom, presses and machining centres used on this stainless steel component operate on the same site, which keeps revision loops short and samples fast, and the approved sample is kept as the master.
How it is manufactured
The route for this stainless steel component is fixed and repeatable: Coil is blanked and drawn through progressive and single-stage dies; secondary machining holds the seats, threads and faces that forming cannot produce.
A cup carries one job in the assembly, and every tolerance on it exists to protect that job. That is why the cup is inspected between operations, not only at the end.
Materials and surface finish
Base materials in stock: carbon steel SPCC / DC01, 304 and 316 stainless, aluminium, brass and copper and the grade agreed for this stainless steel component is 304 / 316 stainless steel.
The finish is chosen for the duty it will see: plating, anodising, powder coating, electrophoresis and passivation. The agreed finish for this stainless steel component travels with the part number on every reorder.
Each shipment is verified against the master sample, so the colour and grain of the finish stay stable.
Quality control
The factory operates with ISO 9001 certification: certificates verify each incoming batch of material, a full CMM report approves the first article, and run inspections follow an agreed sampling plan. First article of the cup: CMM data on diameters, thread class confirmed by gauge. Torque, leak and pressure tests are available where the assembly needs them, with certificates included in the shipment file.
Typical applications
You will find this stainless steel component inside industrial and appliance assemblies under schedules that run for years at a time.
The same stainless steel component is used across several platforms, so the finish is chosen to cover the harshest of them, and the die does not have to change.
Customization and options
Where designs usually differ
Points customers normally tailor on this stainless steel component: material and coating for the duty, wall bands, flange forms, threads and bosses, closed ends and finishes matched to the working environment, and whether the first order is a prototype, a pilot lot or a production release.
The quotation for this stainless steel component marks what the existing tooling can do, so the boundary between free and chargeable changes is explicit. Price validity for the cup is stated on the quotation and respected.
Specifications
| Item | Sales Deep Drawn Motor Parts Metal Brass Stainless Steel Sheet Metal |
|---|---|
| Brand | AUNOV |
| Designing | Driven by your drawing or a physical sample – unusual walls, threads or tolerances are feasibility-checked first; changes are priced before they are made. |
| Tooling | Progressive and drawing dies are designed and built in house, so tooling lead time stays under our control, and first-article timing is measured from the tooling start date. |
| Samples | Samples are issued for approval before the run, and production starts only after written sign-off. |
| Materials | Materials held include carbon steel, 304 / 316 stainless, aluminium and brass; the final grade is fixed with the drawing review. |
| Surface finish | Finish selected from the drawing: plating, coating, anodising or passivation; finish thickness and adhesion checked on the first article. |
| Processing | Coil blanking and progressive drawing, coining on the final station where the print calls for it; batch records are filed so a repeat order starts from approved data. |
| Equipment | Mechanical presses from 5 to 250 T and hydraulic presses 250-500 T, with in-line annealing furnaces, backed by CNC turning centres and a climate-controlled inspection room. |
| Tolerance | +/-0.1 mm general on drawn sections, +/-0.03 mm on machined seats; finer bands confirmed from capability data before quoting. |
| Delivery terms | CIF or DDP, with FOB available, payment by T/T, L/C at sight or D/P; each volume tier carries its own quoted price. |
Packaging and delivery
Packing for this stainless steel component is chosen around the coating: interleaving, bagging or tray packing is matched to the surface, in sealed cartons on export pallets, documented and marked to your instruction.