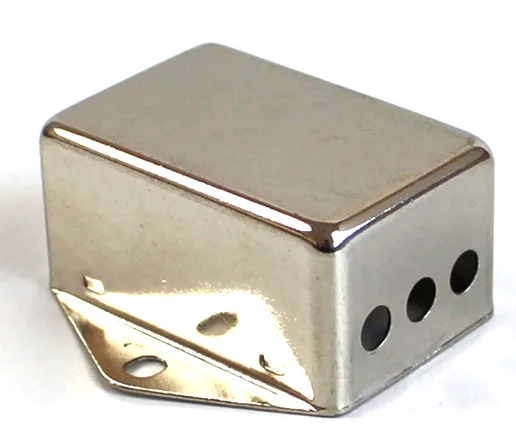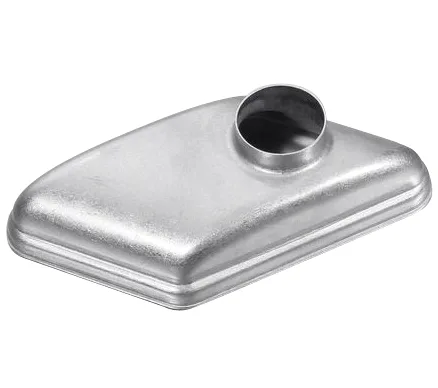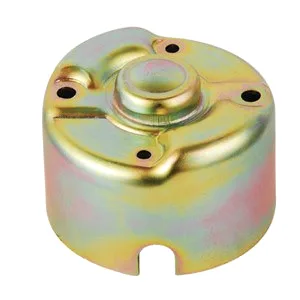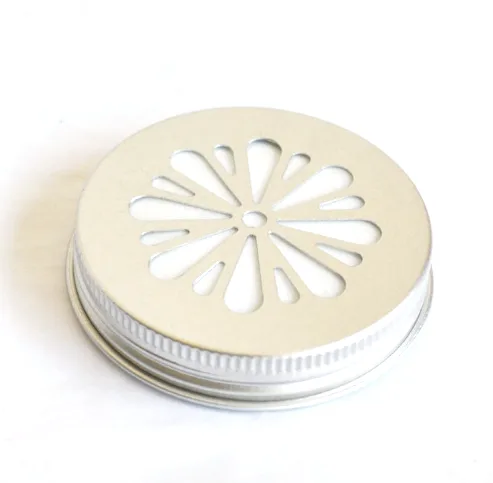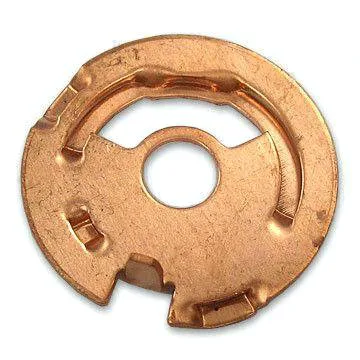
Produced in aluminum by Aunov Tech, the Deep Drawn Aluminum Rotor is formed and machined on the same floor. In operation, the deep drawn part carries the formed geometry the assembly needs at volume. One production floor covers forming, finishing and inspection, keeping first-article quality through scheduled runs with no third party in the loop.
Product overview
The drawing for this aluminium component fixes, wall thickness control, flange geometry and the sealing surface, each measured at first article and gauged on production batches.
Die work and machining for this aluminium component sit on the same floor, so feasibility questions are answered on the shop floor, with the tooling history retained in house.
How it is manufactured
Every aluminium component follows the same routed path: Drawing converts a flat blank into the finished envelope in one controlled sequence; wall thickness is checked at the thinnest section after forming.
Production batches of the contact rotor disc are gauged back to the signed first article, not to a memory of it. Process settings for the contact rotor disc are archived, so later runs can be compared with the one you approved.
Materials and finishing
Materials kept on the floor cover SPCC / DC01 carbon steel, 304 / 316 stainless, aluminium, brass, copper and bronze with this aluminium component costed in aluminium.
The finish is chosen for the duty it will see: zinc, nickel or chrome plating, anodising, powder coating, electrophoresis and passivation. The choice is recorded on the drawing for this aluminium component, so the decision never has to be made twice.
Later runs are measured back to the first article, with mill certificates filed per heat.
Quality control
The factory operates with ISO 9001 certification: material traceability starts with mill certificates, a full CMM report approves the first article, and routine sampling keeps batches aligned with the first article. The contact rotor disc first article is measured on the CMM and thread gauges confirm class. Where the application asks for it, torque, leak or pressure testing is added to the plan, and results travel with the batch paperwork.
Applications
This aluminium component is used in industrial equipment and general assembly work in both OEM and aftermarket supply.
A single design of this aluminium component is often reused across a product family, so wall bands and finishes are selected to cover the widest duty, and cost per piece stays at the volume tier.
Customization and options
Frequently varied options in this contact rotor disc family
The parts of the print for this aluminium component that get adjusted: material grade, coating, wall bands, flange form and end closure, and the batch pattern – prototype, pilot lot or scheduled production.
Options for this aluminium component already covered by the die are shown on the quote, so new tooling is only quoted where it is genuinely required. No change is made to the contact rotor disc without a written revision.
Specifications
| Item | Deep Drawn Aluminum Rotor |
|---|---|
| Brand | AUNOV |
| Designing | Made to your 2D/3D drawings (PDF, DWG, STEP, IGS) – DFM notes are returned before any tooling is cut; the agreed version governs every later batch. |
| Tooling | Our toolroom covers die design, wire-cut EDM and maintenance, so no tooling step is outsourced, and the die remains dedicated to your part. |
| Samples | First-article samples ship with a dimensional report and material certificate, so the sample is retained as the master, and production starts only after your written sign-off. |
| Materials | Standard stock: carbon steel (SPCC / DC01), 304 / 316 stainless, aluminium, brass; special grades are sourced to the drawing when volumes justify. |
| Surface finish | Plating, powder coating, anodising or polishing, per the print; alternatives quoted with the quotation, samples approved in writing. |
| Processing | Deep drawing from coil or blank, with in-process annealing so walls thin evenly; batch records are filed so a repeat order starts from approved data. |
| Equipment | 5-250 T mechanical presses, 250-500 T hydraulic presses and annealing furnaces in line, backed by CNC turning centres and a climate-controlled inspection room. |
| Tolerance | +/-0.03 mm on turned secondary features, +/-0.1 mm on as-drawn walls; dimensional reports accompany the first article. |
| Delivery terms | FOB Ningbo or Shanghai, T/T with deposit and L/C for larger runs; call-off schedules are supported. |
Packing and shipment
The packing method protects the surfaces of this aluminium component: interleaves, bags or trays are matched to the surface treatment, in sealed export cartons, palletised and marked as you direct.