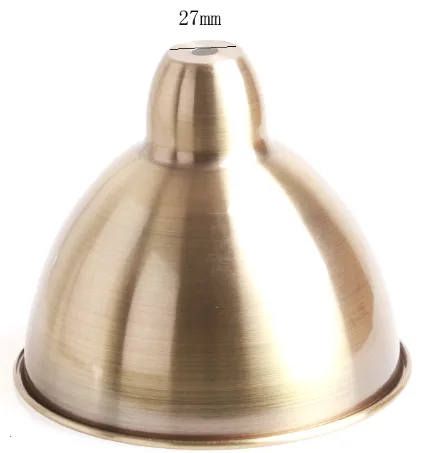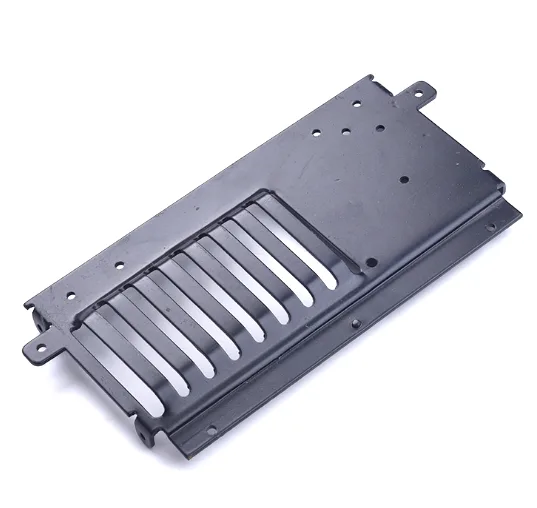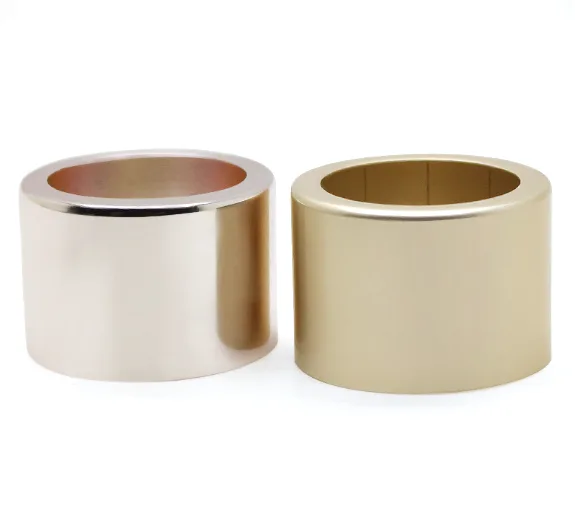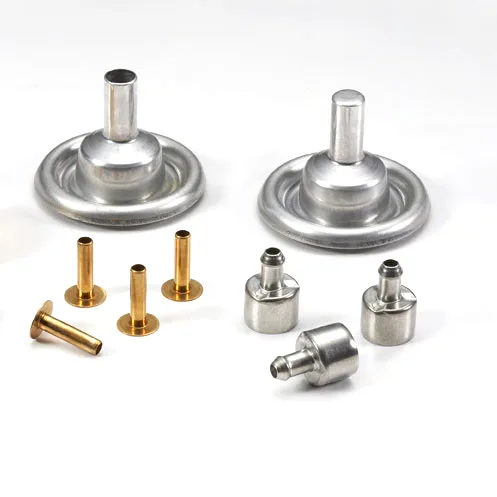
Aunov Tech builds this Custom Deep Drawn Hydroforming Metal Spinning Aluminum Deep Drawing in aluminum, from coil or bar through to the finished surfaces. In duty, the CNC machined part provides the finished surfaces, threads and seats the mating parts locate on. Forming and machining share equipment, staff and batch records, so the approved sample defines every later batch without a second supplier involved.
Product overview
The drawing for this aluminium component fixes, material grade, wall uniformity and thread position, re-checked whenever the drawing is revised.
Toolroom, presses and machining centres used on this aluminium component operate on the same site, so the route from print to sample stays short, and the approved sample is kept as the master.
How it is manufactured
Manufacturing runs on a controlled process path: A tube preform is expanded against the die by internal pressure; ends are trimmed and pierced, then the part is annealed and finished.
Repeat hydroformed dome shell orders are measured against the approved sample, so neither material nor finish drifts between lots. Process settings for the hydroformed dome shell are archived, so later runs can be compared with the one you approved.
Materials and finishing
Materials kept on the floor cover cold-rolled steel (SPCC / DC01), 304 / 316 stainless, aluminium, brass, copper and bronze and this aluminium component runs in aluminium.
Coating and polishing are matched to the end use: zinc, nickel or chrome plating, anodising, powder coating, electrophoresis and passivation. It is written into the drawing for this aluminium component, so it cannot drift between batches.
Material certs and dimensional reports come with the batch on request.
Quality control
The factory operates with ISO 9001 certification: certificates verify each incoming batch of material, a full CMM report approves the first article, and every production run is inspected against the first-article report. First-article inspection of the hydroformed dome shell runs on the CMM: thread classes gauged, diameters logged. If the assembly calls for torque, leak or pressure proof, the test is built into the quality plan, and results travel with the batch paperwork.
Typical applications
The aluminium component is fitted into industrial machinery and equipment assemblies for OEM and Tier-1 customers.
A single design of this aluminium component is often reused across a product family, so the finish is chosen to cover the harshest of them, and cost per piece stays at the volume tier.
Customization and options
Frequently varied options
Typical decisions customers make on this aluminium component: coating, wall bands, flange profiles, threads and the degree of closure on the ends, with orders run as prototypes, pilot lots or scheduled call-offs.
Quotes for this aluminium component show which options the current die already supports, so the effect of a revision on price is clear up front. A written revision is required before any hydroformed dome shell change is actioned.
Specifications
| Item | Custom Deep Drawn Hydroforming Metal Spinning Aluminum Deep Drawing |
|---|---|
| Brand | AUNOV |
| Designing | Made to your 2D/3D drawings (PDF, DWG, STEP, IGS) – a manufacturability review comes back with the quotation; revisions are re-quoted once rather than silently absorbed. |
| Tooling | Dies, fixtures and gauges are made in our own toolroom, so tooling lead time stays under our control, and ownership is confirmed on the quotation. |
| Samples | Samples are issued for approval before the run, so the approved first article becomes the gauge reference, and the signed sample is kept for future reorders. |
| Materials | Materials held include carbon steel, 304 / 316 stainless, aluminium and brass; special grades are sourced to the drawing when volumes justify. |
| Surface finish | Surface treatment matched to the duty: plating, coating or polishing; finish thickness and adhesion checked on the first article. |
| Processing | Tube or sheet preform, hydroforming into the finished contour, trimming, then annealing and finishing. |
| Equipment | 5-250 T mechanical presses, 250-500 T hydraulic presses and annealing furnaces in line, with CNC turning centres for secondary operations and CMM inspection. |
| Tolerance | +/-0.03 mm on turned secondary features, +/-0.1 mm on as-drawn walls; GD&T per drawing, PPAP-style reports on request. |
| Delivery terms | Freight is quoted to your door in FOB, CIF or DDP terms, payment by T/T or L/C. |
Packaging and delivery
The finish on this aluminium component dictates how it is packed: interleaving, individual bags or trays are chosen by finish type, then cartons are sealed and palletised, with marks and documents as you specify.