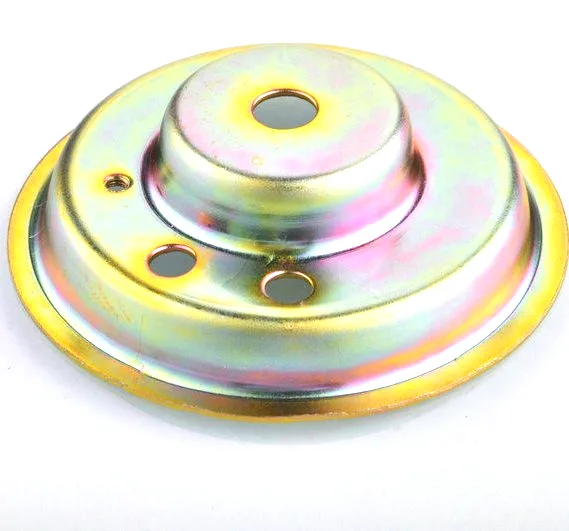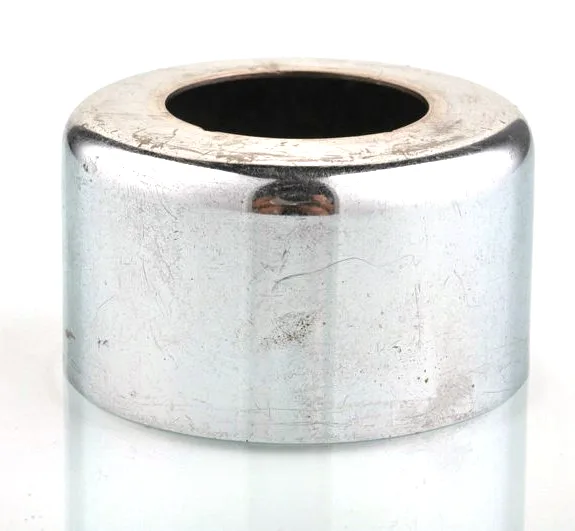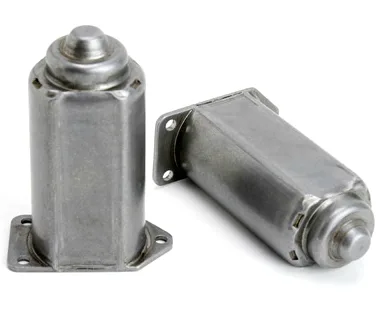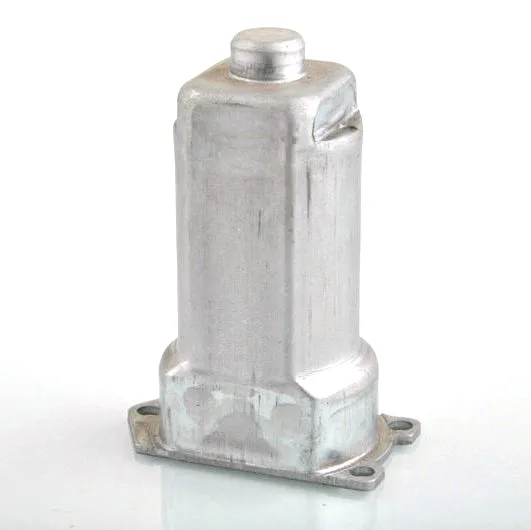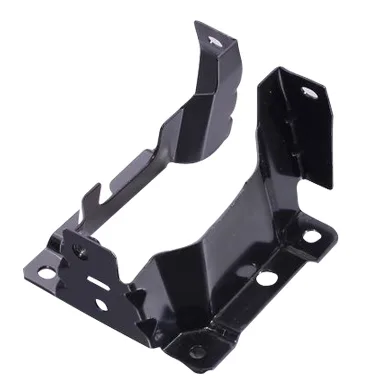
The Deep Drawn Stainless Steel Stamping Deep Drawing Aluminum is produced by Aunov Tech from aluminum or stainless steel, formed and finished under one roof. In duty, the deep drawn part carries the formed geometry the assembly needs at volume. Forming and machining share equipment, staff and batch records, keeping first-article quality through scheduled runs under one roof.
Product overview
For this stainless steel component, the drawing centres on, the draw ratio, corner radii and the faces that must stay flat, re-checked whenever the drawing is revised.
Die work and machining for this stainless steel component sit on the same floor, so the route from print to sample stays short, with the tooling history retained in house.
How it is manufactured
Manufacturing runs on a controlled process path: Blanks are drawn in stages, with interstage annealing where the wall thins; secondary machining holds the seats, threads and faces that forming cannot produce.
Each black automotive bracket shipment is verified against the master sample before it leaves the shop. Mill certificates are filed per heat, so black automotive bracket traceability survives a change of material batch.
Materials and finishing
Standard stock includes cold-rolled steel (SPCC / DC01), 304 / 316 stainless, aluminium, brass, copper and bronze with this stainless steel component costed in 304 / 316 stainless steel.
Coating and polishing are matched to the end use: plating, anodising, powder coating, electrophoresis and passivation. Once approved, the finish for this stainless steel component is fixed and does not get re-decided.
Each black automotive bracket shipment is verified against the master sample before it leaves the shop. Mill certificates are filed per heat, so black automotive bracket traceability survives a change of material batch.
Quality control
Production runs under an ISO 9001 certified quality system: mill certificates cover every delivery of stock, the first article is CMM-measured against the print, and routine sampling keeps batches aligned with the first article. The black automotive bracket first article goes on the CMM, with threads gauged to class. Torque, leak and pressure tests are available where the assembly needs them, and the batch file carries the results.
Applications
The stainless steel component is fitted into industrial equipment and general assembly work under schedules that run for years at a time.
This stainless steel component is supplied to several positions in the same machine, so one tooling set serves every position, and the drawing stays common.
Customization and options
What customers usually vary
Typical decisions customers make on this stainless steel component: coating, wall bands, flange profiles, threads and the degree of closure on the ends, and the batch pattern – prototype, pilot lot or scheduled production.
The quotation for this stainless steel component is explicit about what the die already covers, so new tooling is only quoted where it is genuinely required. Repeat orders of the black automotive bracket keep the same cost split.
Specifications
| Item | Deep Drawn Stainless Steel Stamping Deep Drawing Aluminum |
|---|---|
| Brand | AUNOV |
| Designing | Quotation follows the print, not a catalogue – a manufacturability review comes back with the quotation; changes are priced before they are made. |
| Tooling | Tooling is built and held under your part number, so the die charge appears as its own quotation line, and the die remains dedicated to your part. |
| Samples | Prototype and pre-production samples are provided against the drawing, so any deviation is corrected at sample stage, and later batches are gauged back to the signed sample. |
| Materials | Stock covers carbon steel (SPCC / DC01), 304 / 316 stainless, aluminium and brass; special grades are sourced to the drawing when volumes justify. |
| Surface finish | Plating, coating or polishing to suit the drawing; alternatives quoted with the quotation, samples approved in writing. |
| Processing | Coil-fed stamping, deburred and finished to the print; in-process checks sit between stages, not only at the end. |
| Equipment | 5-250 T presses running progressive and compound dies; first articles and batch samples are checked on the CMM. |
| Tolerance | +/-0.05 mm to +/-0.1 mm across the part; GD&T per drawing, PPAP-style reports on request. |
| Delivery terms | FOB, CIF or DDP per Incoterms 2020, T/T or L/C, with D/P accepted on repeat business; repeat orders reuse the approved first article. |
Packaging and delivery
The finish on this stainless steel component dictates how it is packed: interleaving, individual bags or trays are chosen by finish type, in sealed export cartons, palletised and marked as you direct.