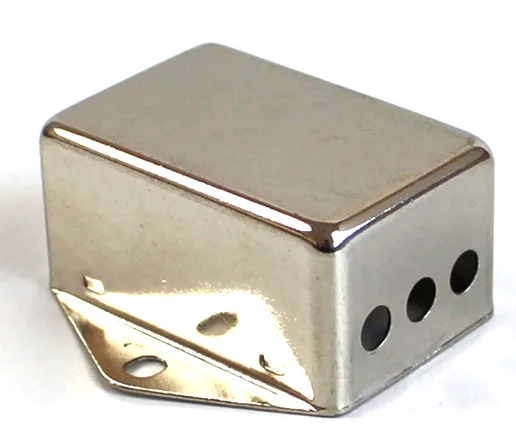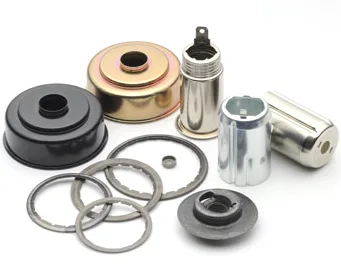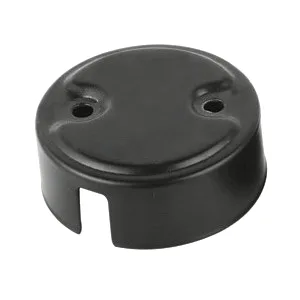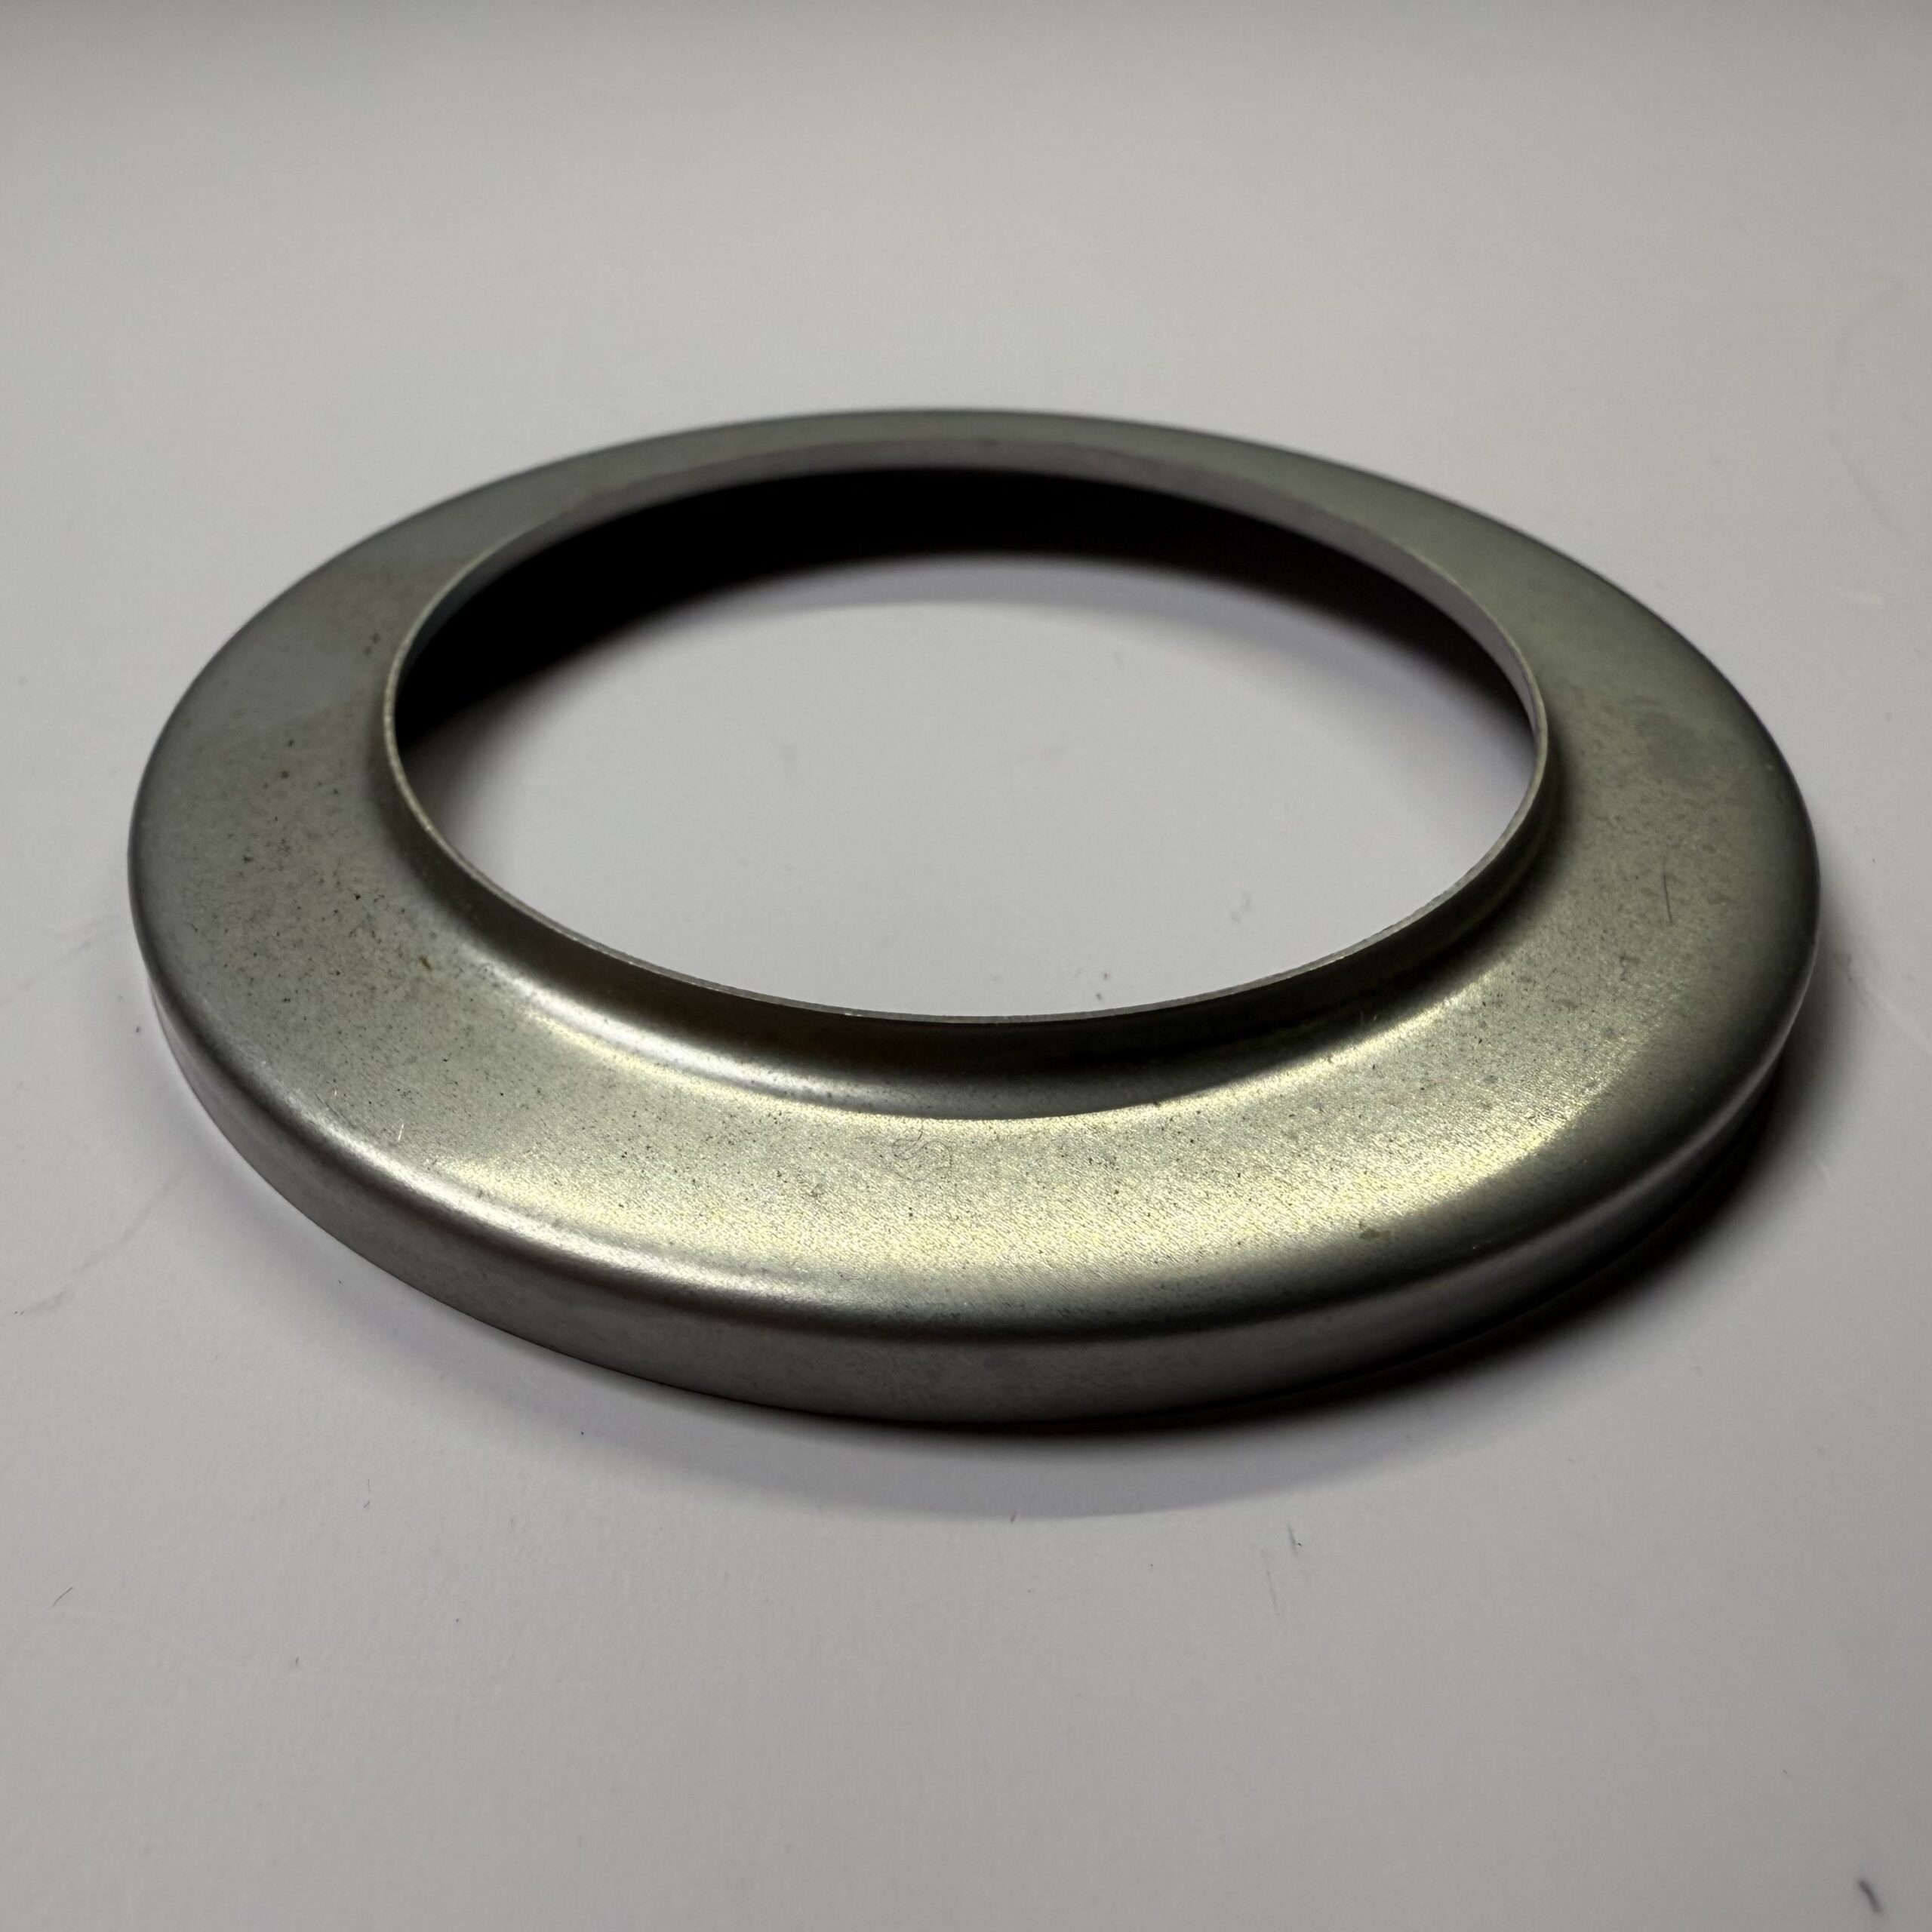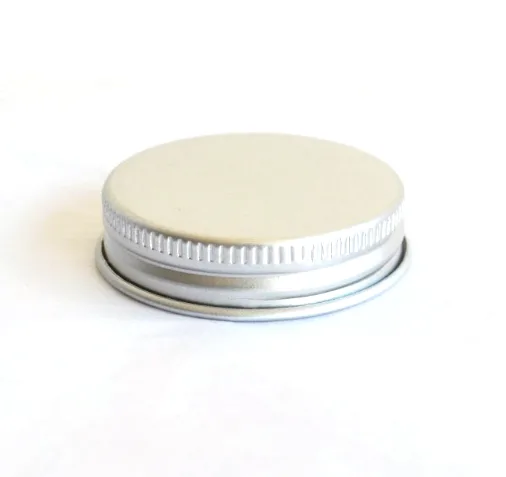
Aunov Tech manufactures the Sheet Metal Deep Drawn Stamped Parts Stainless Steel Deep Drawing in stainless steel on a single production floor. Once installed, the deep drawn part carries the formed geometry the assembly needs at volume. The same floor forms, machines and inspects the part, so the approved sample defines every later batch without re-quoting the job elsewhere.
Product overview
The specification of this stainless steel component turns on, wall thinning, concentricity and the finished mating faces, recorded on the inspection report for every batch.
Tooling and finishing for this stainless steel component run under one roof, so revisions do not wait on outside suppliers, and the approved sample is kept as the master.
Production route
The process for this stainless steel component runs in a fixed sequence: Coil is blanked and drawn through progressive and single-stage dies; piercing and trimming are done in the same die line.
Route cards follow each knurled edge lid batch through the shop, so the next run starts from the data that already worked. Deviations on the knurled edge lid are reported before shipment rather than found on your assembly line.
Materials and finishing
Standard stock includes carbon steel SPCC / DC01, 304 and 316 stainless, aluminium, brass and copper and this stainless steel component runs in 304 / 316 stainless steel.
The surface treatment is picked to match the service conditions: polishing, zinc / nickel / chrome plating, anodising or powder coating. The choice is recorded on the drawing for this stainless steel component, so the decision never has to be made twice.
Material certs and dimensional reports come with the batch on request.
Quality control
The factory operates with ISO 9001 certification: incoming material is verified against mill certificates, first articles are measured on a CMM, and every production run is inspected against the first-article report. First-article inspection of the knurled edge lid runs on the CMM: thread classes gauged, diameters logged. Where the application asks for it, torque, leak or pressure testing is added to the plan, and results travel with the batch paperwork.
Applications
Typical installation of the stainless steel component is in industrial equipment and general assembly work across automotive, appliance and industrial programmes.
This stainless steel component is supplied to several positions in the same machine, so the tightest tolerance in the family sets the spec, and approvals carry across programmes.
Customization and options
Common variation points across this knurled edge lid family
Typical decisions customers make on this stainless steel component: grade and finish for the environment, wall thickness bands, flange and rim forms, threads, bosses and closed ends, and whether orders run as prototypes, pilot lots or scheduled batches.
The quotation for this stainless steel component marks what the existing tooling can do, so there are no surprise tooling charges after approval. Pricing on the knurled edge lid holds for the validity period agreed in writing.
Specifications
| Item | Sheet Metal Deep Drawn Stamped Parts Stainless Steel Deep Drawing |
|---|---|
| Brand | AUNOV |
| Designing | Made to your 2D/3D drawings (PDF, DWG, STEP, IGS) – unusual walls, threads or tolerances are feasibility-checked first; changes are priced before they are made. |
| Tooling | Tooling is built and held under your part number, so die cost stays transparent, and the die remains dedicated to your part. |
| Samples | Pre-production samples come with a full inspection report, so the approved first article becomes the gauge reference, and mass production is gated on that approval. |
| Materials | Standard stock: carbon steel (SPCC / DC01), 304 / 316 stainless, aluminium, brass; grade and temper are confirmed in writing before tooling. |
| Surface finish | Natural, plated or coated – the print decides, and the agreed finish is logged; finish thickness and adhesion checked on the first article. |
| Processing | Deep drawing on maintained presses, blank size and lubrication logged per run; every stage is logged against your part number. |
| Equipment | Mechanical presses from 5 to 250 T and hydraulic presses 250-500 T, with in-line annealing furnaces; first articles and batch samples are checked on the CMM. |
| Tolerance | +/-0.03 mm on turned secondary features, +/-0.1 mm on as-drawn walls; finer bands confirmed from capability data before quoting. |
| Delivery terms | CIF or DDP, with FOB available, payment by T/T or L/C, quoted in USD or EUR; call-off schedules are supported. |
Packaging and delivery
Packing for this stainless steel component is chosen around the coating: the coating decides whether parts are interleaved, bagged or tray-packed, in sealed cartons on export pallets, with documents issued to your instructions.