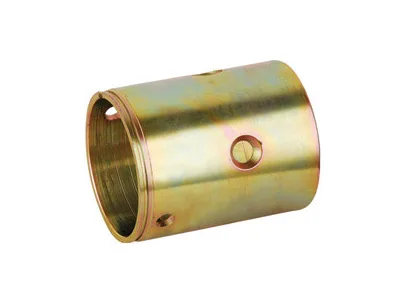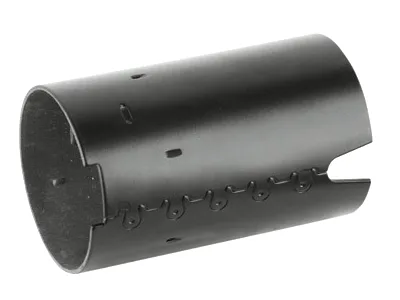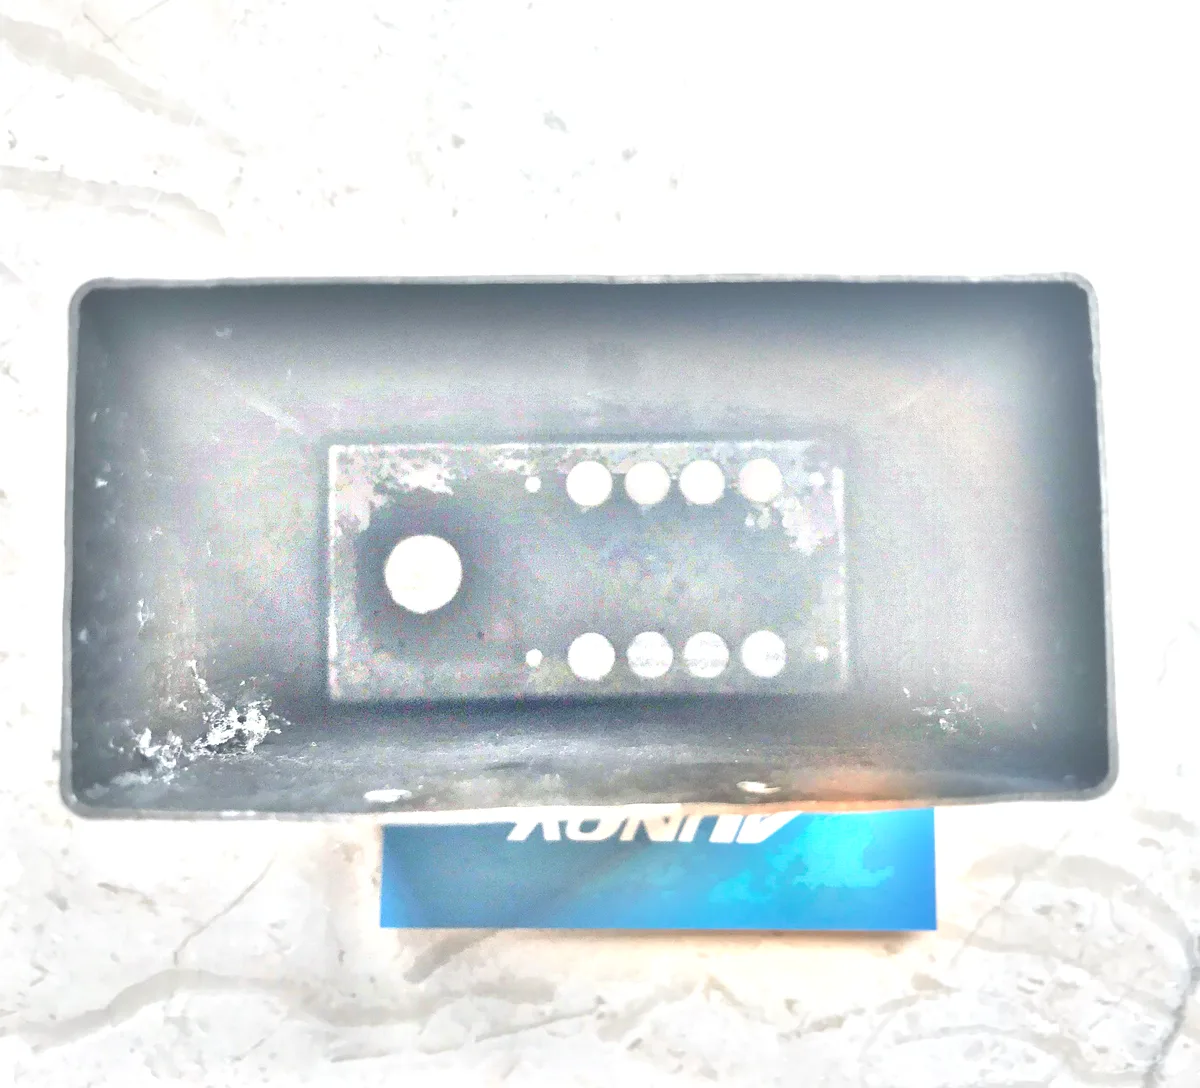
This Hydroformed Aluminum Night Vision Housing is an Aunov Tech production part in aluminum, quoted and built to customer print. In operation, the drawn housing provides a closed, seam-free body the customer builds into. Forming and machining share equipment, staff and batch records, so first-article dimensions hold through volume batches without a second supplier involved.
Product overview
This aluminium housing is defined by, wall thinning, concentricity and the finished mating faces, all held to the drawing and verified at first article.
Tooling and finishing for this aluminium housing run under one roof, so a change of wall or hole does not restart the programme, and nothing about the route depends on a third party.
How the part is produced
This is how the aluminium housing is built: A welded preform is expanded in the hydroforming press; ends are trimmed and pierced, then the part is annealed and finished.
Each shipment is traceable to the signed first article, and that record is what every reorder is built from.
Materials and finishing
Materials kept on the floor cover SPCC / DC01 carbon steel, 304 / 316 stainless, aluminium, brass, copper and bronze with aluminium specified on the drawing for this aluminium housing.
The finish is chosen for the duty it will see: polishing, plating in zinc, nickel or chrome, anodising, powder coating, electrophoresis and passivation. The choice is recorded on the drawing for this aluminium housing, so the decision never has to be made twice.
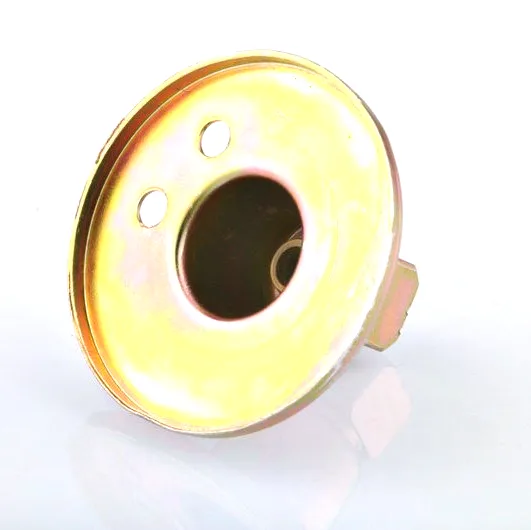
Batch records for the perforated cover plate are filed against the part number, so process settings are reused instead of re-invented. Deviations on the perforated cover plate are reported before shipment rather than found on your assembly line.
Quality control
Production runs under an ISO 9001 certified quality system: incoming material is verified against mill certificates, a full CMM report approves the first article, and every production run is inspected against the first-article report. The perforated cover plate first-article report carries cavity depth and seal face finish. If the assembly calls for torque, leak or pressure proof, the test is built into the quality plan, and the report is packed with the shipment.
Applications
The aluminium housing is specified into industrial and appliance assemblies for OEM and Tier-1 customers.
This aluminium housing is supplied to several positions in the same machine, so one tooling set serves every position, without a second tooling round.
Customization and options
Where designs usually differ
Typical decisions customers make on this aluminium housing: material grade, wall band, flange shape, thread size and finish for the working environment, and how the order is released – sample, pilot run or scheduled call-off.
The quotation for this aluminium housing is explicit about what the die already covers, so you are not charged twice for a feature the die already makes. Costs split the same way on each perforated cover plate reorder.
Specifications
| Item | Hydroformed Aluminum Night Vision Housing |
|---|---|
| Brand | AUNOV |
| Designing | DFM feedback accompanies the quotation, so surprises are caught before the die is cut. |
| Tooling | Dies, fixtures and gauges are made in our own toolroom, so a die can be re-cut against the approved drawing, and ownership is confirmed on the quotation. |
| Samples | Prototype and pre-production samples are provided against the drawing, so any deviation is corrected at sample stage, and mass production is gated on that approval. |
| Materials | Materials held include carbon steel, 304 / 316 stainless, aluminium and brass; special grades are sourced to the drawing when volumes justify. |
| Surface finish | Finish selected from the drawing: plating, coating, anodising or passivation; the finish is inspected with the dimensional report on the first article. |
| Processing | Coil blanking and progressive drawing, coining on the final station where the print calls for it; in-process checks sit between stages, not only at the end. |
| Equipment | Press shop running 5-250 T mechanical and 250-500 T hydraulic presses, annealing ovens on site, with CNC turning centres for secondary operations and CMM inspection. |
| Tolerance | +/-0.03 mm on turned secondary features, +/-0.1 mm on as-drawn walls; finer bands confirmed from capability data before quoting. |
| Delivery terms | Terms are FOB by default, with CIF and DDP quoted on request and freight priced to your door. |
Packing and shipment
Packaging protects the finished surfaces of this aluminium housing: each coating gets its own packing – interleaves, bags or trays, in sealed cartons on export pallets; shipping documents and carton marks follow your instructions.