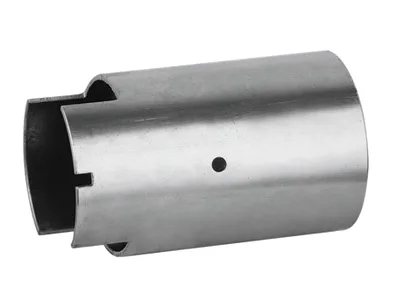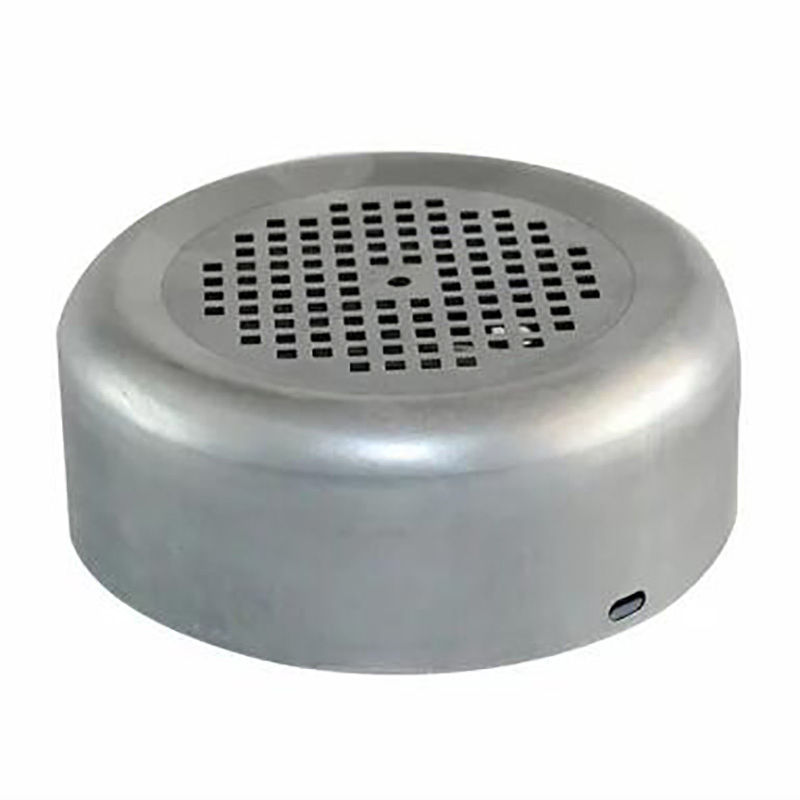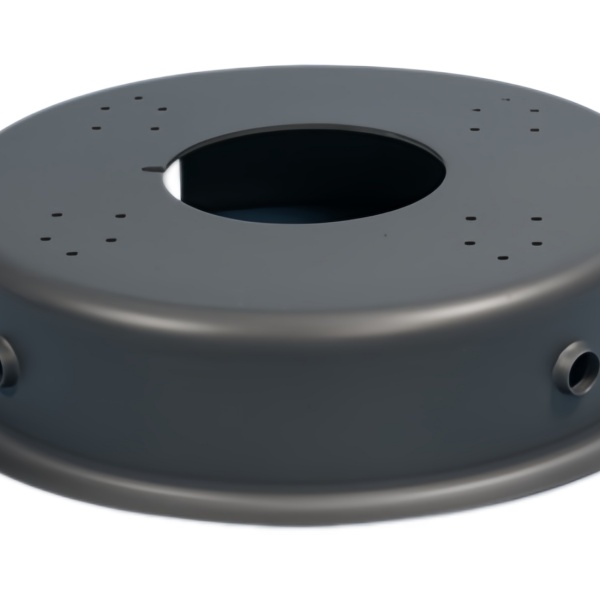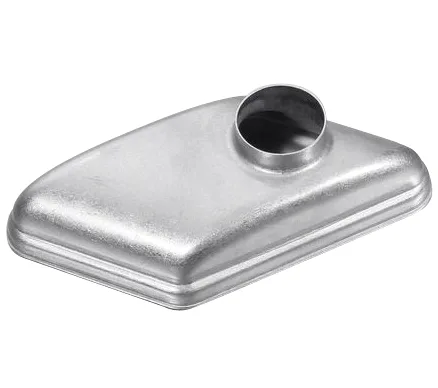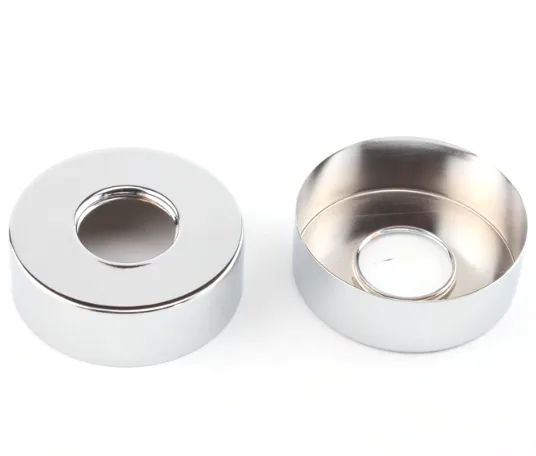
Produced in aluminum or stainless steel by Aunov Tech, the High-quality Custom Stainless Steel Deep Drawing Deep Drawing Aluminum is formed and machined on the same floor. Once installed, the CNC machined part carries the controlled features that forming alone cannot hold. The same floor forms, machines and inspects the part, keeping first-article quality through scheduled runs on one production route.
Product overview
The specification of this stainless steel component turns on, draw depth, wall band and the surfaces that forming cannot hold, re-checked whenever the drawing is revised.
Tooling and finishing for this stainless steel component run under one roof, so a drawing change is absorbed in one step, and the die record stays with your part number.
How it is manufactured
Manufacturing runs on a controlled process path: Drawing runs from flat blank to finished envelope in one controlled sequence; the finishing operations hold the concentricity the drawing calls for.
The cup manufacturing record is archived together with the drawing revision that produced it. Process settings for the cup are archived, so later runs can be compared with the one you approved.
Materials and finishing
Materials kept on the floor cover cold-rolled steel (SPCC / DC01), 304 / 316 stainless, aluminium, brass, copper and bronze and this stainless steel component is costed in 304 / 316 stainless steel.
The surface treatment is picked to match the service conditions: polishing, plating in zinc, nickel or chrome, anodising, powder coating, electrophoresis and passivation. The choice is recorded on the drawing for this stainless steel component, so the decision never has to be made twice.
The cup manufacturing record is archived together with the drawing revision that produced it. Process settings for the cup are archived, so later runs can be compared with the one you approved.
Quality control and inspection
Quality management is certified to ISO 9001: mill certificates cover every delivery of stock, first articles are measured on a CMM, and routine sampling keeps batches aligned with the first article. First-article inspection of the cup runs on the CMM: thread classes gauged, diameters logged. Torque, leak and pressure tests are available where the assembly needs them, and the inspection report ships with each batch.
Applications
This stainless steel component normally works inside industrial machinery and equipment assemblies across automotive, appliance and industrial programmes.
A single design of this stainless steel component is often reused across a product family, so the finish is chosen to cover the harshest of them, without a second tooling round.
Customization and options
The options customers tune most
The options most often changed on this stainless steel component: material grade, coating, wall bands, flange form and end closure, and how the order is released – sample, pilot run or scheduled call-off.
The quotation for this stainless steel component is explicit about what the die already covers, so you can see which options are free and which need new tooling. Price breaks for the cup are shown against quantities on the quote.
Specifications
| Item | High-quality Custom Stainless Steel Deep Drawing Deep Drawing Aluminum |
|---|---|
| Brand | AUNOV |
| Designing | Send drawings, or send a sample to be measured – unusual walls, threads or tolerances are feasibility-checked first; changes are priced before they are made. |
| Tooling | Tooling is built and held under your part number, so tooling lead time stays under our control, and ownership is confirmed on the quotation. |
| Samples | Pre-production samples come with a full inspection report, so the approved first article becomes the gauge reference, and production starts only after your written sign-off. |
| Materials | Carbon steel, 304 / 316 stainless, aluminium and brass are all held in stock; mill certificates and heat numbers accompany the first article. |
| Surface finish | Plating, powder coating, anodising or polishing, per the print; the agreed finish travels with the part number. |
| Processing | Progressive drawing through several stages, annealed between draws, then trim and pierce; batch records are filed so a repeat order starts from approved data. |
| Equipment | 5-250 T mechanical presses, 250-500 T hydraulic presses and annealing furnaces in line, with CNC turning centres for secondary operations and CMM inspection. |
| Tolerance | +/-0.05 mm on flange and rim dimensions, wall controlled by the draw; capability is checked on the first article before the run continues. |
| Delivery terms | FOB Ningbo or Shanghai, T/T with deposit and L/C for larger runs; call-off schedules are supported. |
Packaging and delivery
This stainless steel component is packed to protect the finish: the coating decides whether parts are interleaved, bagged or tray-packed, in sealed cartons on export pallets, with documents issued to your instructions.