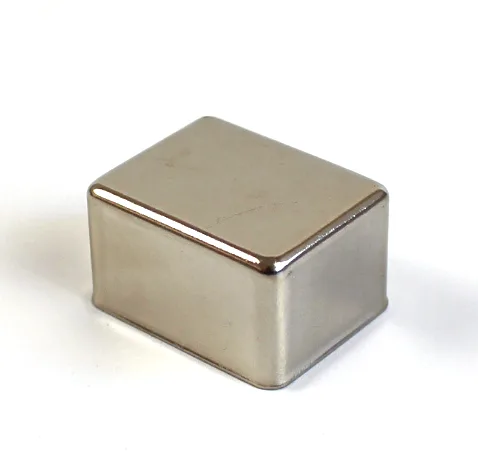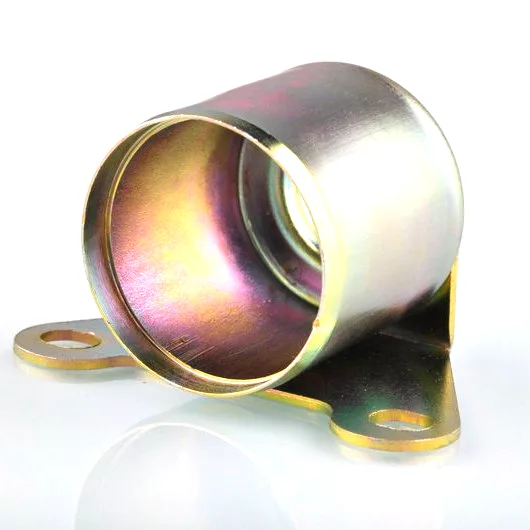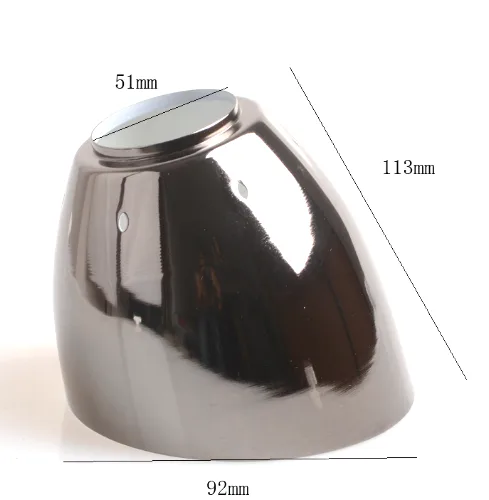
Aunov Tech manufactures the Deep Drawn Aluminum Time Capsule with Emery Finishing in aluminum on a single production floor. Once installed, the drawn housing provides a closed, seam-free body the customer builds into. Forming, machining and inspection share one floor, so the approved sample defines every later batch without re-quoting the job elsewhere.
Product overview
For this aluminium component, the drawing centres on, the formed envelope, flatness and hole location, each measured at first article and gauged on production batches.
Die building, pressing and machining for this aluminium component are all in house, so feasibility questions are answered on the shop floor, and the approved sample is kept as the master.
From coil to finished part
The process for this aluminium component runs in a fixed sequence: The shell starts as coil or blank and is drawn through single and progressive dies; threads are single-pointed or rolled and seats bored in one setup where possible.
The dome, emery finished manufacturing record is archived together with the drawing revision that produced it. Mill certificates are filed per heat, so dome, emery finished traceability survives a change of material batch.
Materials and finishing
Everything is drawn from a fixed stock list: carbon steel SPCC / DC01, 304 and 316 stainless, aluminium, brass and copper with this aluminium component costed in aluminium.
Finish selection follows the working environment: electrophoresis, powder coating, anodising and zinc / nickel plating. The agreed finish for this aluminium component travels with the part number on every reorder.
Repeat dome, emery finished orders are measured against the approved sample, so neither material nor finish drifts between lots. The approved dome, emery finished sample governs later runs, and any grade change is agreed in writing first.
Quality control
An ISO 9001 certified system governs production: incoming material is verified against mill certificates, the first article is CMM-measured against the print, and later batches follow the sampling plan agreed at approval. The dome, emery finished first article records cavity depth and seal face finish. Functional testing – torque, leak or pressure – can be written into the plan, and the batch file carries the results.
Applications
The aluminium component is fitted into industrial machinery and equipment assemblies in both OEM and aftermarket supply.
A single design of this aluminium component is often reused across a product family, so the finish is chosen to cover the harshest of them, and cost per piece stays at the volume tier.
Options and variations
The options customers tune most
Customer choices typically cover material (carbon steel, stainless, aluminum, brass), surface treatment, draw depths, flange and thread features, vent holes, sealed exits and finishes matched to the environment, and order shape – prototype lots first, scheduled volumes after approval.
Tooling impact is stated line by line for each change: free variations stay free, and anything needing a die or fixture is priced separately.
Specifications
| Item | Deep Drawn Aluminum Time Capsule with Emery Finishing |
|---|---|
| Brand | AUNOV |
| Designing | Your drawing sets the part – a manufacturability review comes back with the quotation; the same drawing is used for every repeat order. |
| Tooling | Progressive and drawing dies are designed and built in house, so tooling lead time stays under our control, and the charge is refundable against agreed volumes. |
| Samples | Prototype and pre-production samples are provided against the drawing, so the approved first article becomes the gauge reference, and the signed sample is kept for future reorders. |
| Materials | Carbon steel, 304 / 316 stainless, aluminium and brass are all held in stock; special grades are sourced to the drawing when volumes justify. |
| Surface finish | Natural, plated or coated – the print decides, and the agreed finish is logged; finish thickness and adhesion checked on the first article. |
| Processing | Coil blanking and progressive drawing, coining on the final station where the print calls for it; every stage is logged against your part number. |
| Equipment | Mechanical presses from 5 to 250 T and hydraulic presses 250-500 T, with in-line annealing furnaces, with CNC turning centres for secondary operations and CMM inspection. |
| Tolerance | +/-0.03 mm on turned secondary features, +/-0.1 mm on as-drawn walls; critical dimensions carry CMM data with the shipment. |
| Delivery terms | FOB Ningbo or Shanghai, T/T or L/C, with D/P accepted on repeat business; price breaks tie to annual volume. |
Packaging and delivery
Packaging protects the finished surfaces of this aluminium component: the coating decides whether parts are interleaved, bagged or tray-packed, in sealed cartons on export pallets, documented and marked to your instruction.