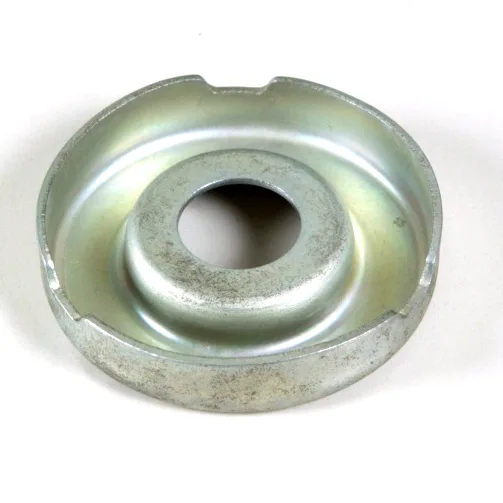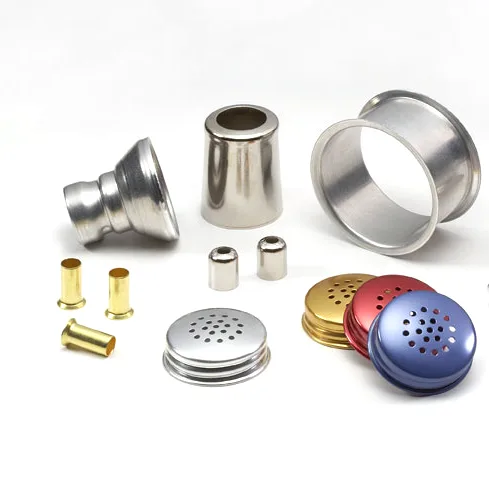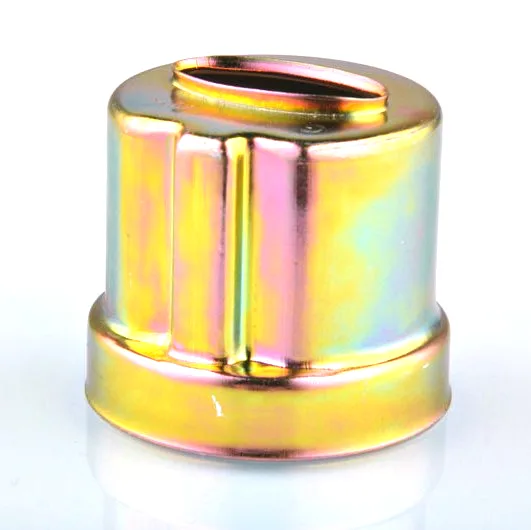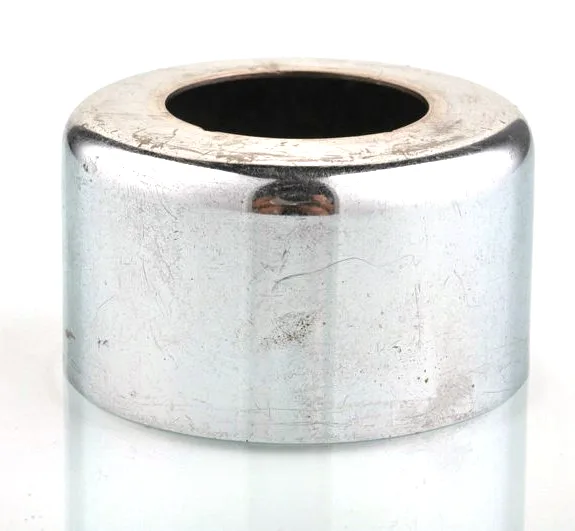
Aunov Tech supplies the Deep Drawn Aluminum Pressure Vessel as a aluminum component manufactured entirely in house. On the product, the deep drawn part replaces a machined-from-solid body with a lighter, faster drawn shell. Forming and machining share equipment, staff and batch records, which keeps tolerances consistent from sample to volume on one production route.
Product overview
What defines this aluminium component is, material grade, wall uniformity and thread position, each measured at first article and gauged on production batches.
Forming, machining and finishing for this aluminium component happen on one site, so a change of wall or hole does not restart the programme, and the approved sample is kept as the master.
How the part is produced
This is how the aluminium component is built: Coil is blanked and drawn through progressive and single-stage dies; after drawing, critical faces are machined and the part is degreased and gauged.
Each nickel-plated pressure vessel shipment is verified against the master sample before it leaves the shop. Deviations on the nickel-plated pressure vessel are reported before shipment rather than found on your assembly line.
Materials and surface finish
Materials kept on the floor cover cold-rolled steel (SPCC / DC01), 304 / 316 stainless, aluminium, brass, copper and bronze and the grade agreed for this aluminium component is aluminium.
The finish is chosen for the duty it will see: zinc and nickel plating, chrome, anodising, powder coating and passivation. The choice is recorded on the drawing for this aluminium component, so the decision never has to be made twice.
Route cards follow each nickel-plated pressure vessel batch through the shop, so the next run starts from the data that already worked. Deviations on the nickel-plated pressure vessel are reported before shipment rather than found on your assembly line.
Quality control
The plant is ISO 9001 certified: certificates verify each incoming batch of material, first-article geometry is confirmed on the CMM, and later batches follow the sampling plan agreed at approval. CMM first-article measurement of the nickel-plated pressure vessel covers diameters and gauges thread class. Functional testing – torque, leak or pressure – can be written into the plan, and the inspection report ships with each batch.
Applications
This aluminium component is used in industrial machinery and equipment assemblies for OEM and Tier-1 customers.
This aluminium component is supplied to several positions in the same machine, so the finish is chosen to cover the harshest of them, and the die does not have to change.
Customization and options
Frequently varied options
What customers usually vary on this aluminium component: coating, wall bands, flange profiles, threads and the degree of closure on the ends, with orders run as prototypes, pilot lots or scheduled call-offs.
Tooled and untooled options for this aluminium component are listed separately, so you are not charged twice for a feature the die already makes. For the nickel-plated pressure vessel, tooling terms live in the quote – nothing is left implied.
Specifications
| Item | Deep Drawn Aluminum Pressure Vessel |
|---|---|
| Brand | AUNOV |
| Designing | Quotation follows the print, not a catalogue – a manufacturability review comes back with the quotation; the approved drawing is kept as the controlled master. |
| Tooling | Progressive and drawing dies are designed and built in house, so die cost stays transparent, and the die remains dedicated to your part. |
| Samples | Sample parts are measured and reported before submission, so the part is proven before it is made in volume, and the signed sample is kept for future reorders. |
| Materials | Materials held include carbon steel, 304 / 316 stainless, aluminium and brass; special grades are sourced to the drawing when volumes justify. |
| Surface finish | Zinc, nickel or chrome plating, anodising, passivation or e-coat; the agreed finish travels with the part number. |
| Processing | Multi-stage deep drawing with interstage annealing, trimmed and pierced in following dies; every stage is logged against your part number. |
| Equipment | Press shop running 5-250 T mechanical and 250-500 T hydraulic presses, annealing ovens on site, with CNC turning centres for secondary operations and CMM inspection. |
| Tolerance | +/-0.05 mm to +/-0.1 mm across the part, wall thickness held to print; critical dimensions carry CMM data with the shipment. |
| Delivery terms | FOB, CIF or DDP per Incoterms 2020, T/T with deposit and L/C for larger runs; price breaks tie to annual volume. |
Packaging and delivery
Packing for this aluminium component is chosen around the coating: the coating decides whether parts are interleaved, bagged or tray-packed, in sealed cartons on export pallets; shipping documents and carton marks follow your instructions.